
Product example
Power Tool Gear Components
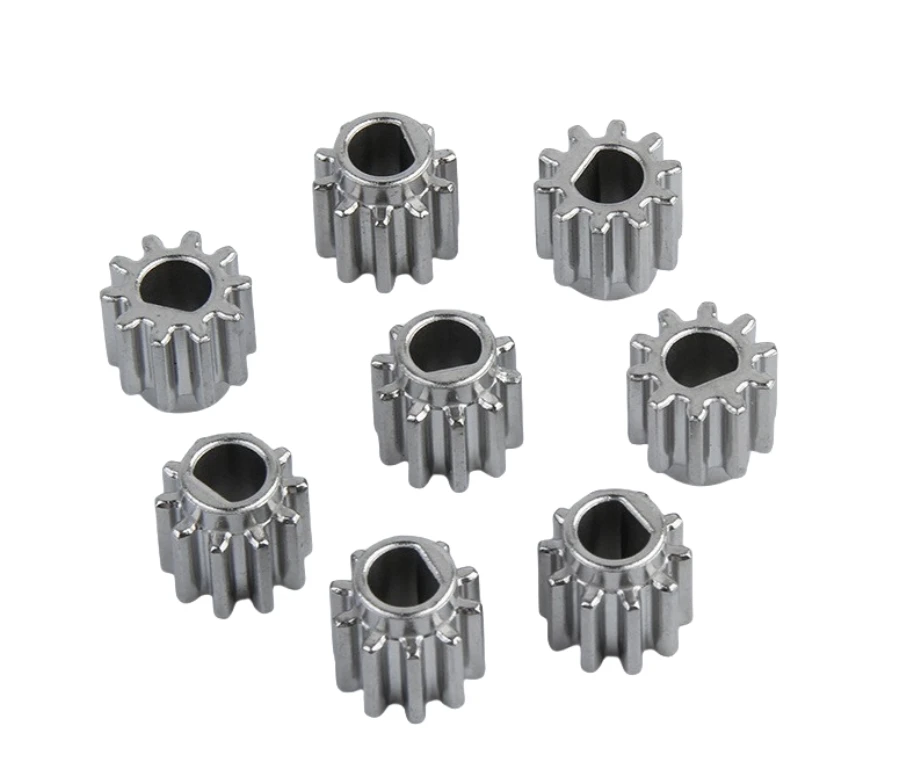
Small gear forms with different bore and hub details. Review their mating gear, load and installation requirements.
Power tool and industrial hardware components are the working parts inside tools and equipment — tool gears, pneumatic fork and clevis parts, guide and connecting components, connection bodies and wear hardware. SINTS produces these by powder metallurgy (PM), metal injection molding (MIM) or machining, with the route following the working duty and the surface that wears.
Small gear forms with different bore and hub details. Review their mating gear, load and installation requirements.
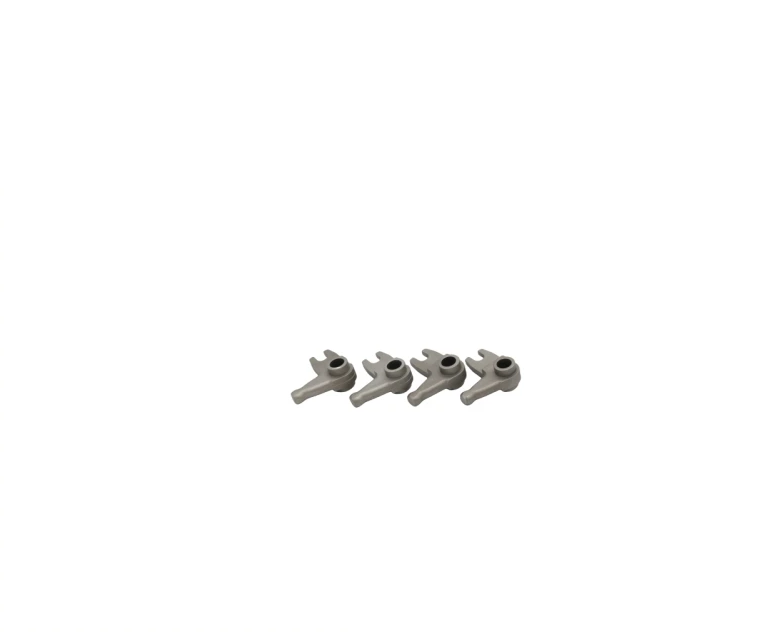
Forked mechanism parts with holes and contact features. Define pin fit, travel and load direction.
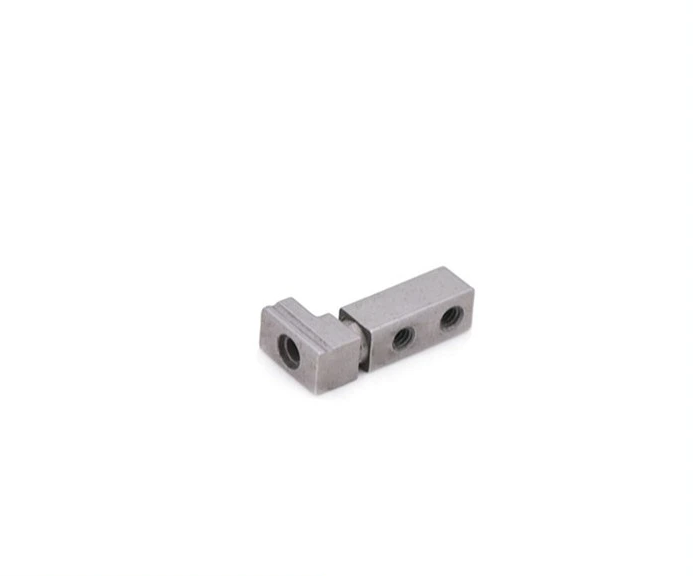
A stepped guide-related part with multiple openings. Clarify the locating, guiding and connecting surfaces.
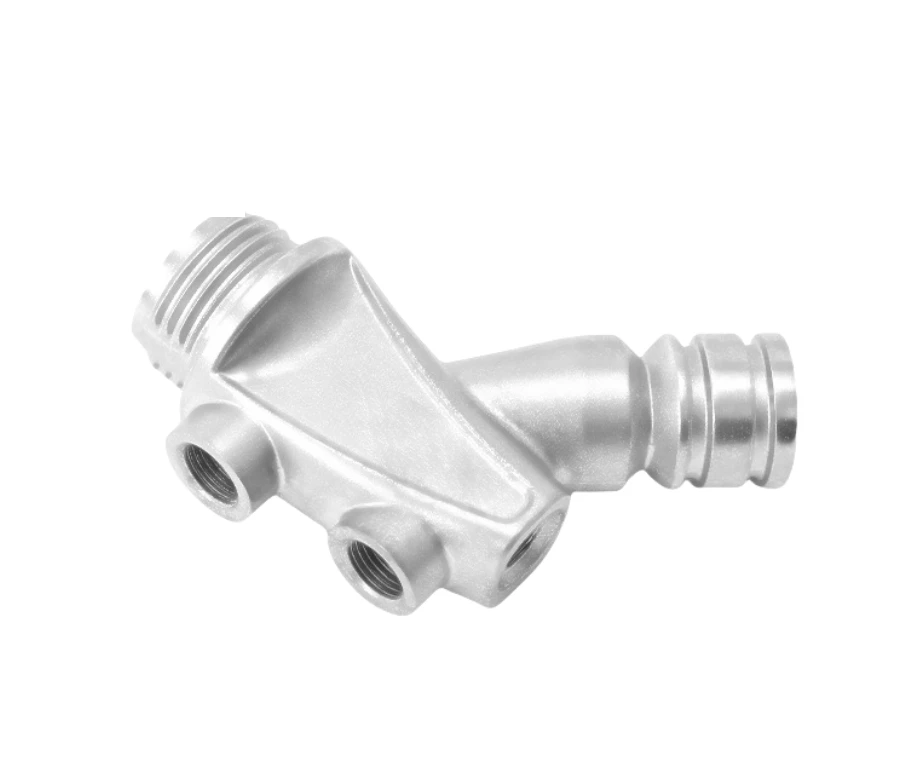
A body with intersecting connection features. Review openings, wall transitions and assembly datums on the part drawing.
Examples from the SINTS product catalog, shown for component identification. These are custom parts, not stock specifications. Dimensions, material, supply scope and acceptance requirements are confirmed from your project drawing.
Explore each component in detail, including its interfaces, manufacturing review and drawing requirements.
The fork examples show a compact component that transfers or guides motion. Supply the mating pin, load direction and movement range so the hole fit, fork ends and contact surfaces can be assessed as one assembly. Critical interfaces may need finishing after forming.
The gear examples illustrate a range of hub and bore shapes. For a new project, distinguish steady rotation from reversing or impact duty, and include the mating gear and installation datums. Material and final condition are confirmed against the agreed operating and inspection requirements.
The part drawing and its assembly determine the manufacturing route and the inspection plan.
Load direction, torque, impact, reversing and expected operating cycles.
Pin and shaft fits, travel, stops and contact geometry.
Material, heat treatment, wear surfaces and corrosion requirements.
Dimensional, assembly and agreed functional tests with mating parts.
Three reference tables for power tool and industrial hardware parts: the grades used for loaded and wearing components, where the forming routes stop, and what the route from drawing to first article looks like.
| Grade | Condition | Yield / UTS (MPa) | Elong. | Hardness | Density (g/cm³) | Why it is used here |
|---|---|---|---|---|---|---|
| 4605 (Fe-2Ni) | Sintered | 500 / 700 | 11% | 70–100 HRB | 7.50 | The default for loaded tool structure parts. More as-sintered strength than 4600 without adding a hardening step. |
| 4605 (Fe-2Ni) | Heat treated | 1425 / 1610 | 3% | 45–50 HRC | 7.50 | Impact and wear parts that must survive abuse: the highest strength available in this alloy set, with elongation down to 3%. |
| 4600 (Fe-8Ni) | Sintered | 265 / 410 | 25% | 70–90 HRB | 7.60 | Brackets, covers, guards and other structural parts where cost matters more than strength. |
| 4140 (42CrMo4) | Heat treated | 1400 / 1405 | 5% | 40–45 HRC | 7.50 | High-load shafts, spindles and connecting parts. Takes through-hardening without the distortion of a case route. |
| 440C | Sintered | 1550 / 1750 | 1% | 58–62 HRC | 7.50 | Blades, cutting edges and abrasion surfaces. The 1% elongation is the price of 58–62 HRC and it has to be acceptable. |
| 17-4PH | Sintered → aged | 720 / 900 → 1070 / 1160 | 11% → 7% | 20–25 → 35–45 HRC | 7.50 | Outdoor and garden tools, and any part that needs strength plus weather resistance. |
Values are reference ranges from the SINTS material summary measured on test pieces. Impact toughness is not in that table, and it is the property that decides most power tool failures — so a part that takes shock loading is reviewed on density and heat treatment, not on tensile strength alone.
| Requirement | Powder compaction | MIM | What it means here |
|---|---|---|---|
| Density and impact toughness | Density follows compacting pressure and mass distribution | Same, with more freedom in geometry | A part at 6.8 g/cm³ and one at 7.4 g/cm³ can show the same tensile value and fail differently under shock |
| Wall section in housings and covers | Set by fill, ejection and green strength; reviewed per part | 1–3 mm works comfortably; below about 0.5 mm cavity fill is at risk | Thin cosmetic housings usually point to MIM; thick loaded structure points to compaction |
| General dimension, as sintered | Roughly ±0.3–0.5% of the dimension | Roughly ±0.3–0.5% of the dimension | Bearing seats and gear-shaft fits are sized or reamed rather than pressed to final |
| Hardened features | Sinter-hardening in the furnace, or quench and temper after | Same, plus the option to mould a hardened insert seat | Distortion after hardening has to be planned into the stock allowance, not corrected afterwards |
| Economic volume | Tooling-led; reviewed against annual demand | Tooling-led; reviewed against annual demand | As a rule of thumb, a tool amortised over fewer than a few thousand pieces a year rarely beats machining |
Percentage tolerances follow the published MIM tolerance note and are planning arithmetic, not a capability claim. Note that tolerance is the last question on a power tool part — density, hardening and edge condition decide whether it survives the first drop test.
| Stage | Typical lead time | What you receive | What we need from you |
|---|---|---|---|
| Drawing review and DFM feedback | Issued with the quotation | Feature-by-feature route proposal, tolerance and finishing notes, and the open points that must be answered before tooling | 2D drawing with tolerances and datums, STEP model, target annual volume, material or the performance requirement |
| Tooling | 25–30 days as quoted on recent programs | Mould or die built and released to trial condition | Approval of the DFM report and confirmation of the alloy |
| T0 samples | 7–10 days after tooling release as quoted on recent programs | Parts plus a dimensional report against the drawing | Agreed inspection plan and datum scheme |
| Sizing, finishing and heat treatment | Runs inside or immediately after the sample stage | Sized and finished parts, hardness and density results where specified | Which features must be held after sintering, and which may be finished |
| First-article report | With the first approved samples | Dimensions, material, hardness and density measured in-house rather than subcontracted | Drawing with the critical characteristics marked |
| Production release | After sample approval | Serial production to the agreed inspection plan | Confirmed annual volume, MOQ and packaging |
Tooling and sample durations above are the lead times quoted on recent programs of comparable size, not a standard promise; the schedule for a specific part is confirmed with its quotation. Every result in the first-article report is measured on the instruments listed on the capabilities page.
Power tool and industrial hardware components are the working parts inside tools and equipment. These answers cover duty-based process selection, moving interfaces and sample qualification.
Repeat-volume gears and structural motion parts are the strongest candidates — spur and helical tool gears, drive and reduction parts, guide and connecting components, and bracket or body parts that carry a defined load. The decision then depends on duty, tooth loading, required density and whether a secondary machining operation is needed on a functional feature.
It changes which property matters. A continuously running drive is dimensioned for fatigue and wear, an intermittent high-load tool is dimensioned for peak stress and impact, and a tool that reverses or jams repeatedly accumulates damage that a steady-duty analysis would miss. Stating the duty cycle, peak load and any stall condition makes the material and treatment recommendation answer a real failure mode.
The pin and the moving interface. A fork or clevis transfers load through a pin or pivot, so the bore diameter and tolerance, the bearing surface, the alignment of the two arms and the hardness at the contact point determine whether the joint stays tight and whether the bore wears or elongates. Those are functional requirements rather than general dimensions.
A tool gear should be specified against the torque it actually transmits and the shock it sees, not against a nominal rating. Gear ratio, tooth form, density, hardness and backlash all follow from that, and where a gear is also a wear surface or a locating feature those functions need to be stated separately so they are addressed rather than assumed.
Sample approval compares the produced part against the agreed drawing and requirements using the intended assembly where relevant — fits, movement, surface condition and any agreed functional check. The acceptance criteria should be agreed before samples are made, so that the result of the check is a decision rather than a debate, and any first-article documentation is defined in the same step.
Include mating parts, operating load and motion, critical fits, final material condition and annual volume.
These are review inputs, not fixed catalog specifications. Supply the drawing revision and identify any requirements still to be confirmed.
Define gear geometry, mating interfaces, duty and final condition before comparing a drawing-based quotation.
Read the guide →Process SelectionCompare MIM and CNC using the same geometry, critical dimensions, material condition, volume and approval requirements.
Read the guide →