
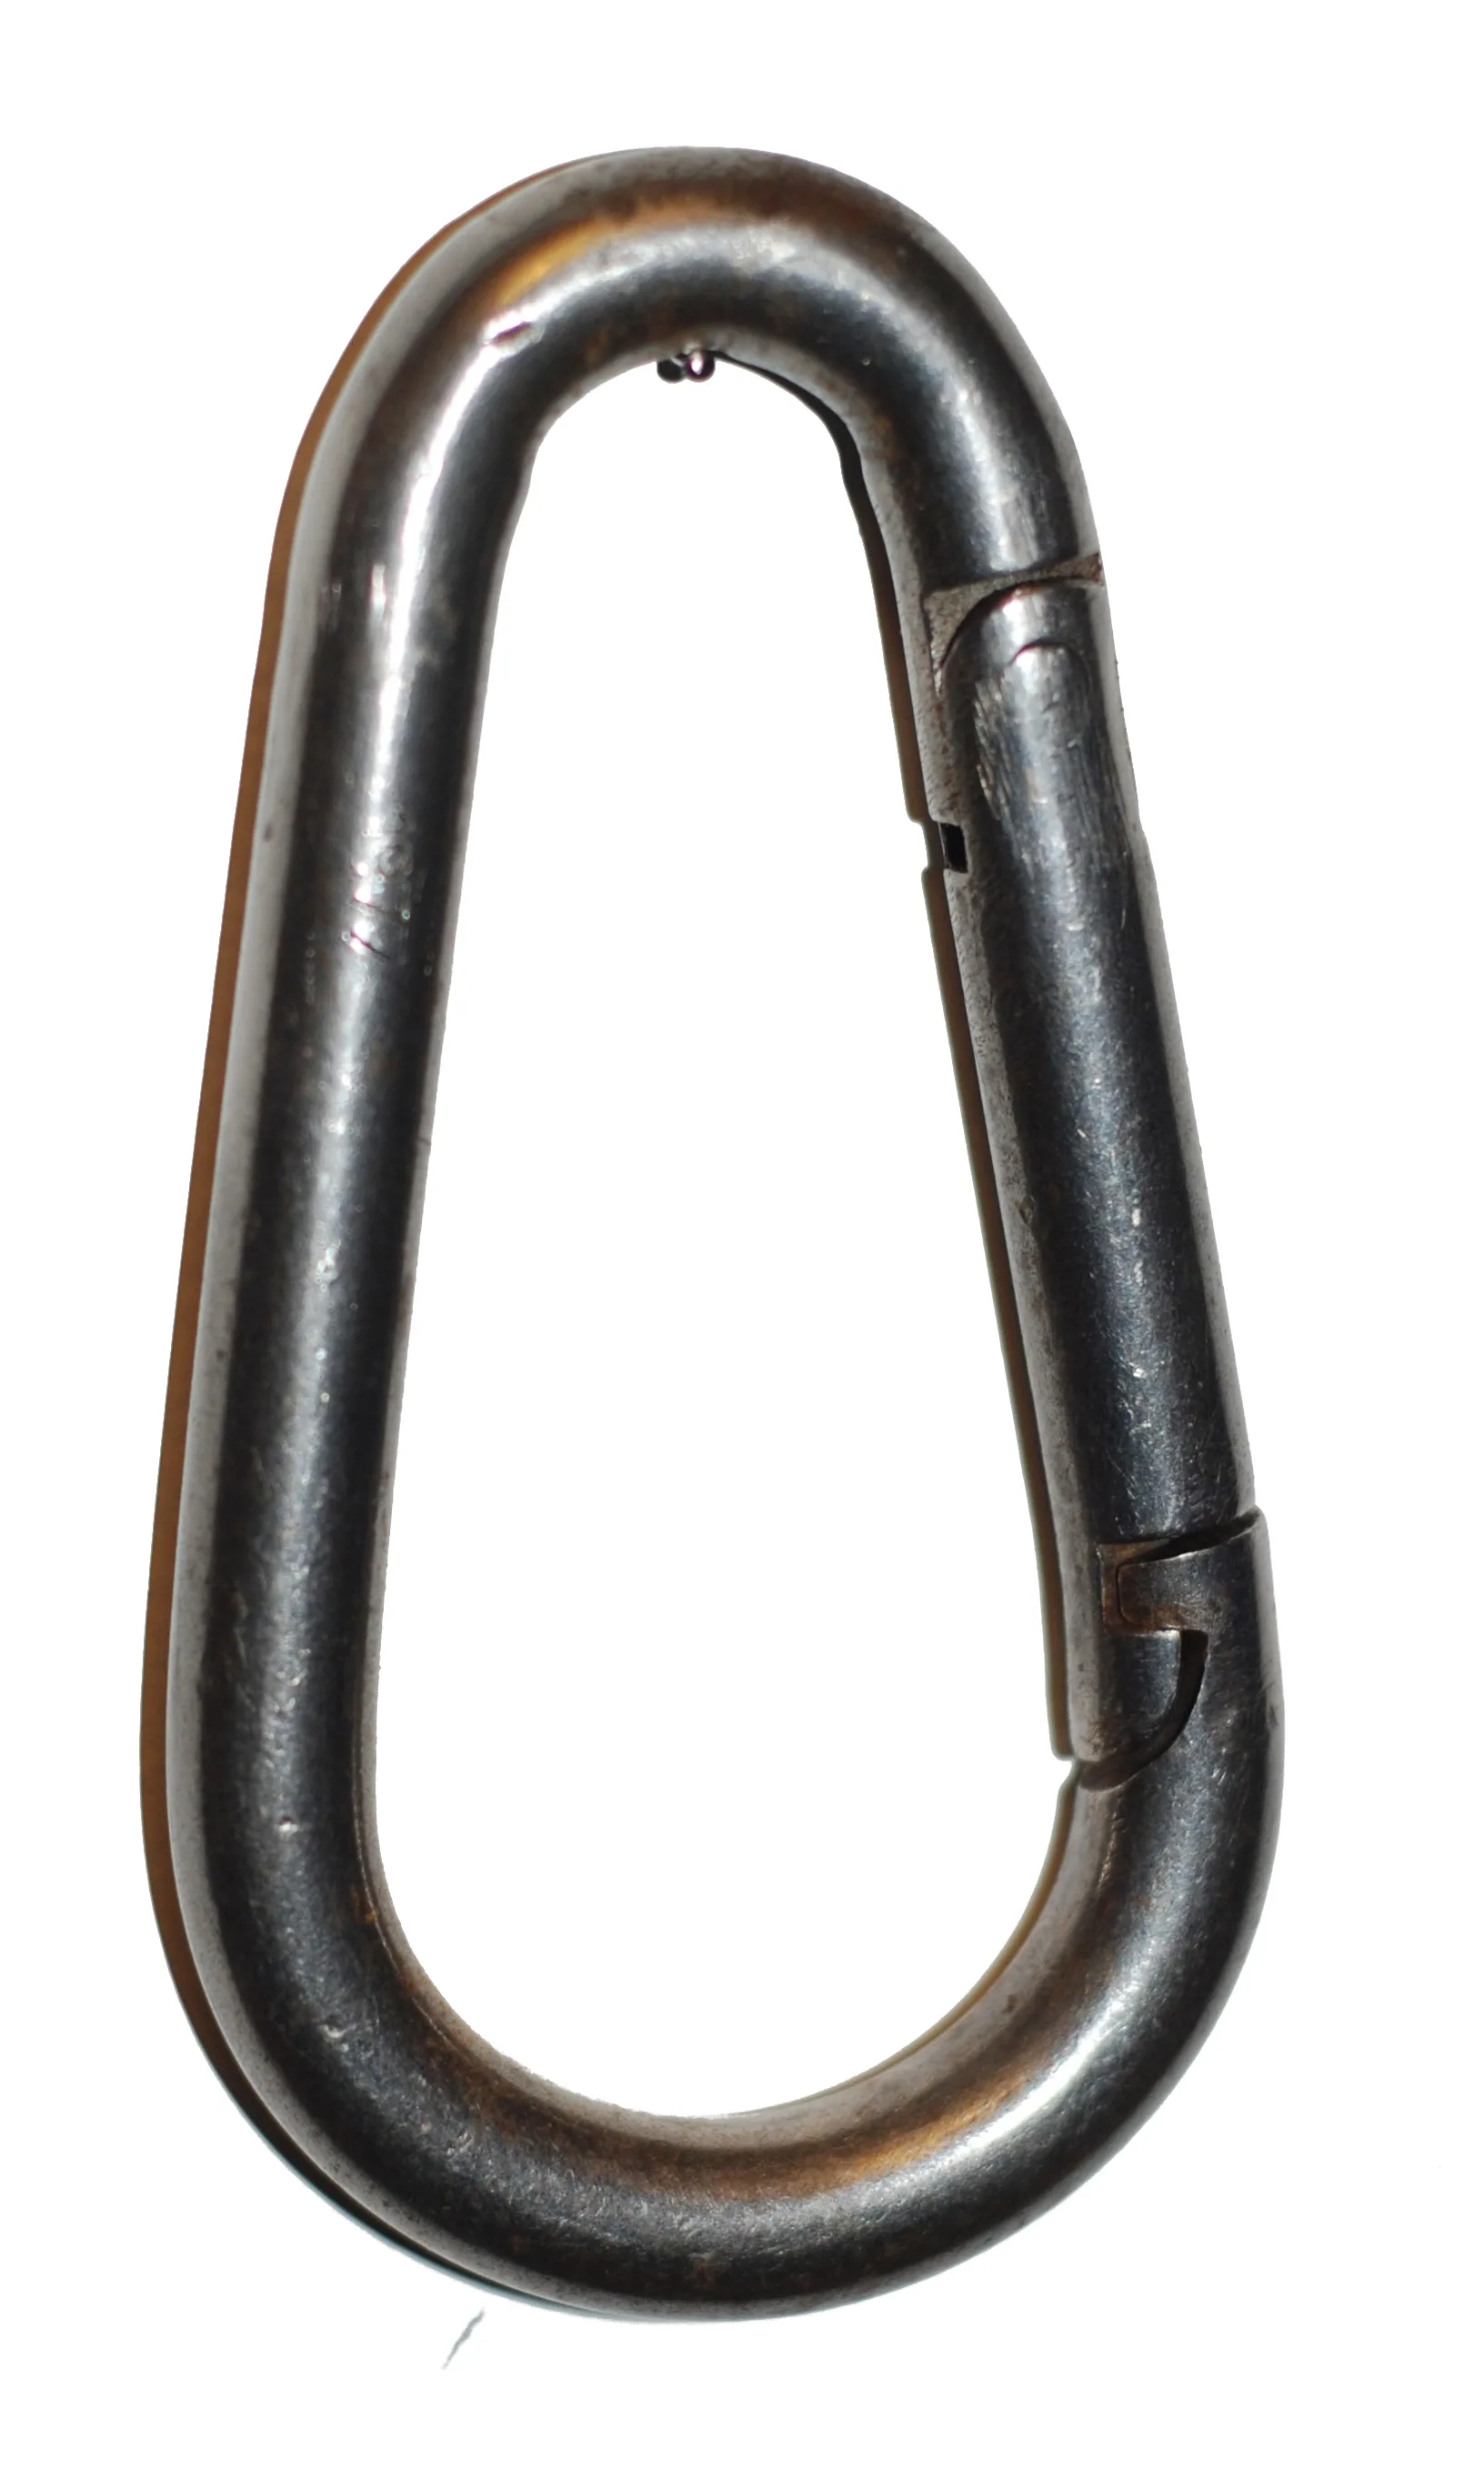
What a climbing connector requires across its load path
This is a component manufacturing discussion, not a rated or certified finished safety product.
Connector assembly, gate engagement and load-direction interfaces
Provide the complete connector assembly, gate engagement and intended load directions.
Identify all interfaces whose wear or movement could affect closure or retention.
Why must component manufacturing and equipment qualification be separated?
Manufacturing inspection can confirm a part against an agreed drawing and material specification.
Qualification addresses the complete product, its intended use and required test program.
Maintaining that boundary prevents a component photograph or dimensional report from being mistaken for equipment approval.
Reviewing routes against the required design and verification
Review forging, machining, forming and other suitable routes against the required design and verification.
Do not choose MIM or PM solely because the component is metal and small.
Compare manufacturing capabilities →Connector material, wear treatment and operating-environment requirements
Define material and final treatment against load direction, wear and the operating environment.
Mark surfaces whose fit or contact changes after finishing.
Rated loads, pressure limits and operating life require their own agreed design and acceptance requirements.
Review material-selection information →Where the manufacturing chain stops and qualification begins
This page has a boundary the other pages in the group do not. A component can be made to a drawing and still not be a rated product, and on load-bearing equipment that distinction is not a formality — it is the whole point.
| Link in the assembly chain | What it adds to the stack | Where to take it out of the chain |
|---|---|---|
| Intended load path | Every link in a load path carries the full load, so the chain does not average. The weakest link decides, and it is usually the one whose orientation was assumed rather than stated. | State the load direction and the loaded members on the drawing. Without that, the part is designed against an assumed path and nobody can tell whether the assumption held. |
| Gate engagement | The gate is a moving link that also carries load. Its engagement geometry and its spring behaviour are two different requirements on one feature. | Separate the structural requirement from the operating requirement. They are verified by different tests and they fail in different ways. |
| Component boundary | A connector is a set of parts. Chains drawn across an assembly are not closed by any one component drawing, and treating them as if they were is where responsibility gets lost. | Define the supplied component explicitly and list what is outside it. The boundary should appear on the drawing, not only in correspondence. |
| Material and wear treatment | Material choice and surface treatment move the same properties. Specifying one without the other leaves the durability of the loaded faces undefined. | State both against the loaded faces rather than against the part as a whole. A blanket treatment note can miss exactly the surface that wears. |
| Verification responsibility | Component manufacture and equipment qualification are separate chains with separate evidence. Nothing in a component inspection report can substitute for the second. | Agree in writing which party holds which evidence. On this class of part that agreement belongs before the order, not after the first batch. |
The assembly designer sets the tolerance allocation. Mark the controlling dimensions on the component drawing.
The honest position for this group is narrow and worth stating plainly: we can manufacture a component to a drawing and hold its dimensions, and that is not the same as certifying a rated product. Anyone who blurs the two on load-bearing equipment is not helping the buyer.
What a component inspection report does and does not cover →
Material records, dimensional checks and qualification requirements
Specify material records, dimensional checks and the customer's required qualification program.
A photograph cannot establish a working load or equipment certification.
Quality documentation →What to include in your enquiry
- Drawing and mating dimensions.Provide the complete connector assembly, gate engagement and intended load directions. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Specify material records, dimensional checks and the customer's required qualification program. Specify the mating part or inspection fixture.
Common questions
Does this page specify a safe working load?
No. Load limits and qualification belong to the complete approved design and its test program; none is assigned to this reference.
Why must component manufacturing and equipment qualification be separated?
Manufacturing inspection can confirm a part against an agreed drawing and material specification. Qualification addresses the complete product, its intended use and required test program. Maintaining that boundary prevents a component photograph or dimensional report from being mistaken for equipment approval.
How should the part be checked in the tool or mechanism?
Specify material records, dimensional checks and the customer's required qualification program. A photograph cannot establish a working load or equipment certification.