
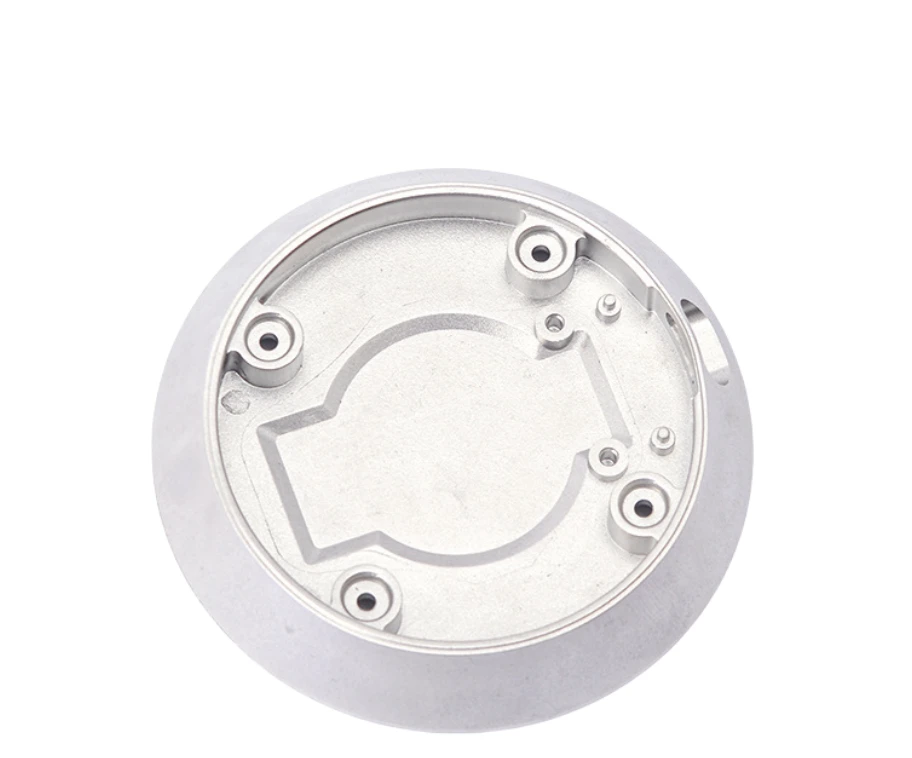
What power tool covers position and protect internally
The circular reference has attachment features and an internal locating profile.
Mating housing, internal clearance and fastening-pattern interfaces
Specify the mating housing, internal clearance and fastening pattern.
Distinguish a locating recess from a nonfunctional relief or cosmetic contour.
Why define the internal envelope of a tool cover?
The exterior and fastening pattern do not fully describe clearance to the enclosed mechanism.
An internal envelope connects the cover to its neighboring parts.
Including it allows assembly and interference checks to address more than the visible profile.
Forming versus machining for cover and mounting bodies
Compare forming and machining for the body and mounting features.
The final mounting plane and locating interfaces may need dedicated finishing.
Compare manufacturing capabilities →Cover component material, wear treatment and environment requirements
Define material and final treatment against load direction, wear and the operating environment.
Mark surfaces whose fit or contact changes after finishing.
Rated loads, pressure limits and operating life require their own agreed design and acceptance requirements.
Review material-selection information →Seating, fastener alignment and internal-clearance checks
Check seating, fastener alignment, internal clearance and the specified exterior finish.
Agree any operating or environmental requirements for the actual tool.
Quality documentation →Where cost sits on a tool cover
A cover is a shape with a large surface and little structure. That makes it a part where a competing process is often cheaper, and where the honest answer to a cost question starts with which process the geometry actually suits.
| Cost element | Why a small order costs more per piece | Why a large order stops getting cheaper |
|---|---|---|
| The forming tool | A round cover with an internal locating profile needs a tool with a clean draw and a controlled rim. Tool cost is moderate, and it is one-off. | Tooling is recovered early. The recurring cost is rim wear, which shows as a change in seating before any dimension fails. |
| Process choice for a large thin shell | A pressed or deep-drawn shell can undercut a formed one at almost any volume when the wall is uniform and the features are shallow. Forming wins where there are thick bosses or undercuts. | The process is chosen once. If stamping or drawing is viable, volume improves that route faster than it improves forming, so the gap widens rather than closes. |
| Coating by surface area | A cover has a large area relative to its mass. Coating and its preparation are priced on area, and this is often the largest line on the part. | Area does not shrink with volume. This line is close to flat per part no matter how many are ordered. |
| Seating and clearance checks | A cover is judged on how it sits on its housing. That is an assembly check, and it needs a fixture that represents the housing. | The fixture is one-off. The check itself is quick once it exists, so repeat orders are cheaper for this reason rather than any other. |
| Internal clearance verification | Clearance to the enclosed mechanism is not visible from outside and needs a section, a scan or a gauge. | Non-destructive methods are faster than sectioning but still per part or per lot. Sampling can be agreed; the measurement cannot be skipped. |
For a price comparison, use the same material, finish, order quantity and inspection requirements.
When a cover enquiry arrives, the first useful question is whether the wall is uniform. If it is, a stamping house will usually beat a forming route and the right answer is to say so early. Forming earns its place where the part has thick bosses, undercuts or a locating profile that a pressed shell cannot hold.
What to include in your enquiry
- Drawing and mating dimensions.Specify the mating housing, internal clearance and fastening pattern. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Check seating, fastener alignment, internal clearance and the specified exterior finish. Specify the mating part or inspection fixture.
Common questions
Can a cover be approved without the mating housing?
Initial dimensions can be reviewed, but fit and interference checks need the housing and enclosed component envelope.
Why define the internal envelope of a tool cover?
The exterior and fastening pattern do not fully describe clearance to the enclosed mechanism. An internal envelope connects the cover to its neighboring parts. Including it allows assembly and interference checks to address more than the visible profile.
How should the part be checked in the tool or mechanism?
Check seating, fastener alignment, internal clearance and the specified exterior finish. Agree any operating or environmental requirements for the actual tool.