Product example
Spur Gears and Compound Gear Parts
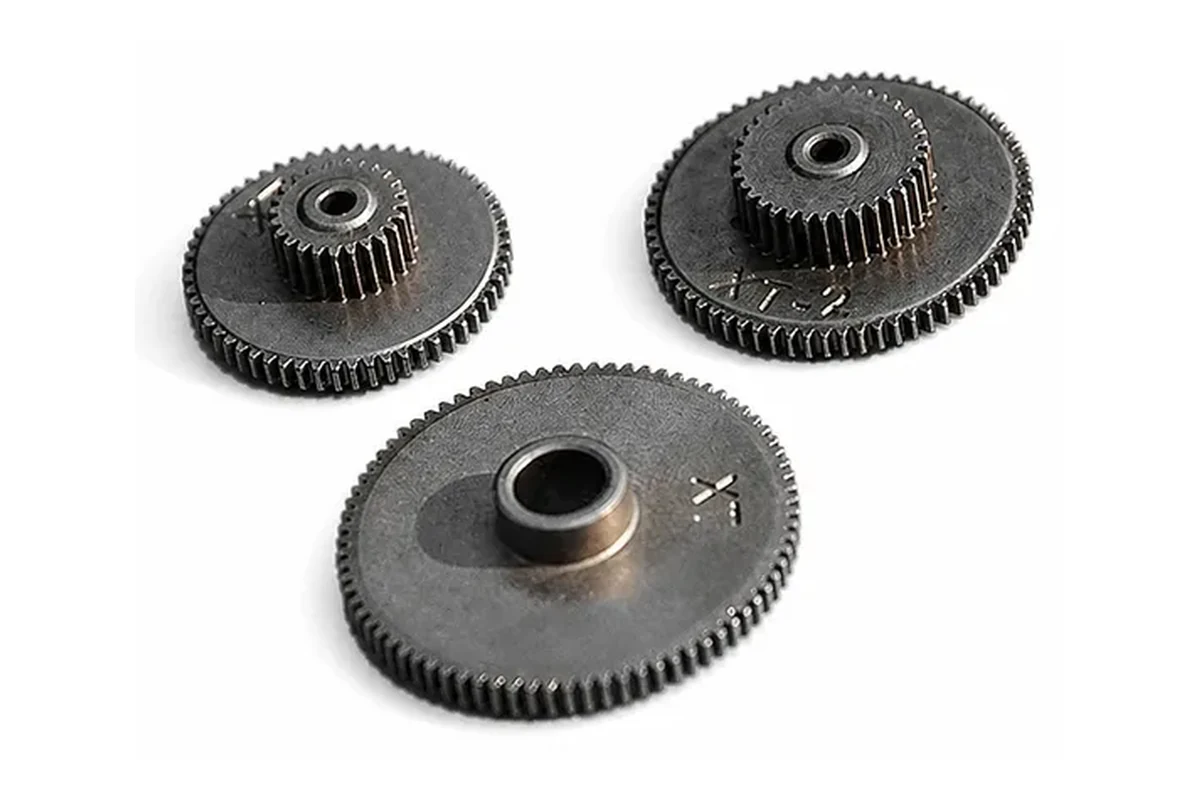
Compound and hubbed gear examples. Tooth geometry and the mounting bore must be defined against consistent datums.
Gears and transmission components are the parts that transfer rotation and torque in a mechanism — spur, helical and bevel gears, compound gears, bushings and the mating supports around them. Powder metallurgy (PM) is usually the first route evaluated for these parts because it forms the tooth profile in one operation; metal injection molding (MIM) becomes relevant when the gear carries integrated geometry beyond the teeth.
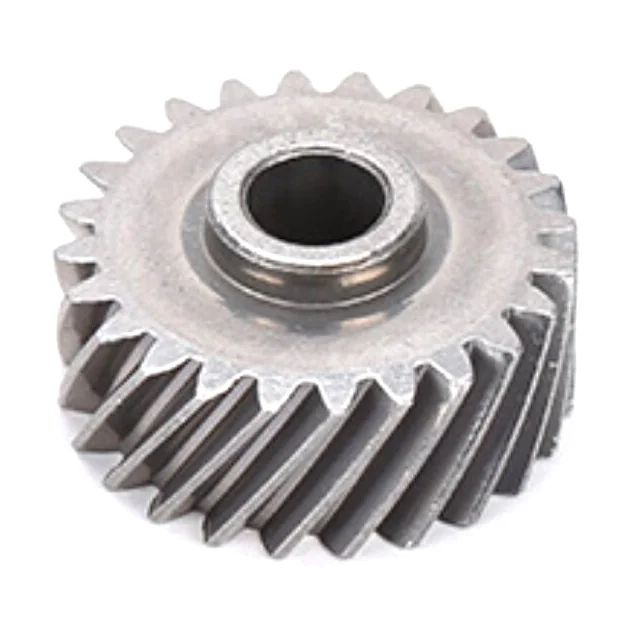
Compound and hubbed gear examples. Tooth geometry and the mounting bore must be defined against consistent datums.
An angled-tooth gear reference. Specify helix angle, hand, mating gear and parameter convention in the drawing.
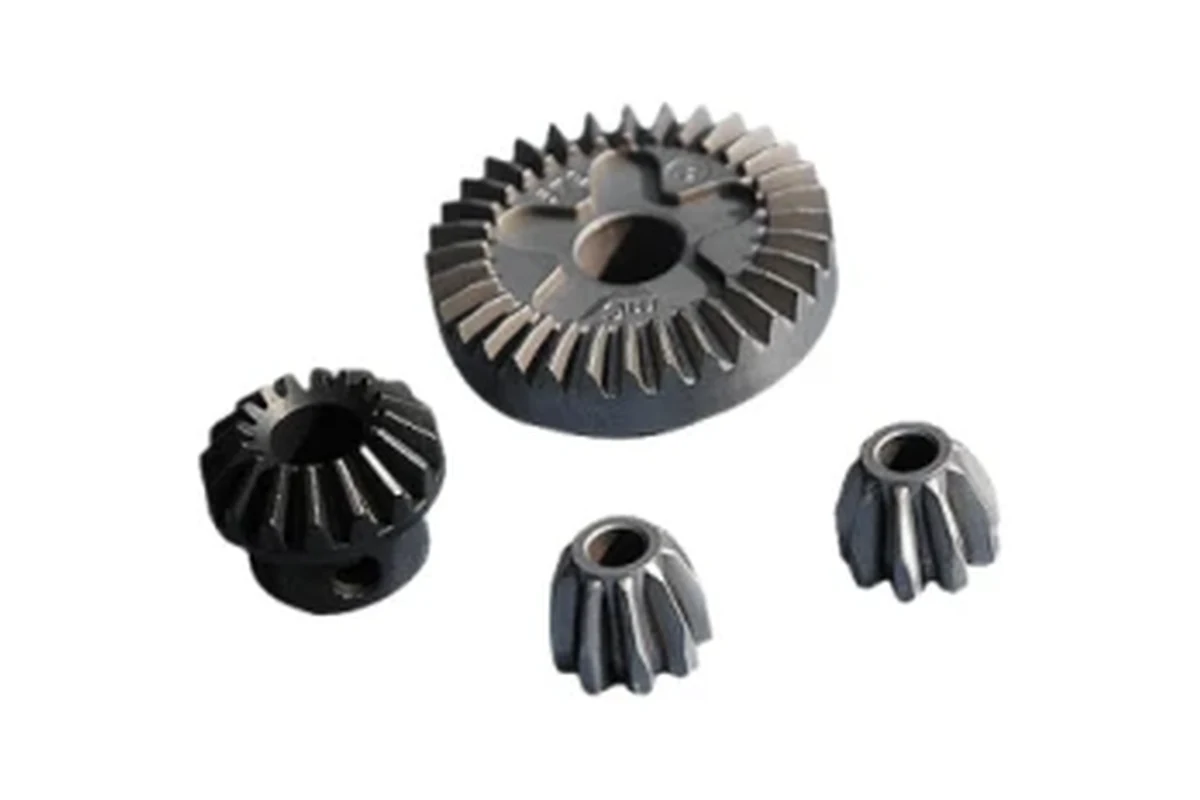
Angled-axis gear references. Review the mating pair, shaft angle and mounting position together.
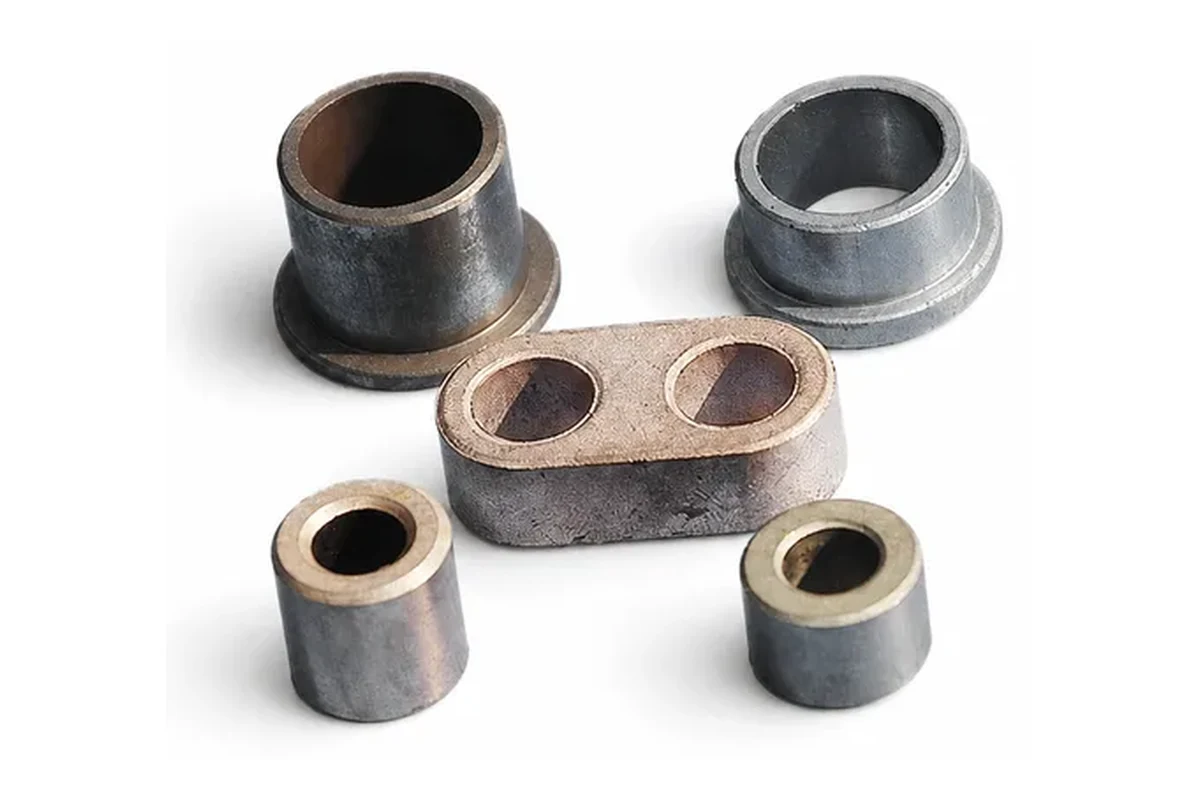
Plain and flanged bushing forms for supporting, locating or guiding a shaft. Fits and lubrication depend on the actual assembly.
Examples from the SINTS product catalog, shown for component identification. These are custom parts, not stock specifications. Dimensions, material, supply scope and acceptance requirements are confirmed from your project drawing.
Tooth count, module or pitch, pressure angle, face width and helix data.
Torque, speed, shock, lubrication and target life or acceptance test.
Bore fits, face datums, runout and the mating gear or shaft.
Material condition, sample quantity, annual demand and inspection scope.
Explore each component in detail, including its interfaces, manufacturing review and drawing requirements.
The examples include different tooth forms and integrated hubs. Tooth data alone is not enough to define a repeatable assembly: include bore fit, face datums, the mating gear and working load. The detailed guides below explain the information needed for each gear form.
The bushing examples show several external profiles. Define whether the part guides, locates or supports motion, then provide the mating shaft and housing. Lubrication and material condition should be specified for the duty rather than assumed from the photograph.
A gear drawing defines one member. The mesh is defined by numbers shared between two members, and every tooth form on this page changes what those numbers do and what the housing has to control as a result. This is the geometry layer, before any tolerance question comes up.
For an unshifted straight-tooth pair the centre distance follows from the module and the two tooth counts: a = m × (z1 + z2) / 2. The pressure angle does not appear in that expression, but it does set the shape of the flank and the separating force that lands on the bearings.
A helix angle changes the arithmetic. The normal module is what the cutter is made to; the transverse module is what the centre distance follows. So the same normal module and the same tooth counts put a helical pair further apart than the straight equivalent: a = mn × (z1 + z2) / (2 cos β). That is one of the reasons a helical pair cannot simply be dropped into a housing designed around the straight version.
Bevels have no centre distance at all, because the axes meet. The pair is positioned by the shaft angle and by the mounting distance measured from the cone apex to the locating face. Where a spur pair is controlled by the distance between two parallel bores, a bevel pair is controlled by where each member sits along its own axis.
| Tooth form | What defines the mesh on paper | What the housing has to control |
|---|---|---|
| Spur / straight | Module, both tooth counts and the pressure angle. For an unshifted pair the centre distance follows from the module and the sum of the teeth. | The distance between two parallel bores, and their parallelism. The mesh itself needs no axial location. |
| Helical | The same three, plus the helix angle and the hand. The normal module is the tooling number; the transverse module is the one the centre distance follows. | Bore spacing, parallelism and axial restraint, because the helix turns torque into a thrust that has to land somewhere. |
| Bevel / angled axis | The shaft angle and the two cone distances. There is no centre distance, since the axes meet; the pair is positioned by where each cone apex sits. | Mounting distance from the locating face to the apex, and the squareness of that face. This decides where the teeth contact along the face. |
| Compound or planetary | Two meshes sharing a member or a carrier. Each mesh has its own centre distance, and one part has to satisfy both. | Every bore position measured from a single datum, because an error in one mesh reappears as an error in the other. |
Note. These are geometric relationships, not acceptance values. How far a pair may depart from them is a design decision belonging to the mating gear, the load case and the acceptable play, and it is the first thing a gear review asks for. Profile shift is the usual exception: a shifted pair moves its working centre distance by design, so a drawing that quotes only the nominal value is checking the wrong number.
The three guides below take each tooth form from this framework to its own drawing requirements: spur and compound gears, helical gears and bevel gears.
The part drawing and its assembly determine the manufacturing route and the inspection plan.
Tooth count, module or pitch, pressure angle, face width and helix data where applicable.
Bore fit, face datums, runout and mating component information.
Torque, speed, shock, noise, lubrication and duty cycle.
Agreed tooth, dimensional and assembly checks for sample approval.
Three reference tables for gears and transmission parts: the grades that are actually used for teeth, where the forming routes stop, and how a gear moves from drawing to first article.
| Grade | Condition | Yield / UTS (MPa) | Elong. | Hardness | Density (g/cm³) | Why it is used here |
|---|---|---|---|---|---|---|
| 4600 (Fe-8Ni) | Sintered | 265 / 410 | 25% | 70–90 HRB | 7.60 | The baseline gear steel. Cheap, dimensionally stable and forgiving, which is why most unhardened drive gears start here. |
| 4600 (Fe-8Ni) | Heat treated | 450 / 900 | 10% | 500–600 HV | 7.60 | The same alloy after hardening: roughly double the strength, at the cost of elongation and a heat-treat step in the schedule. |
| 4605 (Fe-2Ni) | Sintered | 500 / 700 | 11% | 70–100 HRB | 7.50 | Higher as-sintered strength for loaded teeth without going to a full hardening route. |
| 4140 (42CrMo4) | Heat treated | 1400 / 1405 | 5% | 40–45 HRC | 7.50 | High-load gears, shafts and connecting rods. The strength ceiling of the alloy set on this page. |
| 316L | Sintered | 250 / 498 | 40% | 110–160 HV | 7.75 | Gears in wash-down, food or marine environments. Low strength, but it will not rust in service. |
| 17-4PH | Sintered → aged | 720 / 900 → 1070 / 1160 | 11% → 7% | 20–25 → 35–45 HRC | 7.50 | A middle path: corrosion resistance close to stainless with strength approaching the low-alloy grades. |
Values are reference ranges from the SINTS material summary measured on test pieces, not on a specific tooth form. Tooth root strength depends on density at the root, not on the tensile value alone — see the limits table below.
| Requirement | Powder compaction | MIM | What it means here |
|---|---|---|---|
| Tooth form as formed | Spur and helical teeth are pressed to net shape | Compound gears, undercuts and cross-features are moulded in one piece | The more features that must be cut after sintering, the smaller the advantage of either forming route |
| Bore and shaft fit | Sized or reamed after sintering | Sized or reamed after sintering | The bore is the datum for every gear check, so it is almost never left as-sintered |
| General dimension, as sintered | Roughly ±0.3–0.5% of the dimension | Roughly ±0.3–0.5% of the dimension | Tooth-to-tooth error matters more than absolute size for noise and backlash |
| Density at the tooth root | Density follows compacting pressure and mass distribution | Same, with more freedom in geometry | A gear that reaches full density at the rim and not at the root fails at the root |
| Hardening route | Sinter-hardening in the furnace, or quench and temper after | Same, plus the option to mould a hardened insert seat | Choose the route before the alloy: 4600, 4605 and 4140 harden to very different results |
| Economic volume | Tooling-led; reviewed against annual demand | Tooling-led; reviewed against annual demand | As a rule of thumb, below a few thousand pieces a year, cutting a gear can be cheaper than tooling for it |
Percentage tolerances follow the published MIM tolerance note and are planning arithmetic, not a capability claim. Gear accuracy is normally specified separately as a grade plus backlash and runout limits — see the gear RFQ checklist.
| Stage | Typical lead time | What you receive | What we need from you |
|---|---|---|---|
| Drawing review and DFM feedback | Issued with the quotation | Feature-by-feature route proposal, tolerance and finishing notes, and the open points that must be answered before tooling | 2D drawing with tolerances and datums, STEP model, target annual volume, material or the performance requirement |
| Tooling | 25–30 days as quoted on recent programs | Mould or die built and released to trial condition | Approval of the DFM report and confirmation of the alloy |
| T0 samples | 7–10 days after tooling release as quoted on recent programs | Parts plus a dimensional report against the drawing | Agreed inspection plan and datum scheme |
| Sizing, finishing and heat treatment | Runs inside or immediately after the sample stage | Sized and finished parts, hardness and density results where specified | Which features must be held after sintering, and which may be finished |
| First-article report | With the first approved samples | Dimensions, material, hardness and density measured in-house rather than subcontracted | Drawing with the critical characteristics marked |
| Production release | After sample approval | Serial production to the agreed inspection plan | Confirmed annual volume, MOQ and packaging |
Tooling and sample durations above are the lead times quoted on recent programs of comparable size, not a standard promise; the schedule for a specific part is confirmed with its quotation. Every result in the first-article report is measured on the instruments listed on the capabilities page.
Gears and transmission components transfer rotation and torque between shafts. These answers cover tooth geometry, mounting interfaces, backlash and how process route follows from the load case.
Spur, helical and planetary gears produced in repeat volume are the classic candidates, along with compound gears that combine a gear profile with a hub or boss, and bushings that support the same shaft. Suitability then depends on tooth loading, density, required accuracy, backlash and whether the gear needs a heat treatment or a machined bore afterwards.
Yes, and that is usually where MIM earns its place: a gear combined with a cam, a one-way feature, a splined hub or a lever arm that would otherwise need a second part or a second operation. When the geometry is essentially a gear and a bore, powder metallurgy is normally the better fit, and when it is essentially an axisymmetric hub, turning is.
Specify them as functional requirements tied to the meshing pair, not as one overall tolerance. Backlash, tooth-to-tooth variation, runout and center distance each affect noise and life differently, and a gear that meets a general dimensional tolerance can still run rough if backlash or tooth form drifts. Stating the mating gear and the acceptable noise or play gives the review something measurable to work against.
A significant one, because the gear's accuracy in the assembly depends on how it is located as much as on the teeth. Bore diameter and tolerance, concentricity between bore and pitch circle, keyway or spline features, hub length and face datum all determine whether the tooth geometry is actually used as designed. Machining or reaming of the bore after sintering is common for exactly this reason.
Peak load, fatigue duty, shock and lubrication should be reviewed together. Static tooth strength, fatigue at the tooth root, surface wear at the flank and any shock or reversing condition each point to different density, alloy and heat-treatment choices, and the same nominal gear can need a different treatment for a steady drive than for an intermittent one. Sharing stall and impact conditions makes the material recommendation meaningful.
Send complete tooth data, the mating gear, installation dimensions, working load, material condition and annual quantity.
These are review inputs, not fixed catalog specifications. Supply the drawing revision and identify any requirements still to be confirmed.
Define gear geometry, mating interfaces, duty and final condition before comparing a drawing-based quotation.
Read the guide →PM & GearsReview which gear features need sizing, machining or heat treatment, and how the final inspection sequence should follow them.
Read the guide →