
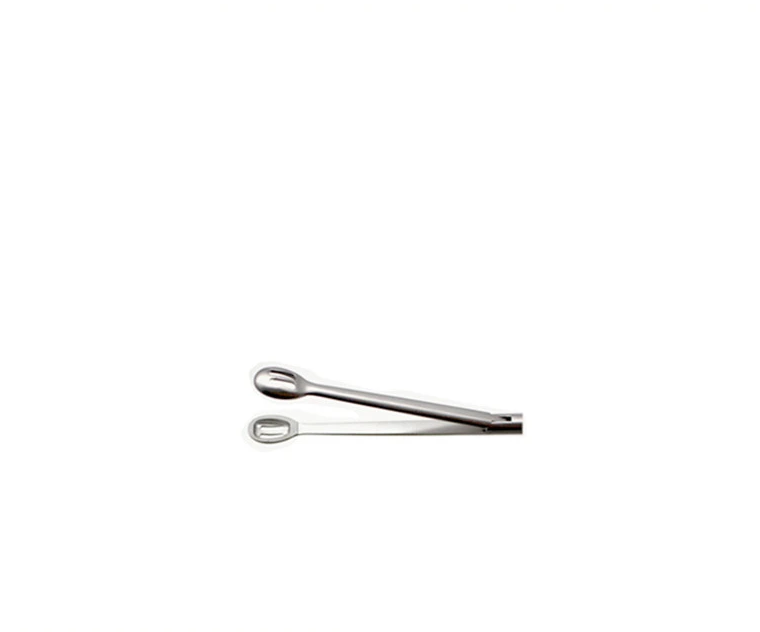
What a 17-4PH instrument project needs beyond the grade
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
The lung-pliers description is a source reference, not a clinical indication or verified finished instrument.
Jaw drawing, mating pair, pivot and actuation interfaces
Provide the jaw or link drawing, mating pair, pivot and actuation arrangement.
State which material specification and final condition the project requires.
Why state the final condition of a specified instrument alloy?
The grade name does not fully describe the delivered material and processing requirements.
Stating the final condition connects material records with component inspection.
The instrument design and its validation remain separate from the use of a particular alloy designation.
MIM versus machining against compact features
Compare MIM and machining against the compact features and inspection needs.
Heat treatment and finishing must be part of the agreed route rather than implied by the grade name.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →17-4PH condition, surface and traceability requirements
Provide the material specification, final surface requirements and documentation needed for the component.
Cleaning, traceability and device-related validation must follow the customer project.
The catalog reference does not establish medical compliance or an intended clinical use.
Review material-selection information →Geometry, material record and paired-movement checks
Check geometry, material records, final condition and paired movement.
Any cleaning or device-level validation is governed by the customer's project requirements.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →How 17-4PH instrument jaws and links fail, and where the condition matters more than the alloy
Writing 17-4PH on a drawing settles the alloy but not the part. The same grade in a different condition has different strength, different corrosion behaviour and different behaviour at the pivot, and the failures below split along that line.
| What goes wrong in service | What drives it | Where the drawing closes it out |
|---|---|---|
| Staining and discoloration after repeated steam cycles | The high-strength condition of a precipitation-hardening stainless is a compromise: it gives up some corrosion resistance to gain strength. Repeated steam, cleaning agents and chloride traces find that trade-off, especially in crevices at the pivot. | The condition stated with the strength requirement it is there to meet, plus passivation as a required step; verified by a cyclic cleaning test on assembled instruments, since a single-part salt-spray result says little about a hinge crevice. |
| The jaws do not meet evenly along their length | Jaw alignment comes from the pivot holes and from how the pair was matched. Two jaws each inside their own position tolerance can still open a gap at the tip, and the gap is what the surgeon reports. | Pivot hole position and fit stated per part, plus a requirement on the assembled pair at the tip; verified by closing a mated pair on a gauge and checking contact along the jaw, not by CMM on the single part. |
| The pivot stiffens after cleaning | A tight bore plus a roughened surface after a few cleaning cycles is enough. The instrument is not damaged, but it no longer feels like the same tool. | Bore finish and the pin fit stated with the finish included, plus the pin material named; verified by an opening-force measurement after cycling rather than at first assembly. |
| A crack starts at the internal corner of the jaw window | The window corner is a sharp internal feature in a thin section, and it is exactly where sintered material has the least margin. A radius too small to matter on the drawing decides the fatigue life. | Internal corner radii called out explicitly on the load-bearing side, with a section thickness minimum in the same area; verified by a fatigue or repeated-load test on parts taken from the production process, since the corner is where porosity concentrates. |
| The link fatigues at its thinnest section | Density in a compacted part varies with section thickness. The thinnest section is not only the weakest geometrically but often the least dense, and the two effects multiply. | Minimum section thickness stated together with a density requirement located at that section; verified by metallographic sectioning and by a load-cycle test, not by a single static pull. |
Note. The table names service failure modes and the drawing features that address them; it sets no acceptance values. Dimensions, tolerances and test criteria come from the project drawing.
The condition and the crevice are the two items that decide corrosion behaviour, and neither is a manufacturing tolerance: they are choices made on the drawing that a shop can only follow. Jaw alignment and pivot feel are assembly requirements, so they can only be judged on a mated pair. The two cracking items are where process control actually earns its place, because corner radius and section density are set by tool design and compaction, and both are invisible on the delivered part until they fail. In a device where the paperwork matters as much as the part, it helps to state which item is being controlled by design and which by process, because the validation evidence differs.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Is the alloy name enough to define the delivered material condition?
No. Specify the applicable material requirements, processing condition and evidence needed for acceptance.
Why state the final condition of a specified instrument alloy?
The grade name does not fully describe the delivered material and processing requirements. Stating the final condition connects material records with component inspection. The instrument design and its validation remain separate from the use of a particular alloy designation.
What must the sample approval requirements define?
Check geometry, material records, final condition and paired movement. Any cleaning or device-level validation is governed by the customer's project requirements.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →