
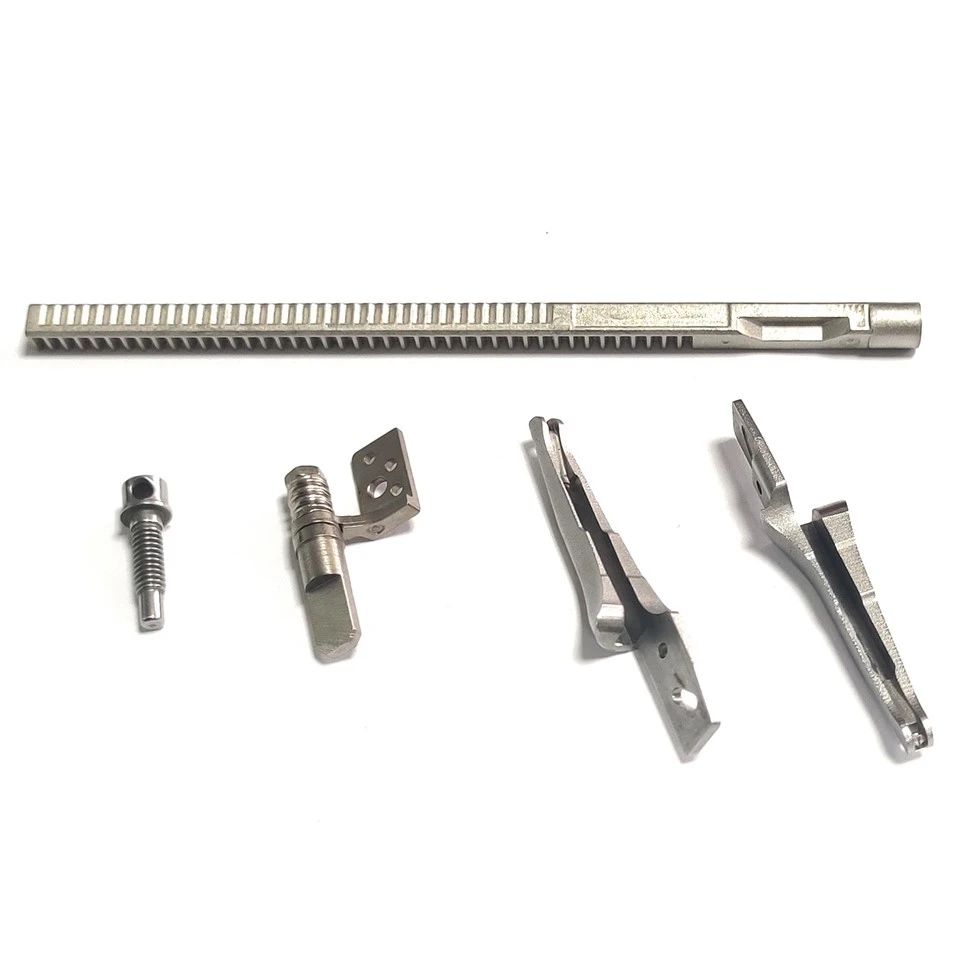
What instrument racks, links and pins each do in a mechanism
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
This reference group is intended for selecting the individual part to review.
Selected component drawing, mating parts and movement-path interfaces
Provide the selected component drawing, mating parts and movement path.
For a rack, define tooth engagement; for a link or pin, define its connection and guiding interfaces.
Why distinguish racks from links and pins in an instrument?
Each transfers or controls movement differently.
A rack needs a defined tooth relationship, while links and pins need defined joints or guidance.
Separating those functions avoids applying a single generic accessory specification to several mechanically different parts.
Comparing routes per geometry rather than per group
Compare forming and machining for each geometry instead of assigning one process to the group.
Working teeth, holes or sliding surfaces may need secondary finishing.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Instrument rack and linkage material, surface and traceability requirements
Provide the material specification, final surface requirements and documentation needed for the component.
Cleaning, traceability and device-related validation must follow the customer project.
The catalog reference does not establish medical compliance or an intended clinical use.
Review material-selection information →Functional geometry, movement clearance and surface checks
Check the chosen part's functional geometry, movement clearance and final surface.
Agree material and inspection records appropriate to the project.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Which features of a rack, link or pin move between lots
A rack, a link and a pin fail in different ways, so they do not share one list of drifting features. The one thing they have in common is that the functional feature is a relationship rather than a size.
| What drifts between lots | Where the drift comes from | What the release check catches |
|---|---|---|
| Rack tooth pitch and cumulative error | Tooth form is set by the mould, but pitch accumulates error over the length. A rack that is correct at both ends can still be out in the middle if shrinkage varied along the part. | Check pitch over the full toothed length, not over a few teeth. State the datum end and the length over which the total error applies. |
| Link hole distance | Hole distance depends on shrinkage along the link and on how the holes are finished. A change in sintered density moves both holes relative to the ends and relative to each other. | Check hole to hole, and check hole to end as a separate item. Only the first describes how the linkage moves. |
| Pin diameter and straightness | Pins are usually sized or ground, and the same tool wear that widens a bore narrows a pin over time. Straightness is affected by sintering and by how the pin was supported in heat treatment. | Gauge pin and hole as a pair, and check straightness over the working length. A pin that is straight overall can still be bent where it carries load. |
| Surface roughness on a sliding or guiding surface | Roughness depends on the finishing sequence. A tumbled surface and a ground surface can measure the same overall size and behave very differently in a sliding joint. | Specify roughness on the surface that guides or slides, and check it there. Roughness quoted without a location tends to be measured wherever it is convenient. |
| Material and heat records per lot | Slender parts are often made in small lots, which means more lots and more chances for a record to be separated from its parts. | Tie the material certificate and any heat treatment record to the lot, and keep that link through finishing. For instrument work this is usually the first document a customer asks for. |
Note. This describes how the process behaves across a production run, not the history of any particular lot. Acceptance values, sample sizes and inspection methods come from the project drawing and the agreed quality plan.
A rack is inspected over its length, a link between its holes, a pin against its hole. Each is a relationship that a single-part drawing can state and a set of independent dimensions cannot. Where the drawing gives only sizes, the functional feature becomes an assembly surprise.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Can a reference group be quoted as one product?
Identify each part and quantity in the bill of materials; their geometry, finishing and inspection requirements can differ.
Why distinguish racks from links and pins in an instrument?
Each transfers or controls movement differently. A rack needs a defined tooth relationship, while links and pins need defined joints or guidance. Separating those functions avoids applying a single generic accessory specification to several mechanically different parts.
What must the sample approval requirements define?
Check the chosen part's functional geometry, movement clearance and final surface. Agree material and inspection records appropriate to the project.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →