
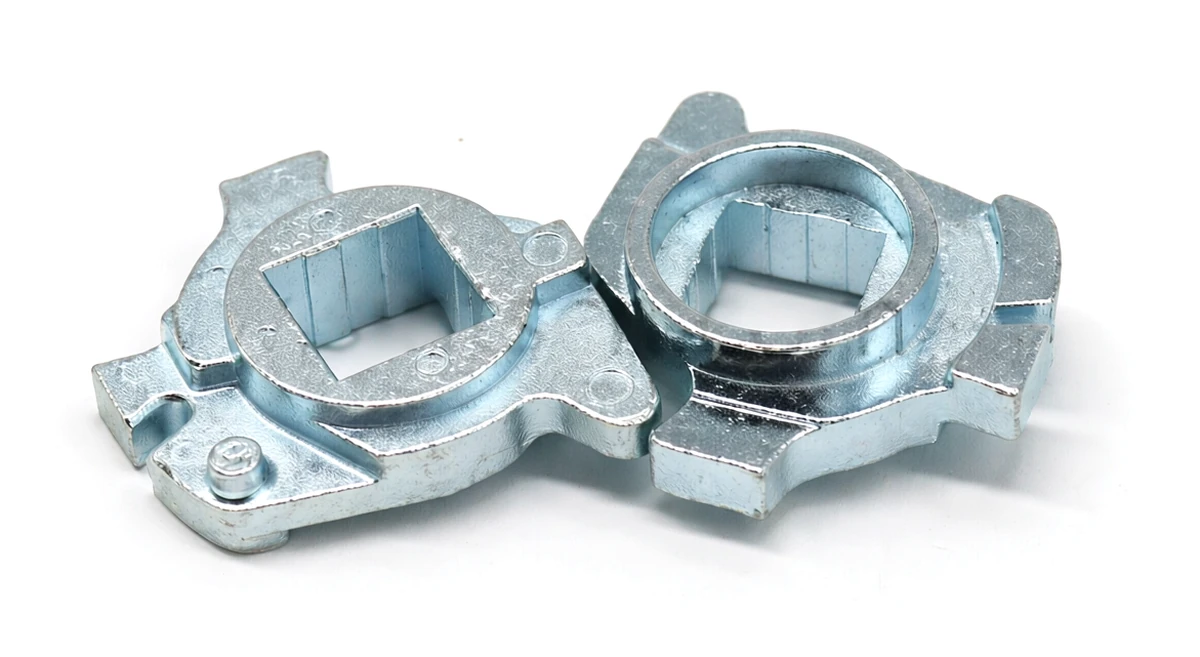
What a zinc-plated spindle transfers through a plated interface
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
Define the spindle profile, mating parts and final plated condition on the drawing.
Spindle profile, coupling and retaining-arrangement interfaces
Identify the spindle profile, coupling and retaining arrangement.
Mark dimensions that must be met after plating and the faces that engage the mating drive.
Why define the final inspection condition for plated hardware?
The delivered surface is part of the working fit.
A measurement taken at an earlier production stage may not describe that condition.
An explicit final-state requirement connects the material, coating and dimensional acceptance without leaving the comparison ambiguous.
Machining, forming and the plating sequence for spindles
Compare machining and forming for the requested member, then specify the plating and final inspection sequence.
Base material and coating are separate requirements.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Zinc-plated spindle substrate, coating and dimensional requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
The component specification does not establish a security rating for the complete lock.
Review material-selection information →Final engagement, retention and surface-condition checks
Check final engagement, retention and surface condition.
Include any customer-defined corrosion or dimensional acceptance after coating.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Where zinc-plated spindles fail, and why plating sequence decides it
A lock spindle is a torque path with two drive ends and a plating on top. The plating is applied after the geometry is finished, so it changes the very dimensions the spindle is judged on, and it does so unevenly at exactly the features that carry the load.
| What goes wrong in service | What drives it | Where the drawing closes it out |
|---|---|---|
| Zinc flakes off the square drive | The corners of a square drive are edges, and edges take a thicker, more brittle deposit because current density concentrates there. Under torque the coating on the corner fails first, and flaking starts where the spindle is supposed to transmit load. | Edge condition at the drive ends stated on the drawing, plus an adhesion requirement checked after torque rather than on a flat witness panel; verified by driving a sample to the specified torque and inspecting the corners afterwards. |
| White corrosion product appears in storage | Zinc protects by sacrificing itself, and the white product is that sacrifice happening. Without a passivation over the zinc, or with passivation damaged by handling, it starts in the bag before the part is ever installed. | Passivation type named, and handling and packing stated so the passivation is not rubbed off; verified by a humidity test on packed parts, since the failure is a storage failure rather than a service one. |
| Hardened spindles crack at the corners | The same acid cleaning that prepares the surface for plating introduces hydrogen, and a hardened substrate holds it. Cracks appear after installation, at the corner where the stress already concentrates. | Substrate hardness on the drawing, with the baking window after plating made mandatory at that hardness; verified by a sustained-load test on plated parts rather than by visual inspection, which cannot see it. |
| The spindle no longer fits the follower after plating | Plating adds thickness to every face. A clearance sized on the machined part closes by roughly twice the coating thickness on a bore fit, and unequally on a square because corners build faster. | All fits and the overall length specified in the final plated condition, with the pre-plate dimensions treated as process dimensions; verified with the production follower after plating, not with a gauge at nominal. |
| The spindle twists under load | Substrate hardness and the unsupported length between the drive and the follower decide this, and both are easy to leave off a drawing that focuses on the plating. | Substrate hardness or a stated torsional limit, plus the support span identified; verified by a torque test to a stated limit with the part held as it is in the lock, not in a smooth-jaw vice. |
Note. The table names service failure modes and the drawing features that address them; it sets no acceptance values. Dimensions, tolerances and test criteria come from the project drawing.
Every item here is created by the order of operations rather than by the geometry. The flaking, the fit loss and the twist all come from plating being specified as a finish instead of as a step that changes dimensions and properties. That is why a plated spindle drawing is only complete when it says which condition the tolerances apply to. The two items that a shop can control without a drawing change are passivation integrity and the baking window, and both of those are worth naming because they are invisible until the parts are in a bag or in service.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Should spindle fit be checked before or after plating?
The drawing should state the final required condition; working fit normally needs verification in the delivered condition.
Why define the final inspection condition for plated hardware?
The delivered surface is part of the working fit. A measurement taken at an earlier production stage may not describe that condition. An explicit final-state requirement connects the material, coating and dimensional acceptance without leaving the comparison ambiguous.
How should the completed mechanism be checked?
Check final engagement, retention and surface condition. Include any customer-defined corrosion or dimensional acceptance after coating.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →