
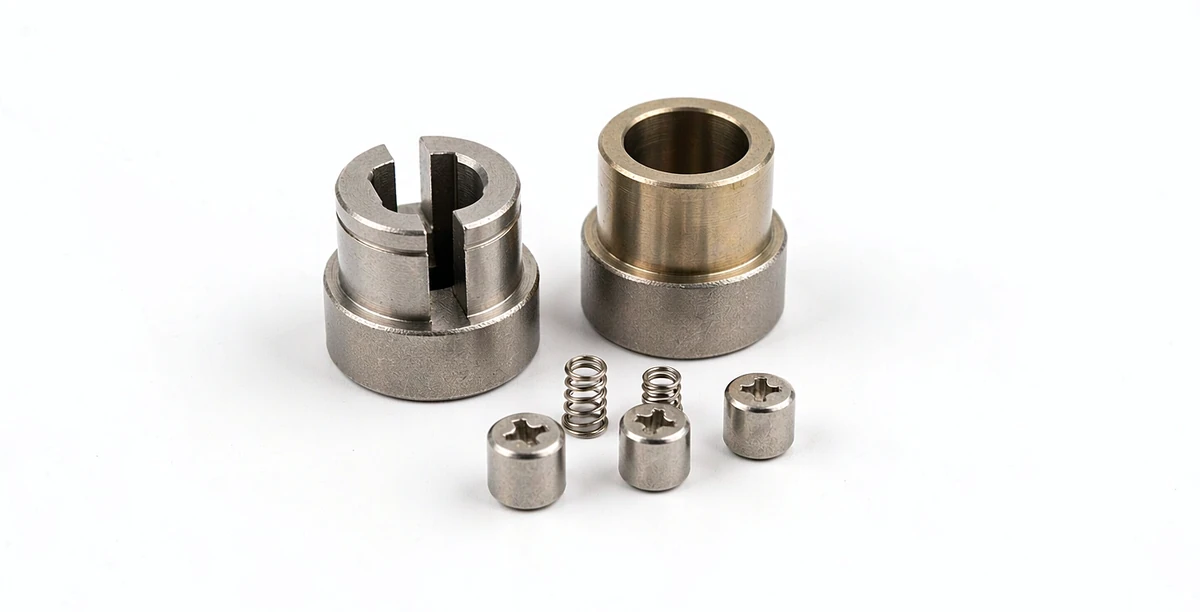
What traditional lock core parts coordinate in the mechanism
The individual core member must be identified before assigning material or production requirements.
Core assembly, drive profile and pin-to-retainer interfaces
Provide the core assembly, drive profile and relationship to pins, retainers or other mating elements.
Mark the critical guide and engagement features.
Why review a lock core as a sequence of interfaces?
Drive, guidance and retention occur at different locations in the core.
A component contributes to that sequence through its own features.
Showing the mating arrangement makes it clear which relationships must be preserved during manufacture and checked at assembly.
MIM versus machining for compact core geometry
Evaluate MIM for integrated compact geometry alongside machining for simpler axes and openings.
Secondary finishing may be needed where fit controls core operation.
Compare manufacturing capabilities →Lock core material, treated-surface and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
Specify any testing required on the assembled lock separately.
Review material-selection information →Drive fit, retention and freedom-of-movement checks
Check drive fit, retention and freedom of movement in the completed core.
Define any required durability or security evaluation at the assembly level.
Quality documentation →Where MIM earns its place in a pin-tumbler core
The case for moulding a traditional pin-tumbler core is not precision for its own sake. It is the number of features that would otherwise be cut one at a time: chambers, ribs, bosses, the plug bore and the mounting face. The review is a count of features against the moulding cost, and then a hard look at the walls between them.
| Feature | What it governs | How it is specified and verified |
|---|---|---|
| Integrated feature count | Whether one moulded body really replaces several machined pieces, which is the only reason to mould it. | Bosses, ribs and chambers listed on the 3D model and compared against a machined alternative in the DFM review. |
| Wall section between adjacent chambers | Sintering distortion and chamber straightness, which decide whether the pins still drop. | Minimum wall between chambers marked up before quoting; distortion checked by sectioning and CMM on the first article. |
| Shear line definition | Pin seating and the feel of key rotation across the full turn. | Position of the shear line relative to the plug datum, stated on the drawing; CMM, not a functional guess. |
| Gate and ejector position | Whether witness marks land on a visible or a functional surface. | Gate and ejector locations agreed and drawn on the DFM sheet before the mould is cut; the part drawing then carries the requirement. |
| Sizing versus cutting | Which features can stay net-shape and which need a finishing cut, which sets both price and lead time. | Two lists on the DFM sheet: features held by sizing, features requiring cut. Nothing moves between those lists without a drawing revision. |
Use the dimensions and acceptance criteria on the project drawing.
Moulding a core stops paying when the feature count is low or when several walls fall below the thickness the sintering step can hold without support. It also stops paying on large bodies where a compact-and-sinter route reaches the same shape, because powder metallurgy presses are cheaper per part than moulding and debinding at that size.
What to include in your enquiry
- Drawing and mating dimensions.Provide the core assembly, drive profile and relationship to pins, retainers or other mating elements. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Check drive fit, retention and freedom of movement in the completed core. Specify the mating part or inspection fixture.
Common questions
Can the core component be supplied from a sample only?
A sample can support initial identification, but the drawing, material and acceptance criteria need agreement before manufacture.
Why review a lock core as a sequence of interfaces?
Drive, guidance and retention occur at different locations in the core. A component contributes to that sequence through its own features. Showing the mating arrangement makes it clear which relationships must be preserved during manufacture and checked at assembly.
How should the completed mechanism be checked?
Check drive fit, retention and freedom of movement in the completed core. Define any required durability or security evaluation at the assembly level.