
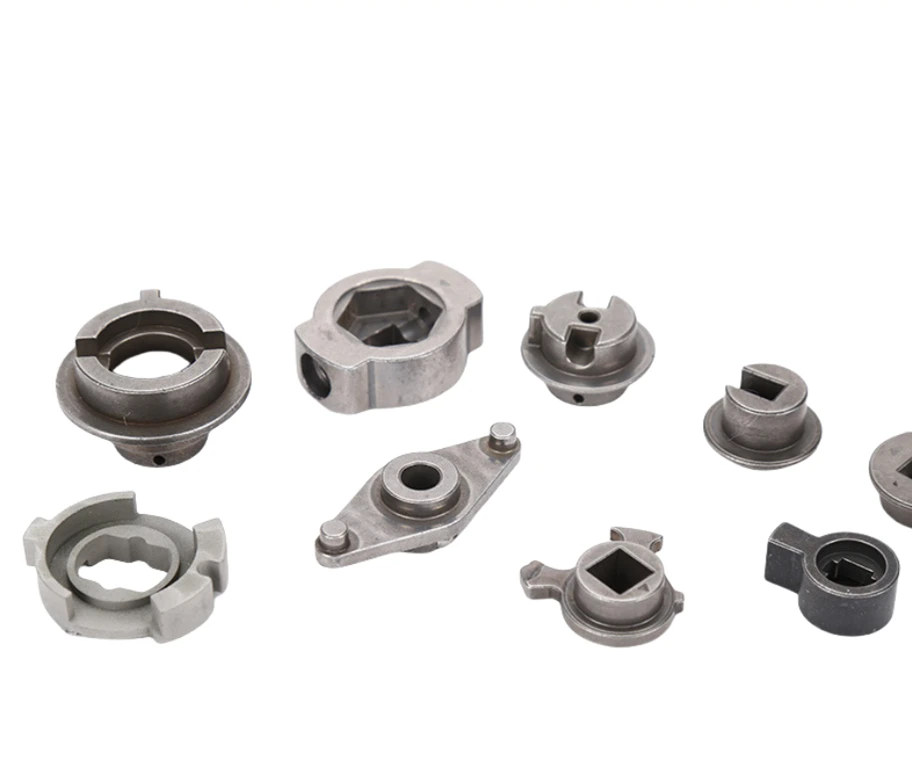
What integrated lock components combine in a compact form
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
The reference group illustrates several potential functions.
Drive, retaining and contact-feature interfaces
Separate the drive, retaining and contact features on the drawing.
Identify how their relative position controls the mechanism.
Why identify integrated features individually?
Integration can reduce the number of separate parts, but each drive, contact and retaining feature still has a function.
Separating those requirements on the drawing makes their relationships inspectable and shows where final operations may still be required.
MIM versus machining for integrated lock geometry
Evaluate MIM for the integrated geometry while comparing machining where simpler features dominate.
Include any post-forming operations needed for the critical interfaces.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Integrated lock component material, treated-surface and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
The component specification does not establish a security rating for the complete lock.
Review material-selection information →Feature relationship, drive engagement and treated-dimension checks
Check feature relationships, drive engagement and final dimensions after treatment.
Approve the component in its actual lock function.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →What sets the cost of a short run of integrated MIM lock parts
An integrated part is usually chosen to remove assembly steps, and the saving it creates is real. It also front-loads cost into tooling, so the first run carries a burden the tenth run does not. The five items below are where that burden sits.
| Cost element | Why a small order costs more per piece | Why a large order stops getting cheaper |
|---|---|---|
| Mould, sizing tool and furnace setters | Three separate tooling items can exist before a single part is sold. Integration adds cavities and slides, and each one raises the mould price. On a short run the tooling is spread over very few parts, so it dominates the piece cost. | Tooling is recovered and then stops moving. What comes back later is a second mould when the first reaches the end of its life, and that step does not get cheaper with volume. |
| Compounded feedstock | Feedstock is compounded in a batch and has a limited working life, so a small order still consumes a batch. Unused material cannot be held indefinitely, which puts a floor under the material line. | Material is the one line that tracks the metal market rather than the order size. Beyond a certain point the price per kilogram does not fall, so volume cannot push it down. |
| Debind and sinter as a batch process | The furnace runs a cycle whatever it contains. A partly filled load spreads the cycle cost over fewer parts, and this is often the largest single difference between a trial batch and a production batch. | A furnace has a fixed cycle time and a fixed load. Once it is full, more volume means another cycle or another furnace, and neither reduces the cost per part. |
| Sizing, where the drawing requires it | Sizing is one part at a time through a press. Labour and handling per piece are high, and on a small order there is no way to spread them. | Automated handling or a design change that removes the sizing step can cut this line, but both need investment and re-qualification. Beyond that, a per-piece operation stays a per-piece operation. |
| First article and lot documentation | A first article report, dimensional layout and material record cost about the same whether they cover 500 parts or 50,000. On a short run they can exceed the material cost. | Sampling can be argued down to a limit, not to zero. Critical dimensions still get recorded per lot, so this line stays roughly constant per shipment rather than per part. |
Note. The split below describes cost structure, not prices. What a specific part costs depends on its geometry, material, finish and the quantity you can commit; this page explains which of those you can move and which you cannot.
Only the tooling and the furnace load change substantially with quantity. Material and documentation barely move, and a per-piece finishing step stays per-piece. That is why doubling a small order rarely halves the piece price, and why the real savings happen at the design stage: one less sizing step, one less machined face, one less inspection fixture.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Does near-net forming eliminate all lock-part machining?
No. Close fits, threads or contact surfaces may still need machining or another finishing operation.
Why identify integrated features individually?
Integration can reduce the number of separate parts, but each drive, contact and retaining feature still has a function. Separating those requirements on the drawing makes their relationships inspectable and shows where final operations may still be required.
How should the completed mechanism be checked?
Check feature relationships, drive engagement and final dimensions after treatment. Approve the component in its actual lock function.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →