
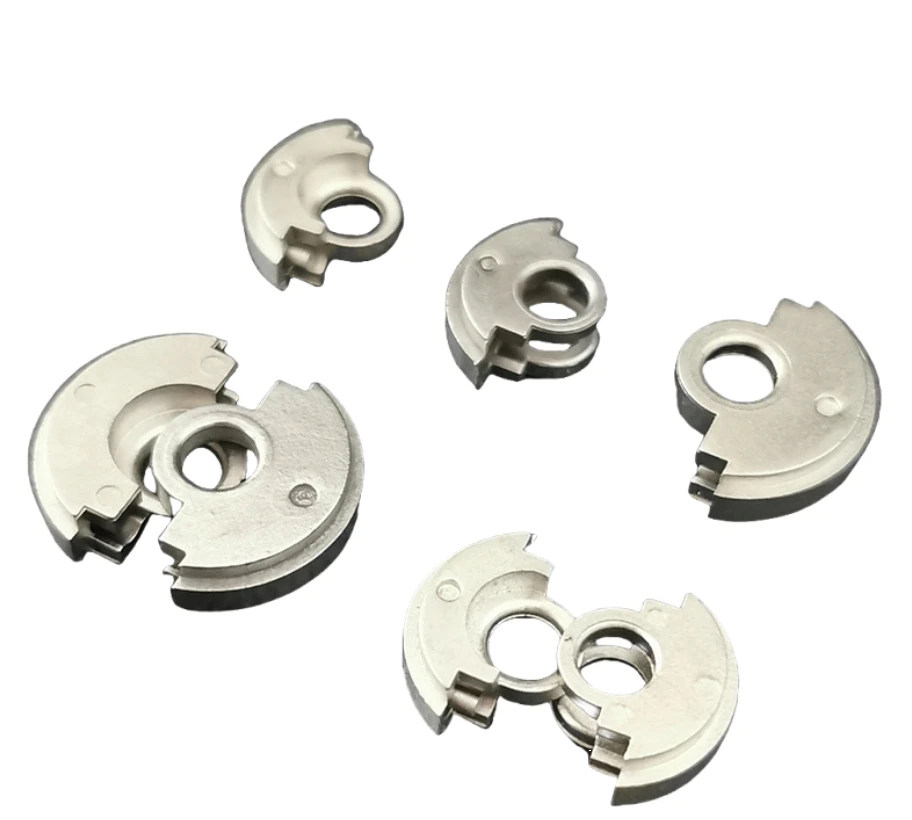
What cams and retainers coordinate in a security mechanism
The reference group illustrates shaped profiles around a central opening.
Central drive, rotation range and working-profile interfaces
Define the central drive, rotation range and the working profile.
Identify which edge drives another part and which provides clearance or retention.
Why relate the cam profile to its drive opening?
The working profile is positioned by the drive or locating interface.
Measuring the two without their angular relationship does not fully define the action.
A shared reference makes the intended engagement understandable in both manufacturing and assembly inspection.
MIM, PM and machining for cam profiles
Compare MIM, PM and machining against the profile and quantity.
Contact faces and drive openings may need finishing beyond the formed body.
Compare manufacturing capabilities →Cam and retainer material, treated-surface and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
Specify any testing required on the assembled lock separately.
Review material-selection information →Drive-to-profile relationship and engagement-clearance checks
Inspect the relationship between drive and profile, engagement clearance and finished surface.
Verify motion with the mating security mechanism.
Quality documentation →What sets the price of a cam and retainer set
A cam is cheap to form and expensive to verify, because what matters is the angular relationship between the drive and the profile rather than any single size. That shift from size to relationship is what moves cost.
| Cost element | Why a small order costs more per piece | Why a large order stops getting cheaper |
|---|---|---|
| The forming tool | A cam profile is cut into the tool, and the drive shape needs its own core. Both are one-off, and neither gets cheaper with a larger order. | Tooling is recovered early. A profile change later means a tool change, so the drawing should be settled before the tool is cut. |
| Coining or sizing | Where the profile has to be held closely, coining is a per-part press operation with its own tool. | Coining can be automated, but it remains a stroke per part. Removing it by holding the profile in the mould is a design and tooling decision, not a volume effect. |
| Heat treatment in a load | Hardening runs as a batch, and a small order still fills a furnace cycle or waits to share one. | Sharing a load with other work is the usual answer for small quantities, and it constrains the delivery schedule more than the price. |
| Edge and profile finishing | Deburring an engaging edge is where the part is judged. On a small order it is done by hand or in a short barrel cycle. | Automation is possible once the edge requirement is written as a dimension. As long as the drawing says deburr, the operation stays manual at any volume. |
| Fixture for the angular check | The relationship between drive and profile needs a fixture or a CMM programme. This is a one-off engineering cost that appears on every first order. | Once the fixture exists, checking is quick. Repeat orders on the same part skip this line entirely, which is why the second quotation often looks better than the first. |
For a price comparison, use the same material, finish, order quantity and inspection requirements.
Two of these five are one-off and two are per-part. The per-part ones can be reduced by writing the requirement as a dimension: a stated edge radius and a stated profile tolerance turn manual judgement into a measurable operation, which is the only route to a stable price at any volume.
What to include in your enquiry
- Drawing and mating dimensions.Define the central drive, rotation range and the working profile. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Inspect the relationship between drive and profile, engagement clearance and finished surface. Specify the mating part or inspection fixture.
Common questions
Can the outside cam profile be dimensioned independently of the drive?
Its angular and positional relationship to the drive is usually functional; specify the assembly relationship on the drawing.
Why relate the cam profile to its drive opening?
The working profile is positioned by the drive or locating interface. Measuring the two without their angular relationship does not fully define the action. A shared reference makes the intended engagement understandable in both manufacturing and assembly inspection.
How should the completed mechanism be checked?
Inspect the relationship between drive and profile, engagement clearance and finished surface. Verify motion with the mating security mechanism.