
What a custom lock cylinder request must define in supply scope
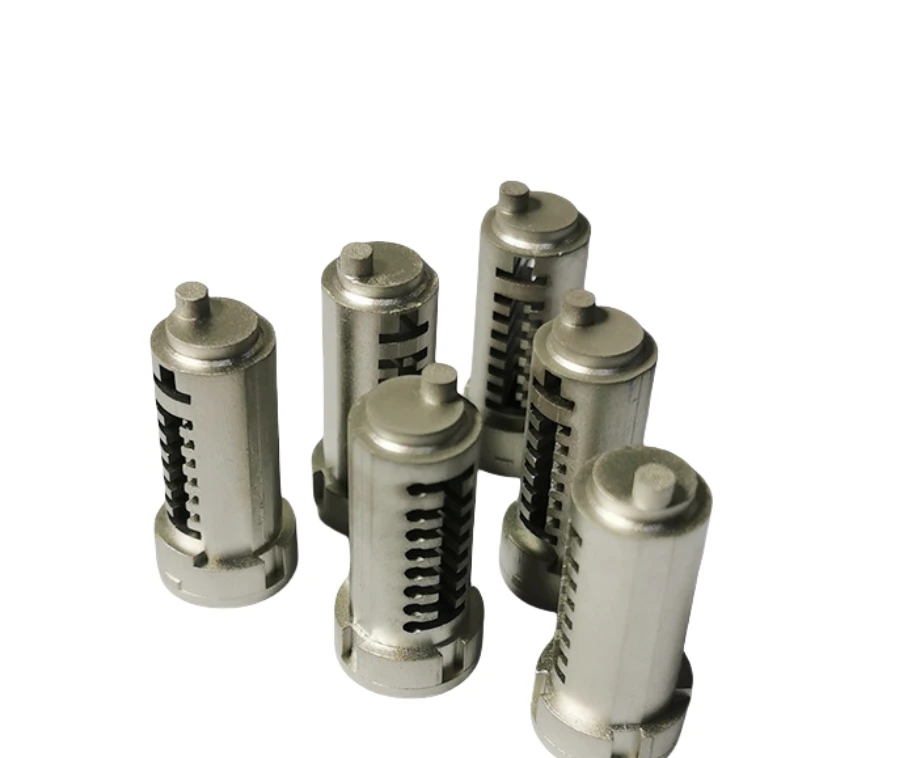
The reference shows repeated cylindrical forms with engagement features.
Supplied parts, slot-to-axis and end-connection interfaces
Identify each supplied part and the relationships between slots, axis and end connection.
Provide the assembly if multiple members work together.
Why define the cylinder bill of materials?
A cylinder assembly can contain several parts with different materials, processes and inspection needs.
A visible assembly does not identify all of them.
A bill of materials makes the supplied scope explicit and distinguishes component approval from assembled mechanism approval.
Reviewing machining and forming per individual part
Review machining and forming at the individual-part level.
Final assembly, inspection and any separate springs or pins must be included explicitly in the supply scope.
Compare manufacturing capabilities →Lock cylinder material, treated-surface and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
Specify any testing required on the assembled lock separately.
Review material-selection information →Slot position, guiding fit and engagement checks
Check slot position, guiding fit and required engagement.
Agree whether approval covers individual components or the assembled cylinder mechanism.
Quality documentation →Where the cost sits in a lock cylinder bill of materials
A cylinder is bought as a set of parts that have to work together, and each part carries its own tooling and its own finishing. The order size therefore applies to the whole set, not to the largest part in it.
| Cost element | Why a small order costs more per piece | Why a large order stops getting cheaper |
|---|---|---|
| Tooling across the bill of materials | Every part in the set needs its own tool. A five-part cylinder can need five tools before production starts, and the smallest part in the set can carry the most awkward tool. | Tooling is amortised once. Volume reduces the share per set but does not reduce the number of tools, and a long programme will eventually need replacements. |
| Freezing the reference before production | A cylinder is usually reproduced against an existing assembly, and turning that into a frozen drawing is engineering work regardless of quantity. A small order still needs the same reference settled. | The reference is settled once. Later orders reuse it, which is why a repeat order on a reproduced part is often proportionally cheaper than a repeat order on a new design. |
| Machining of slots, pin holes and end connections | Forming gives the blank; slots and cross holes are then cut one part at a time. On a small order this is a large share of the work. | Automatic or multi-spindle machining lowers the per-piece time, but the number of operations stays. Every additional cut face is a line item that volume cannot remove. |
| Plating rack space | Small parts are plated on racks, and a rack costs the same whether it is full or half full. A short run pays for rack space it does not use. | Plating scales with surface area and rack loading, which is close to linear. Beyond a full rack, the cost per part is essentially flat. |
| Assembly and pairing | Where the set includes a keyed relationship, parts are matched rather than picked at random. Matching is manual and does not shorten with a smaller batch. | Workstations can be split, but each set still needs its own match and its own function check. This is the line that volume helps least on a cylinder. |
For a price comparison, use the same material, finish, order quantity and inspection requirements.
The bill of materials is the thing to review before discussing quantity. Cutting one part out of the set, or moving a slot from a machined feature to a formed one, changes the cost structure more than doubling the order does. Volume only spreads the tooling; it does not simplify the set.
What to include in your enquiry
- Drawing and mating dimensions.Identify each supplied part and the relationships between slots, axis and end connection. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Check slot position, guiding fit and required engagement. Specify the mating part or inspection fixture.
Common questions
Are springs and internal pins included in the part quotation?
Only if they are included in the agreed bill of materials and assembly scope.
Why define the cylinder bill of materials?
A cylinder assembly can contain several parts with different materials, processes and inspection needs. A visible assembly does not identify all of them. A bill of materials makes the supplied scope explicit and distinguishes component approval from assembled mechanism approval.
How should the completed mechanism be checked?
Check slot position, guiding fit and required engagement. Agree whether approval covers individual components or the assembled cylinder mechanism.