
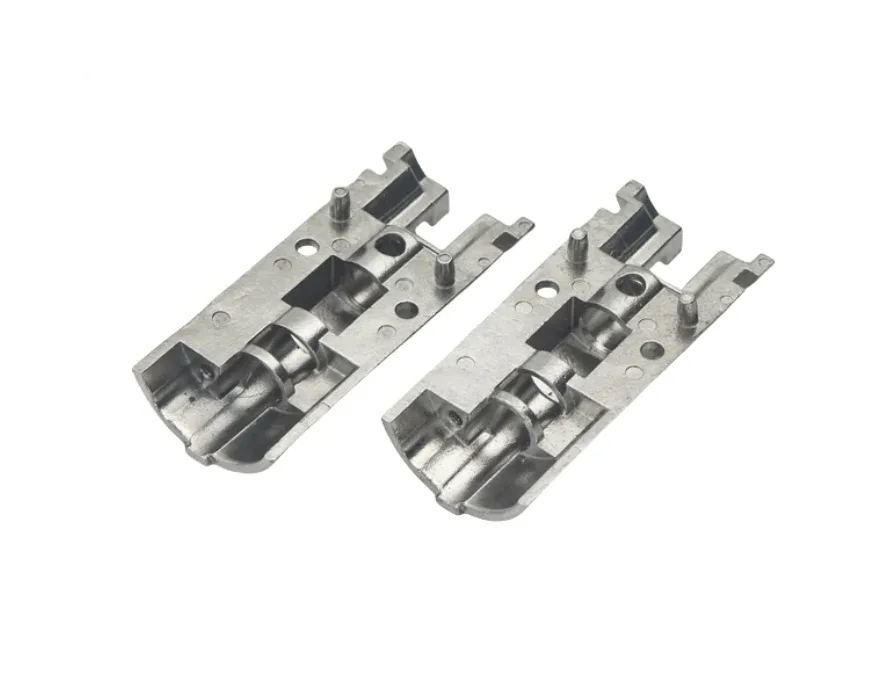
What support plates position within a lock body
The reference shows elongated components with cavities and mounting or guide features.
Supporting faces, locating holes and moving-member clearances
Identify the supporting faces, locating holes and clearances around the moving members.
Keep guide relationships consistent with the lock's assembly datums.
Why review cavities and guides with the moving members?
A cavity may provide clearance or position another part, while a guide controls movement.
The mating members reveal which surfaces are functional.
Reviewing them together avoids assuming that every recess is simply noncritical empty space.
MIM versus machining for integrated support geometry
Compare MIM and machining for integrated support geometry.
Recesses and working seats need review for tooling, finishing and inspection access.
Compare manufacturing capabilities →Support plate material, treated-surface and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
Specify any testing required on the assembled lock separately.
Review material-selection information →Mounting fit, guide alignment and travel-interference checks
Check mounting fit, guide alignment and interference through the mechanism's travel.
Inspect edges around moving or assembled parts.
Quality documentation →Where the cost goes on a thin support plate
A support plate looks cheap to make and is not, because most of its cost sits in operations that cannot be batched: keeping it flat, keeping the edges clean, and keeping it flat again after coating.
| Cost element | Why a small order costs more per piece | Why a large order stops getting cheaper |
|---|---|---|
| The forming tool | A thin plate needs a tool with a flat, well-supported face. The tool itself is not the expensive part; getting flatness out of a thin section is what drives the design. | Tooling is amortised quickly on a plate. What returns later is rework of the tool when flatness drifts, which is a maintenance cost rather than a volume cost. |
| Flatness correction | Sintered thin sections distort, and the correction is done part by part on a press or by hand. This is the line that makes a small order expensive. | Automated handling helps, but a plate that needs correction still needs it on every part. The better answer is a design change that removes the correction, and that is a one-off engineering decision. |
| Deburring of thin edges | Thin edges deform under bulk deburring, so the operation is often done with more care and less speed than on a solid part. | Barrel finishing scales, but thin parts limit the media and the time. The process window is narrow, so volume does not buy much speed. |
| Plating and rack handling | Thin plates need support on the rack to avoid distortion, which reduces how many fit per rack. | Rack loading is limited by the part, not the tank. Adding volume adds racks and handling, not efficiency. |
| Flatness inspection in the free state | Flatness has to be checked with the part unrestrained, which is slower than a go gauge and hard to automate. | Sampling can be agreed, but the check itself does not get faster. This stays a per-lot time cost. |
For a price comparison, use the same material, finish, order quantity and inspection requirements.
For a plate, the cheapest change is usually a small increase in thickness or a stiffening feature that removes the need for correction. That decision costs nothing in tooling terms and removes the largest single line. Discounting a thin plate is harder than designing a stiffer one.
What to include in your enquiry
- Drawing and mating dimensions.Identify the supporting faces, locating holes and clearances around the moving members. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Check mounting fit, guide alignment and interference through the mechanism's travel. Specify the mating part or inspection fixture.
Common questions
Can a support plate be approved using flatness alone?
No. Hole, cavity and guide relationships also determine whether the mechanism operates correctly.
Why review cavities and guides with the moving members?
A cavity may provide clearance or position another part, while a guide controls movement. The mating members reveal which surfaces are functional. Reviewing them together avoids assuming that every recess is simply noncritical empty space.
How should the completed mechanism be checked?
Check mounting fit, guide alignment and interference through the mechanism's travel. Inspect edges around moving or assembled parts.