
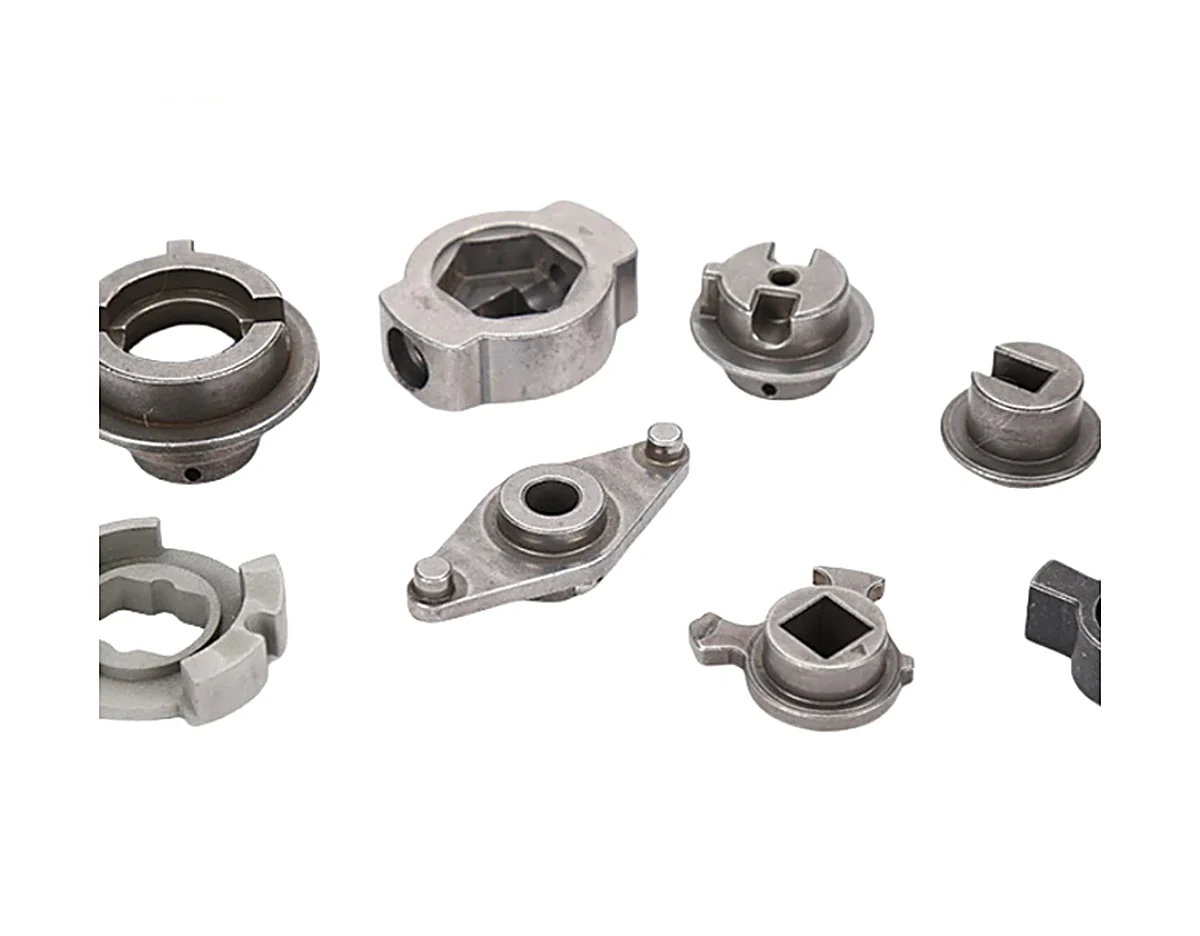
What lock core cams and drive inserts connect in the mechanism
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
The reference group contains several functions rather than one interchangeable part.
Exact member, central drive and engaging-profile interfaces
Identify the exact member, central drive shape and engaging profile.
Define angular orientation and the interfaces to the surrounding lock core.
Why separate drive inserts from retaining components?
A drive insert transfers movement, while a retainer holds another member in place.
Their similar scale does not imply the same critical features.
Identifying each role prevents a shared catalog photograph from becoming an unsuitable common specification.
MIM, PM and machining for cam and insert profiles
Compare MIM, PM and machining for the chosen profile.
Drive openings and working contacts should be reviewed for finishing and dimensional inspection.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Cam and insert material, treated-surface and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
The component specification does not establish a security rating for the complete lock.
Review material-selection information →Drive fit, angular relationship and core-engagement checks
Check drive fit, angular relationship and engagement in the core.
Specify whether the requested item rotates, retains or locates another component.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Which cam and insert features actually shift between lots
A cam is judged by where its profile sits, not by how large it is. Most of the variation between lots on this class of part therefore appears as an angular or positional shift that the overall dimensions do not reveal.
| What drifts between lots | Where the drift comes from | What the release check catches |
|---|---|---|
| Cam rise profile | The profile is set by the mould and then adjusted, if at all, by coining. Coining removes a fixed amount of material, so a lot that sinters slightly denser ends up with a profile a little lower than the lot before it. | Check the profile against the mating follower or a stated lift, using the drive as the datum, and check a part from the middle of the load as well as from the ends. |
| Angular position of the drive | The drive shape is formed by a core that can rotate slightly as it wears or as it is reset. The error appears as a rotation of the whole cam, so every reading taken from the drive moves together. | Measure the angular relationship between the drive and the highest point of the cam. Checking the drive size alone will not show a rotation. |
| Face parallelism where the cam runs against a housing | Both faces are usually sized. Parallelism depends on how the part seats in the sizing die, and a small tilt there survives into the finished part. | Check parallelism in the free state and state the datum face. Where the cam runs against a housing face, parallelism controls end play more directly than thickness does. |
| Hardness after heat treatment | Cam and insert parts are often through-hardened or case-hardened. Position in the load and section thickness both change the result, and a cam has thick and thin sections in the same part. | Agree the test location and use a coupon that travels with the load. A hardness figure quoted without a location cannot be reproduced on a re-check. |
| Edge condition on the engaging profile | Deburring is a manual or barrel operation whose result varies with media life and cycle count. Two lots can both be free of visible burrs and still differ in how sharp the engaging edge is. | Define the edge condition, for example a stated radius or a limit on material standing above the nominal profile, and inspect at magnification. A note that says deburr is not a specification. |
Note. This describes how the process behaves across a production run, not the history of any particular lot. Acceptance values, sample sizes and inspection methods come from the project drawing and the agreed quality plan.
Cams reward a drawing that states relationships rather than sizes. Where the drawing gives the lift and the angle from the drive, four of these five items can be checked without ambiguity. Where it gives only the outline, the same part can pass every dimension and still change the timing of the mechanism.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Should all parts in a lock-core group share one specification?
No. Identify each drawing and its function; cams, retainers and drive inserts have different critical interfaces.
Why separate drive inserts from retaining components?
A drive insert transfers movement, while a retainer holds another member in place. Their similar scale does not imply the same critical features. Identifying each role prevents a shared catalog photograph from becoming an unsuitable common specification.
How should the completed mechanism be checked?
Check drive fit, angular relationship and engagement in the core. Specify whether the requested item rotates, retains or locates another component.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →