
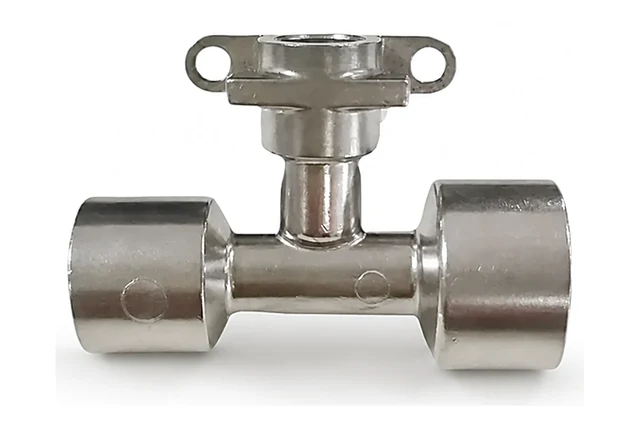
Valve-style geometry reference
This reference illustrates body, passage and moving-interface geometry. Supply scope follows the drawing.
Discuss a similar component →Metal component geometries for fluid-control and dispensing reviews, with attention to media exposure, fits and surface condition.
This reference illustrates body, passage and moving-interface geometry. Supply scope follows the drawing.
Discuss a similar component →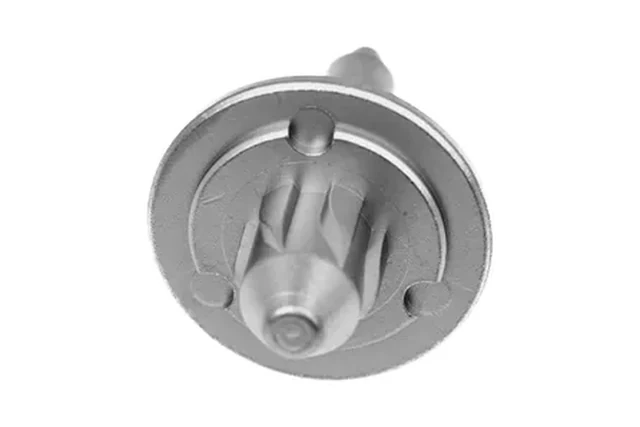
Used to discuss moving interfaces; not evidence of a qualified plunger or sealing component.
Discuss a similar component →Representative custom component references. Dimensions, material, manufacturing route and validation requirements are confirmed from your drawing; these are not off-the-shelf catalog items.
Seat carriers, cages, retainers and compact bodies where ports or integrated features can make near-net-shape production useful.
Reciprocating parts where straightness, sliding finish, impact, magnetic behavior or leakage can dominate the design.
Cams, levers, couplings and small gears that actuate metering or valve functions.
Small stainless parts exposed to beverage, adhesive, air or other media, with project-specific cleaning and compatibility requirements.
The parts in this group sit near each other because they all live in a flow path, but the flow path is not what they are specified against. Each one holds a different interface: a seat, a sliding clearance, a timing profile or a wetted surface. Which one it is decides who finishes the part and who tests it.
| Form in this group | The form it is nearest to | What decides between them |
|---|---|---|
| Valve-adjacent body or cage | Sealing body | Who owns the sealing geometry decides it. A carrier locates a seal that does the sealing, so its job is concentricity and seat flatness; a body that forms the sealing surface itself carries the finish and the leak test, and that finishing step does not disappear because the body was pressed near net shape. |
| Plunger | Shaft | The stroke decides it. A shaft holds a position; a plunger travels through a bore and has to keep its clearance over the whole distance. Straightness across the stroke, not diameter alone, is the requirement the drawing has to carry, and it usually forces a finishing operation. |
| Dispensing cam or lever | Mechanism cam | Whether the profile is a timing function or a force function decides it. A metering cam is specified by where the follower sits at each point of the stroke; a force cam is specified by contact stress and wear at the working flank. The same outline means two different things. |
| Media-contact part | Structural part in the same assembly | Whether the surface is wetted decides it. A wetted surface takes its grade, finish and cleaning requirement from the medium; a structural bracket beside it does not. Quoting both under one material line is what usually hides the mismatch until testing. |
| Near-net body with a finished seat | Fully machined body | Which feature is the expensive one decides it. If the ports and passages are the cost, near-net shape removes most of it; if the seat is the cost, the route only changes how the blank arrives at the same finishing operation, and the saving is smaller than the drawing suggests. |
Note. Cleanliness, food-contact suitability and pressure rating are program-specific and are not implied by a stainless grade or by the shape of the part. They are agreed as part of the supply and validation scope.
| Review area | Information to define | Manufacturing decision |
|---|---|---|
| Media & conditions | Fluid or gas, temperature, pressure, cleaning chemicals and exposure duration. | Confirm grade, corrosion and surface-treatment compatibility for the actual service. |
| Sealing interface | Mating seal, seat geometry, leakage criterion, surface finish and pressure-test method. | Plan critical-surface finishing and agree who performs component and assembly leak testing. |
| Motion & clearance | Stroke, guiding length, mating bore, cycle duty and contamination risk. | Review sliding fit, particle sensitivity and wear after finishing. |
| Cleanliness & scope | Particle limits, cleaning/packing requirements and any end-use documentation. | Confirm the component supply and validation plan; food-contact or pressure suitability is not inferred from shape. |
Material & final condition. Stainless grades may be candidates for corrosion-sensitive hardware. Material, porosity/density, surface finish and cleanliness are reviewed as a system. Machining remains part of the route where sealing or close sliding fits demand it. Review material data →
| Component / condition | First route to evaluate | Why / watchout |
|---|---|---|
| Feature-rich valve carrier / cage | MIM + critical finishing | 3D ports and integrated geometry may favor MIM; sealing bores/faces still require functional finishing. |
| Simple cylindrical plunger / stem | Turning / grinding | Axisymmetric precision motion and sealing surfaces usually favor machining. |
| Small actuation lever / cam | MIM or CNC | Complexity and repeat volume can favor MIM; contact profile and wear still need validation. |
| Micro nozzle / precision orifice | Micro-machining / EDM / laser | Do not default to MIM; hole geometry, roughness, concentricity and erosion can dominate performance. |
| Large manifold / valve body | CNC / casting / forging | Size, flow paths and finishing economics often make other processes more natural. |
Boundary: a near-net-shape body does not eliminate precision finishing on sealing, sliding or metering surfaces. Food-contact or chemical-compatibility status is also program-specific.
Review geometry, material and volume, identify critical features and clarify the proposed tooling and secondary operations.
Define trial parts, dimensional checks, material confirmation and any customer-required functional approval.
Confirm the approved route, control plan, packaging and repeat-supply requirements for the program.
Armatures, plungers, seats and valve interfaces.
Application guide →Plungers, guides, metering and valve-adjacent hardware.
Application guide →Valve, linkage and corrosion-sensitive stainless hardware.
Application guide →Utility-transfer inserts and compact fluid/pneumatic interfaces.
Application guide →State media, pressure/temperature, mating seals, leakage or clearance targets, cleaning requirements, drawing and annual quantity.
Practical answers from the drawing review, not from a brochure.
The interface the part has to hold: a seat, a clearance, a timing profile or a wetted surface. Whichever of those carries the function decides both the process and the inspection.
It can form the geometry, but the surface and flatness a seal needs may require a finishing operation. Whether that is needed follows from the leak or pressure requirement rather than from an assumption.
The media it contacts, the corrosion requirement, and any cleanliness or extractable limit. Those decide the alloy and the post-sinter steps as much as the shape does.