
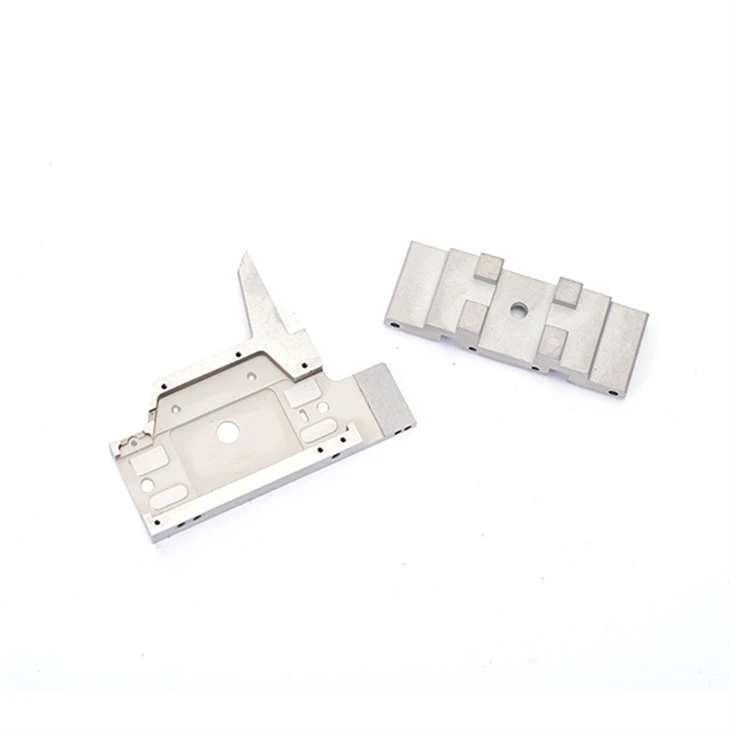
What bathroom mounting plates and supports do behind the visible fitting
This catalog reference is for component review rather than a finished bathroom fixture.
Wall attachment, hole position and concealed-face interfaces
Define wall or fixture attachment, hole positions and the load-bearing contact surfaces.
Note which faces are visible and which are concealed after installation.
Why define concealed mounting faces carefully?
The visible fitting may conceal the surfaces that actually determine its position.
A small change at a concealed seat can alter the assembled gap or alignment.
The drawing should prioritize the interfaces that position the hardware, then define the separate appearance requirements.
Machining versus near-net forming for plates and recesses
Compare machining and near-net forming for the plate, recess and mounting geometry.
Flat mounting faces and threads may require secondary operations to meet the assembly drawing.
Compare manufacturing capabilities →Bathroom hardware grade, moisture and corrosion requirements
Specify the required grade or performance criteria together with cleaning, wear and appearance requirements.
For any surface that contacts food or beverage, identify the applicable customer documentation and acceptance criteria.
For contact surfaces, specify the stainless grade and finish.
Review material-selection information →How the mounting plate closes the gap to the visible fitting
A concealed plate never appears in a finished installation, so it is usually the last part to be toleranced and the first to be blamed. In the chain from wall to visible trim it carries four links, and only one of them can absorb error without something showing.
| Link in the assembly chain | What it adds to the stack | Where to take it out of the chain |
|---|---|---|
| Plate flatness against the wall face | A plate that is not flat is pulled flat by the fasteners, and that pull does not disappear. It travels into the fixture body as preload, so the sealing face is no longer the shape it was measured at. | Hold flatness on the plate after forming, not on the fixture. If the plate is only checked in the free state, nothing in the chain records what the assembly looked like once it was tightened. |
| Hole pattern position | Holes toleranced from the plate outline inherit every variation of that outline. Two plates from the same batch can have their hole group shifted together and still pass, while the fixture mounts off-centre. | Tolerance the hole group from its own datum, not from an edge. This is the single change that most often removes a whole link from the chain without touching any manufacturing process. |
| Boss height between plate and fixture | Standoff height is the sum of plate thickness, formed boss and washer. Three parts each inside their own band can still add up to a gap that no one specified. | Treat the standoff as one assembly dimension with a named contributor, and state which of the three is allowed to move. Left implicit, the last part in the stack absorbs it, which is usually the washer. |
| Plate thickness against screw engagement | Thread engagement is not visible after assembly and is rarely measured. A plate at the low end of its thickness band loses engagement without failing any drawing dimension. | Specify a minimum engagement length rather than a nominal thickness. That converts an invisible risk into a number the supplier can hold and the inspector can check. |
| Plate edge against trim outline | The visible gap is produced by two outlines, so its variation is the sum of both. Neither part is out of tolerance when the gap is unacceptable. | Put the visible gap on the drawing as its own requirement, referenced from the same datum the trim uses. Two independent profile tolerances cannot control a gap that both parts create. |
The assembly designer sets the tolerance allocation. Mark the controlling dimensions on the component drawing.
The habit worth building for concealed parts is to ask which link is meant to absorb the accumulation before the parts are made. In most bathroom assemblies the honest answer is the fastener clearance, and letting anything else absorb it is where complaints start.
Attachment fit, seating and final-finish checks
Check attachment fit, seating, edge condition and final finish.
Specify cleaning agents, moisture exposure and the required corrosion evaluation for the project.
Quality documentation →What to include in your enquiry
- Drawing and mating dimensions.Define wall or fixture attachment, hole positions and the load-bearing contact surfaces. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Check attachment fit, seating, edge condition and final finish. Specify the mating part or inspection fixture.
Common questions
Can the surface finish be selected only for appearance?
No. The cleaning environment, underlying material and mounting interfaces should also be considered when choosing the finish.
Why define concealed mounting faces carefully?
The visible fitting may conceal the surfaces that actually determine its position. A small change at a concealed seat can alter the assembled gap or alignment. The drawing should prioritize the interfaces that position the hardware, then define the separate appearance requirements.
How should fit and operating behavior be approved?
Check attachment fit, seating, edge condition and final finish. Specify cleaning agents, moisture exposure and the required corrosion evaluation for the project.