
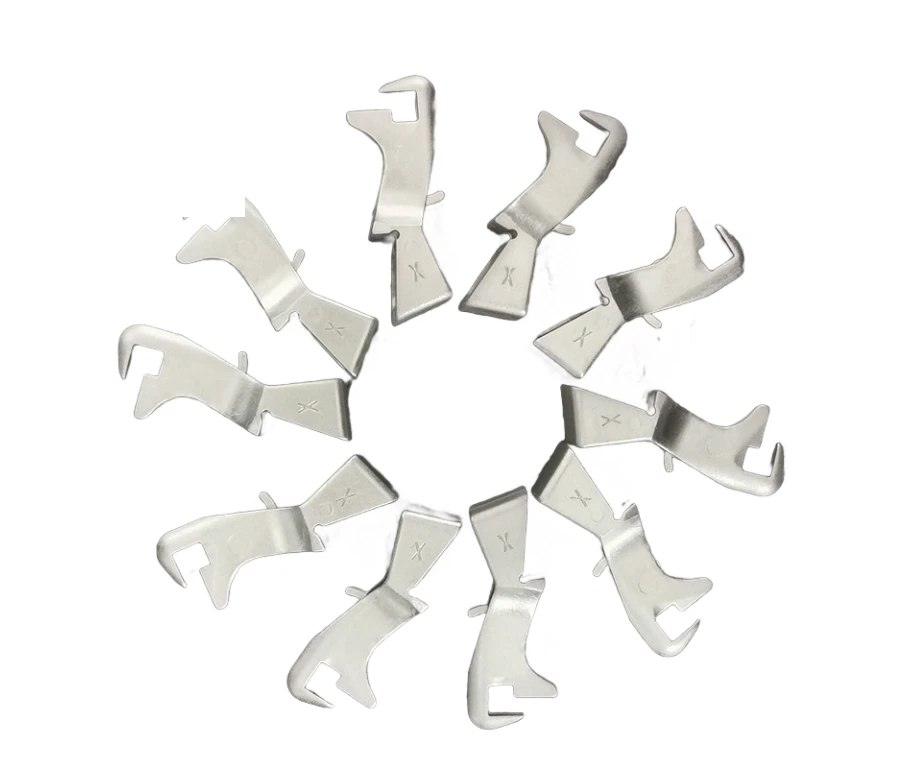
What forked sewing-machine parts do in a compact mechanism
The group shows several profiles, not interchangeable versions of one specification.
Mating pin, movement range and contact-direction interfaces
Define the mating pin or lever, movement range and contact direction.
Hole location and fork geometry should be related to the surfaces that position the part in the machine.
Why check a fork throughout its movement?
A fork can fit its pin at one position and still interfere with neighboring parts elsewhere in the cycle.
The useful acceptance condition is the required movement envelope, not only a static gap measurement.
The mating assembly identifies where that envelope must be checked.
Forming versus machining for fork openings and section changes
Compare formed production and machining with attention to fork openings and changes in section.
Critical pin fits and contact surfaces can require finishing after the body is formed.
Compare manufacturing capabilities →Forked linkages: forming, casting or machining
A fork has two features that rarely come from the same process cheaply: an opening that must stay parallel through its travel, and an arm that has to be stiff enough not to deflect under the load. The comparison turns on which of the two the drawing actually controls.
| Alternative process | When it wins on this part | What puts sintering back in front |
|---|---|---|
| Stamping and bending | Wins on the thin fork where the opening can be blanked and the arm bent. Tooling is cheap and the per-piece cost at volume is low. | Bending leaves the two prongs at slightly different heights unless they are coined afterwards. Where the prongs must stay coplanar, that coining is a per-piece operation with a per-piece setup. |
| CNC machining | Wins on the low-volume fork and on any variant where the pin hole and the fork opening have to be referenced from one setup. | A fork is mostly air. Milling removes a large fraction of the stock as chips, and that time does not fall with quantity, so the route never becomes the supply answer. |
| Investment casting | Wins on the mid-volume fork body that is too intricate for a press tool and too small for a sand casting. | As-cast surface on a sliding opening means either machining the opening or accepting the cast tolerance. Machining it puts the parallelism back into a setup, which is what forming was meant to avoid. |
| Zinc die casting | Wins on the lever that carries no significant load and needs no wear resistance, where the shape is complex and the volume is high. | A cast fork is not hard enough at the prong faces. Where the prongs are the working surfaces, a hardened part is needed and the casting only supplies the arm. |
| Sintering | Wins where the fork opening, the pin hole and the arm are one body, so the prong faces can be hardened in the same cycle as forming and the two prongs come out coplanar by construction. | It loses where the part is a flat plate with a slot. There, blanking is cheaper and needs no sizing after the furnace. |
We can compare these routes once we know the alloy, tolerances and order quantity.
The dimension that matters on a fork is not the opening width. It is the symmetry between the pin hole axis and the fork opening, because that is what determines whether the part binds at the end of its stroke. State it as a datum relationship, not as two independent dimensions.
Grade, wear and cleaning requirements for sewing-machine parts
Specify the required grade or performance criteria together with cleaning, wear and appearance requirements.
For any surface that contacts food or beverage, identify the applicable customer documentation and acceptance criteria.
For contact surfaces, specify the stainless grade and finish.
Review material-selection information →Pin fit, fork spacing and travel-interference checks
Check pin fit, fork spacing, contact edges and interference through the required travel.
Run the agreed mechanism test with the actual mating components.
Quality documentation →What to include in your enquiry
- Drawing and mating dimensions.Define the mating pin or lever, movement range and contact direction. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Check pin fit, fork spacing, contact edges and interference through the required travel. Specify the mating part or inspection fixture.
Common questions
Are the pictured parts interchangeable between sewing machines?
No. Each profile needs its own drawing and assembly reference, including movement and connection requirements.
Why check a fork throughout its movement?
A fork can fit its pin at one position and still interfere with neighboring parts elsewhere in the cycle. The useful acceptance condition is the required movement envelope, not only a static gap measurement. The mating assembly identifies where that envelope must be checked.
How should fit and operating behavior be approved?
Check pin fit, fork spacing, contact edges and interference through the required travel. Run the agreed mechanism test with the actual mating components.