
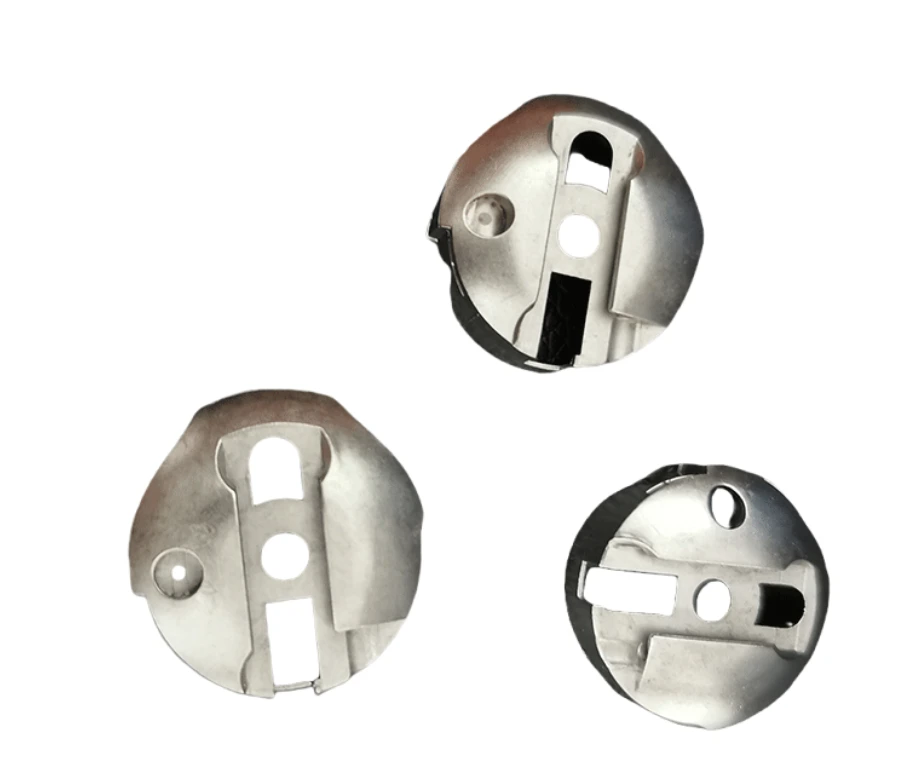
What sewing-machine covers and guides do around moving elements
The catalog contains several related shapes.
Clearance slots versus locating features
Mark clearance slots separately from features that locate the part.
Thin curved sections and openings need to be assessed in the assembled condition.
Why distinguish a clearance opening from a guide slot?
A clearance opening prevents interference; a guide slot helps control movement.
Their size, edge and position requirements therefore serve different purposes.
Identifying the role of each opening prevents unnecessary precision on free space while overlooking a working interface.
Forming versus machining for curved profiles and slots
Compare forming and machining for the curved profile and slots.
The chosen route must preserve mounting geometry while meeting edge and finish requirements around openings.
Compare manufacturing capabilities →Covers and guide plates: which route holds the slot
Nearly every argument about a cover plate is actually about one slot. If the slot is clearance, almost any process can make it. If the slot guides something, its side faces are functional, and that changes both the route and the tolerance band by a wide margin.
| Alternative process | When it wins on this part | What puts sintering back in front |
|---|---|---|
| Progressive die stamping | Wins on the thin cover where the slot is a clearance opening. Blank, pierce and form in one strip at the lowest per-piece cost available. | A pierced slot carries a shear taper and a burr on one side. Where the slot side faces guide a moving part, that taper is a functional error, and deburring does not restore the side face. |
| Laser cutting plus bending | Wins at low volume and wherever the slot pattern is still being revised, since a change needs a new program and not a new tool. | The cut edge is perpendicular but carries a heat-affected zone and a small taper of its own. On a guide slot that has to run against a pin, the edge condition becomes a wear question. |
| CNC milling | Wins where the slot side faces have to be square to the plate and parallel to each other within a narrow band. | Milling a thin plate distorts it unless the stock is supported, and the support is a fixture per geometry. The setup cost repeats for every variant, which is where the low-volume advantage goes. |
| Die casting | Wins on the thicker cover or the frame that surrounds the mechanism, where the section is heavy and the tolerance is moderate. | Draft has to be built into the slot if the slot is cast. A drafted slot cannot guide anything, so the slot is either cut afterwards or the casting is not the right route for that feature. |
| Sintering | Wins where the slot and a locating boss have to coexist on a part with a change of thickness, because a formed slot has no shear taper and no burr to remove on either side. | It loses on the plain flat cover. There, blanking is cheaper, faster and does not need a sizing step after the furnace. |
We can compare these routes once we know the alloy, tolerances and order quantity.
Split the drawing before comparing prices: clearance slots as one class, guide slots as another. Merging them into a single tolerance is the most common reason a quotation comes back wrong, and the reason the first samples get rejected for something nobody intended to specify.
Cover and guide grade, edge and finish requirements
Specify the required grade or performance criteria together with cleaning, wear and appearance requirements.
For any surface that contacts food or beverage, identify the applicable customer documentation and acceptance criteria.
For contact surfaces, specify the stainless grade and finish.
Review material-selection information →Opening position, seating and moving-part interference checks
Check opening positions, seating and interference with moving parts.
Inspect accessible edges and any surface that contacts thread or another sensitive component.
Quality documentation →What to include in your enquiry
- Drawing and mating dimensions.Mark clearance slots separately from features that locate the part. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Check opening positions, seating and interference with moving parts. Specify the mating part or inspection fixture.
Common questions
Should every slot have the same tolerance?
No. Identify whether each opening locates, guides or simply clears another part; those functions call for different controls.
Why distinguish a clearance opening from a guide slot?
A clearance opening prevents interference; a guide slot helps control movement. Their size, edge and position requirements therefore serve different purposes. Identifying the role of each opening prevents unnecessary precision on free space while overlooking a working interface.
How should fit and operating behavior be approved?
Check opening positions, seating and interference with moving parts. Inspect accessible edges and any surface that contacts thread or another sensitive component.