
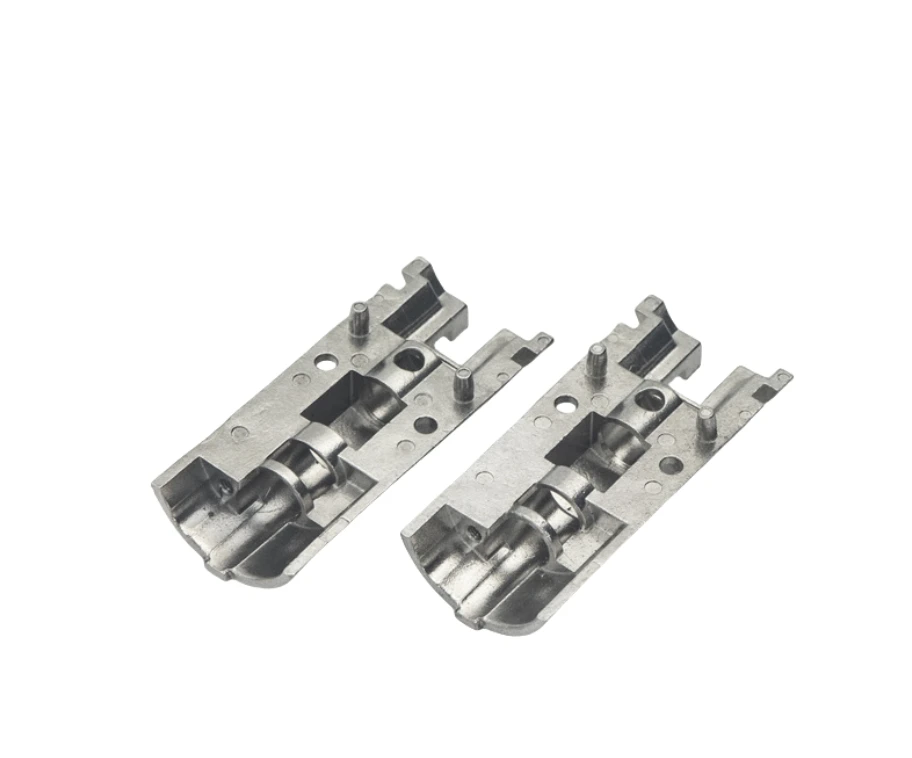
What custom lock body hardware integrates in one component
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
Each drawing should identify its role within the complete lock assembly.
Mounting scheme, supported members and contact-surface interfaces
Specify the mounting scheme, supported members and any working contact surfaces.
Mark features that establish position separately from clearance pockets.
Why include installation clearance for lock body hardware?
The component must permit assembly as well as operation.
A cavity or opening that fits an installed member may still need a defined installation path.
Including the neighboring parts helps identify the clearances and edges relevant to both stages.
Forming versus machining for cavities and datums
Compare forming of integrated geometry with machining where the cavity or datum requirements favor it.
Include necessary deburring and finishing access.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Lock body hardware material, treated-surface and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
The component specification does not establish a security rating for the complete lock.
Review material-selection information →Mounting, cavity and final-fit checks
Check mounting and cavity relationships, edges and final fit.
Use the intended lock assembly to confirm that neighboring parts can be installed and operated.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →What makes a lock body housing expensive at low volume
A lock body is a large, heavy part with cavities and mounting features. Its cost profile is the opposite of a small MIM component: material and press time matter from the first part, and tooling is spread over a much larger mass.
| Cost element | Why a small order costs more per piece | Why a large order stops getting cheaper |
|---|---|---|
| Press tonnage and projected area | The press is chosen by projected area. A large face needs a large press, and that press runs one part per stroke rather than a multi-cavity load. | Press time is proportional to strokes, so volume does not shorten it. More capacity means another press, not a cheaper part. |
| Powder consumption | A heavy part consumes material in proportion to its mass, and on this class of part material is a substantial share of the first quotation. | Material follows the metal market and the mass of the part. Design, not order size, is what reduces it. |
| Furnace load by weight and height | A lock body takes vertical space in the furnace. Fewer parts fit per load than with small components, so the cycle cost is spread over less pieces. | The load is limited by the chamber, and the chamber is already full. Extra volume buys cycles, not efficiency. |
| Machining of cavities, threads and seats | A formed cavity is close to final, but threads and seating faces are cut. Each cut face is a set-up and a per-piece time. | Multi-part fixtures and combined tools cut the time per part. They do not remove operations, and each feature still has to be cut on every part. |
| Coating or plating by surface area | Finishing is priced on exposed area. A body has a lot of it, and rack or jig space is used up quickly. | Surface treatment is close to linear with area. It is one of the few lines where the cost per part is predictable and does not improve with scale. |
Note. The split below describes cost structure, not prices. What a specific part costs depends on its geometry, material, finish and the quantity you can commit; this page explains which of those you can move and which you cannot.
On a body this size the first three lines dominate, and none of them improve much with quantity. The lever that works here is geometry: a smaller projected area, a cavity that needs no secondary cut, a seat that can be formed instead of milled. Those are drawing decisions, and they are available before the first order rather than after the tenth.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Can the same lock body hardware serve several lock designs?
Only after their mounting, clearance and operating interfaces are confirmed; an identical-looking cavity is not sufficient.
Why include installation clearance for lock body hardware?
The component must permit assembly as well as operation. A cavity or opening that fits an installed member may still need a defined installation path. Including the neighboring parts helps identify the clearances and edges relevant to both stages.
How should the completed mechanism be checked?
Check mounting and cavity relationships, edges and final fit. Use the intended lock assembly to confirm that neighboring parts can be installed and operated.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →