
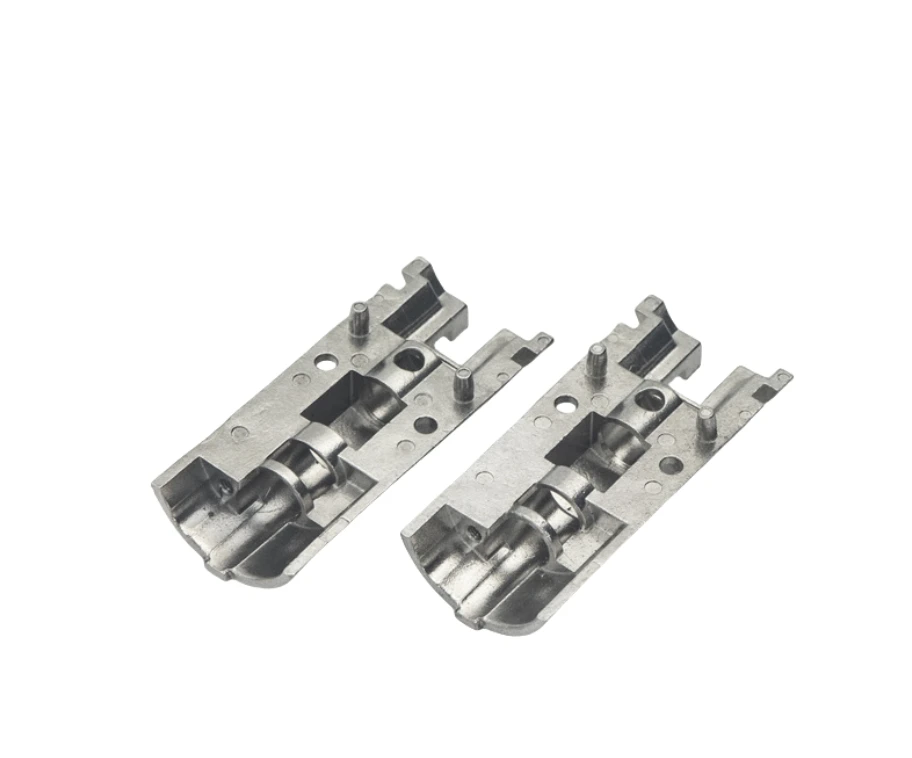
What guide and support parts align inside a smart lock
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
Their dimensional relationships remain important even when actuation is electronically controlled.
Guide paths, lock-body attachment and moving-member contacts
Define the guide paths, attachment to the lock body and contact with the moving members.
Mark which surfaces locate the component during assembly.
Why define mechanical clearances before control-system testing?
The guide and support geometry provide the physical conditions for movement.
Their requirements should be inspectable without relying on electronic behavior to explain a mismatch.
System testing can then evaluate the completed mechanism against an already defined mechanical arrangement.
Integrated forming versus machining of guide features
Compare integrated forming with machining of critical guide and locating features.
The final route should establish the datums used for inspection.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Smart-lock internals: when sintering is the wrong answer
Electronic actuation changed the tolerances that matter. A guide that only had to slide now also has to let a sensor confirm position, so clearance and repeatability matter more than strength. That reorders the process comparison entirely.
| Alternative process | When it wins on this part | What puts sintering back in front |
|---|---|---|
| Zinc die casting | Wins on the lock-body frame and the larger guide seat, where the wall is heavy and the tool life is long. | A cast guide face carries the dimensional scatter of porosity and shrinkage. Where the face is a sliding datum, that scatter becomes clearance variation between units, which is what the electronics then have to tolerate. |
| CNC machining | Wins where two guide paths have to stay parallel within a band that only one setup can hold. | Sintered parts come out of the furnace with some flatness loss and are corrected by sizing. The sizing tool is worth its cost only when the volume is there; below that, milling the two faces in one setup is the cheaper way to the same result. |
| Plastic moulding with a metal insert | Wins on guides that carry no load and need no wear resistance. It is lighter, cheaper and needs no finishing. | A flame requirement, a wear requirement or a temperature requirement removes plastic from the comparison. So does any need for the guide to hold a thread. |
| Sheet metal brackets | Wins on the mounting plate and the support tabs, which are flat, thin and mostly clearance. | Bent sheet gives one thickness and a soft edge. Where the part must present a hardened slide face, or where the edge itself is the guide, bending does not get there. |
| Sintering | Wins where a guide channel, a limit step and a mounting ear are one part in a wear-resistant alloy, and hardening is part of the same cycle rather than a second trip. | It loses when the part is a flat bracket with two holes. There, bending is cheaper and no one has to argue about sizing. |
Note. This table is a screening aid, not a recommendation against our own process. Where a row above describes your part better than the sintering route does, we will say so and quote against the route that actually fits; the quantities, alloy and tolerances on your drawing still decide the answer.
One commercial reality shapes this comparison more than any tolerance: the electronics iterate faster than the mechanism. That means these parts often run in small batches across several revisions, and tooling amortisation matters more than the quoted piece price. Ask for the amortisation to be shown separately.
Guide part material, treated-surface and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
The component specification does not establish a security rating for the complete lock.
Review material-selection information →Guide alignment, attachment and operating-clearance checks
Inspect guide alignment, attachment and operating clearance after finishing.
Verify motion using the intended actuator and lock mechanism.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Do electronic controls compensate for an incorrectly fitted guide?
Do not assume so. The mechanical fits and movement need to meet their own drawing and test requirements.
Why define mechanical clearances before control-system testing?
The guide and support geometry provide the physical conditions for movement. Their requirements should be inspectable without relying on electronic behavior to explain a mismatch. System testing can then evaluate the completed mechanism against an already defined mechanical arrangement.
How should the completed mechanism be checked?
Inspect guide alignment, attachment and operating clearance after finishing. Verify motion using the intended actuator and lock mechanism.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →