
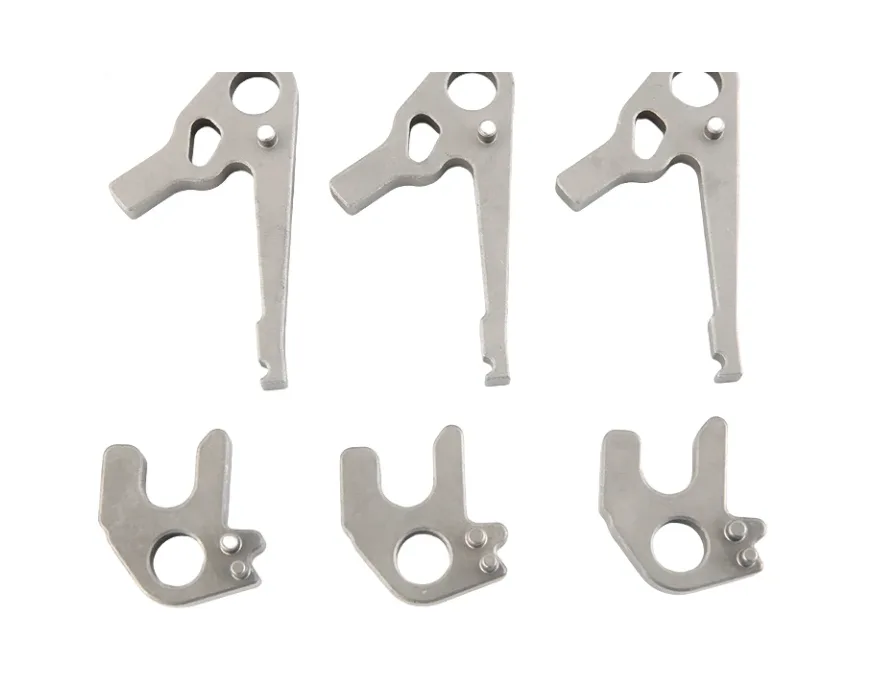
What smart lock forks and links transmit from the actuator
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
The reference includes different open-ended profiles and connection features.
Actuator, mating pin and driven-member interfaces
Identify the actuator, mating pin and driven member for each part.
Define fork spacing, pivot positions and the limits of motion.
Why check open-ended links through the full stroke?
An open profile can clear a mating member in one position but contact it elsewhere.
Reviewing the full stroke identifies the functional clearances and stops.
This provides a better basis for acceptance than a single static fit comparison.
MIM versus machining for fork and link contacts
Compare MIM or other forming with machining of critical holes and contacts.
Open ends and changes in section require a part-specific tooling review.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Fork and link material, treated-surface and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
The component specification does not establish a security rating for the complete lock.
Review material-selection information →Pin fit, fork spacing and full-stroke interference checks
Check pin fit, fork spacing and interference over the complete movement.
Include the final finish and any required operating cycles in approval.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →The five features on small lock parts that decide the tool
On a part this small, the unit price is set by the tool long before it is set by the metal. Every feature below either adds a slide, adds a cavity, or adds a secondary operation, and those three are what a quotation is actually made of.
| What we flag | Why it bites on this part | How the drawing usually changes |
|---|---|---|
| Walls under 0.8 mm | Feedstock will not fill a long thin section reliably at production rate. The first samples look fine and the yield problem appears at month three. | Thin walls are either thickened locally or the part is split so the thin detail becomes a machined or stamped insert. |
| Locating pins and posts | A slender post in a sintered part bends in the ejector and leans in the furnace, and there is no straightening step that fixes it cheaply. | Posts get a draft and a root fillet, or they become a hole with a pressed pin, which is also easier to replace in service. |
| The face that seats a sensor | A flatness call on a sintered face is achievable, but only if the face is a single plane that the tool can press squarely. A face split by a step will not hold it. | The seating face is isolated as one plane, and if it must be truly flat it is given a facing allowance instead of a flatness call. |
| Number of cavities | Small parts are priced by cavity count, and cavity count is set by annual volume. A 16-cavity tool on a 20,000 piece a year part is a tool nobody can amortise. | The cavity count is quoted against the stated annual volume, and the drawing does not need to change at all. This one is a conversation, not a revision. |
| Magnets, sensors and inserts | MIM cannot co-sinter a dissimilar material. A pocket drawn for a magnet is a pocket that has to be pressed to size and glued or staked. | The pocket is dimensioned as a press fit with a retention feature, and the insert is listed as buyer-supplied or supplier-supplied explicitly. |
Note. These are the changes we most often ask for on this class of part, not a review of any particular drawing. They describe how the process behaves; dimensions, tolerances and acceptance values come from the project drawing.
What we do not do is quote a 16-cavity tool and let the buyer discover the amortisation later. If the volume does not support the cavity count, we say so and quote fewer cavities at a higher unit price, because that is the number that is actually true.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Can the same fork shape serve different actuators?
Only if the connection, load and travel requirements match; the actuator and mating mechanism must be specified.
Why check open-ended links through the full stroke?
An open profile can clear a mating member in one position but contact it elsewhere. Reviewing the full stroke identifies the functional clearances and stops. This provides a better basis for acceptance than a single static fit comparison.
How should the completed mechanism be checked?
Check pin fit, fork spacing and interference over the complete movement. Include the final finish and any required operating cycles in approval.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →