
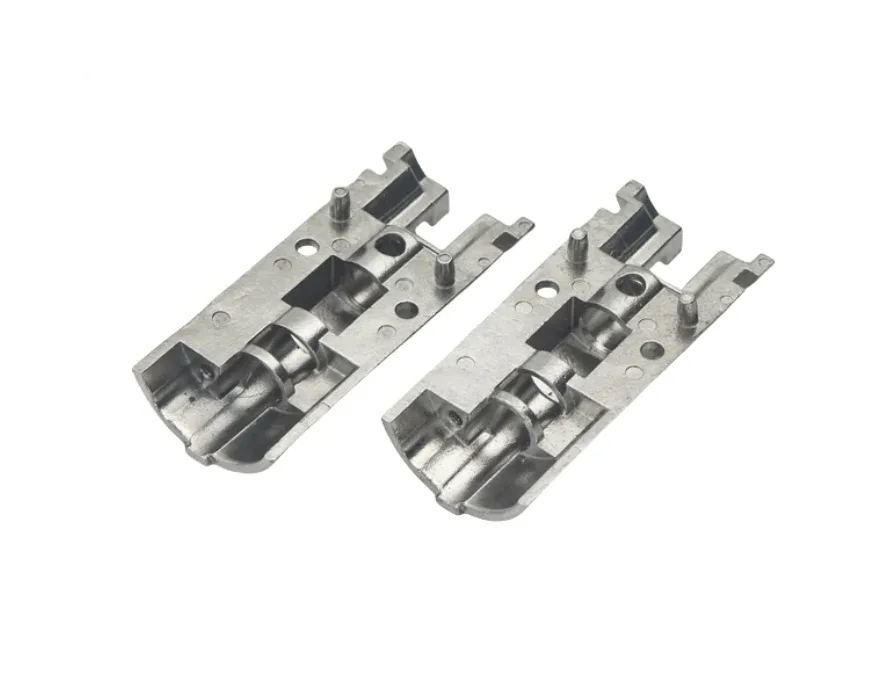
What support plates position within a lock body
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
The reference shows elongated components with cavities and mounting or guide features.
Supporting faces, locating holes and moving-member clearances
Identify the supporting faces, locating holes and clearances around the moving members.
Keep guide relationships consistent with the lock's assembly datums.
Why review cavities and guides with the moving members?
A cavity may provide clearance or position another part, while a guide controls movement.
The mating members reveal which surfaces are functional.
Reviewing them together avoids assuming that every recess is simply noncritical empty space.
MIM versus machining for integrated support geometry
Compare MIM and machining for integrated support geometry.
Recesses and working seats need review for tooling, finishing and inspection access.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Support plate material, treated-surface and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
The component specification does not establish a security rating for the complete lock.
Review material-selection information →Mounting fit, guide alignment and travel-interference checks
Check mounting fit, guide alignment and interference through the mechanism's travel.
Inspect edges around moving or assembled parts.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Where the cost goes on a thin support plate
A support plate looks cheap to make and is not, because most of its cost sits in operations that cannot be batched: keeping it flat, keeping the edges clean, and keeping it flat again after coating.
| Cost element | Why a small order costs more per piece | Why a large order stops getting cheaper |
|---|---|---|
| The forming tool | A thin plate needs a tool with a flat, well-supported face. The tool itself is not the expensive part; getting flatness out of a thin section is what drives the design. | Tooling is amortised quickly on a plate. What returns later is rework of the tool when flatness drifts, which is a maintenance cost rather than a volume cost. |
| Flatness correction | Sintered thin sections distort, and the correction is done part by part on a press or by hand. This is the line that makes a small order expensive. | Automated handling helps, but a plate that needs correction still needs it on every part. The better answer is a design change that removes the correction, and that is a one-off engineering decision. |
| Deburring of thin edges | Thin edges deform under bulk deburring, so the operation is often done with more care and less speed than on a solid part. | Barrel finishing scales, but thin parts limit the media and the time. The process window is narrow, so volume does not buy much speed. |
| Plating and rack handling | Thin plates need support on the rack to avoid distortion, which reduces how many fit per rack. | Rack loading is limited by the part, not the tank. Adding volume adds racks and handling, not efficiency. |
| Flatness inspection in the free state | Flatness has to be checked with the part unrestrained, which is slower than a go gauge and hard to automate. | Sampling can be agreed, but the check itself does not get faster. This stays a per-lot time cost. |
Note. The split below describes cost structure, not prices. What a specific part costs depends on its geometry, material, finish and the quantity you can commit; this page explains which of those you can move and which you cannot.
For a plate, the cheapest change is usually a small increase in thickness or a stiffening feature that removes the need for correction. That decision costs nothing in tooling terms and removes the largest single line. Discounting a thin plate is harder than designing a stiffer one.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Can a support plate be approved using flatness alone?
No. Hole, cavity and guide relationships also determine whether the mechanism operates correctly.
Why review cavities and guides with the moving members?
A cavity may provide clearance or position another part, while a guide controls movement. The mating members reveal which surfaces are functional. Reviewing them together avoids assuming that every recess is simply noncritical empty space.
How should the completed mechanism be checked?
Check mounting fit, guide alignment and interference through the mechanism's travel. Inspect edges around moving or assembled parts.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →