
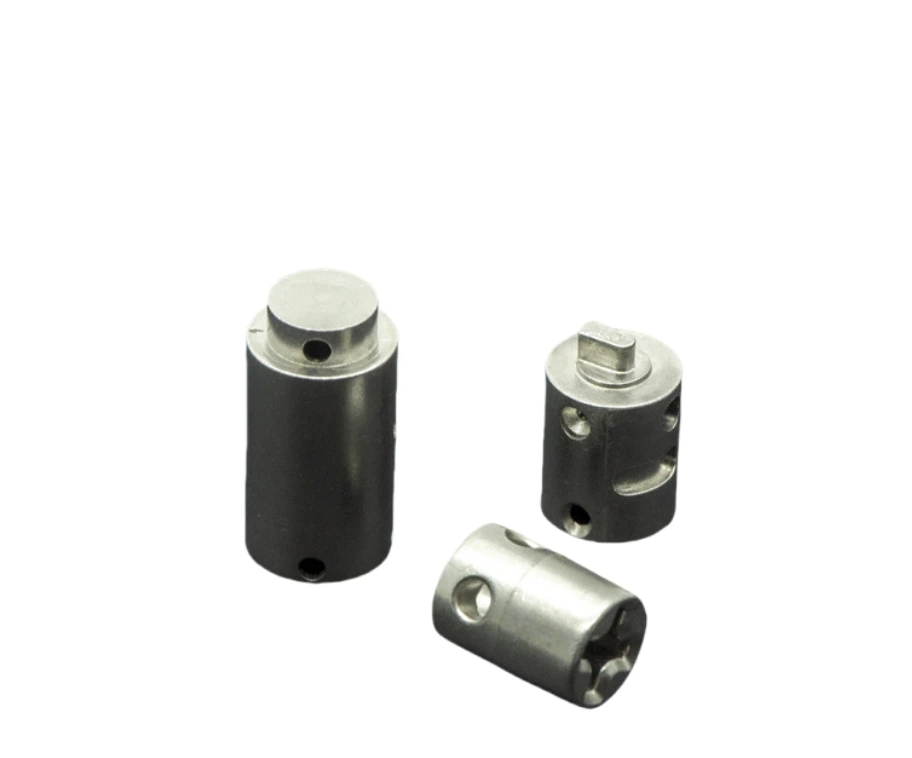
What cylindrical lock components combine in one body
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
Their function depends on how the cylinder is retained and actuated in the lock.
Locating diameter, end features and opening-position interfaces
Specify the locating diameter, end features and position of any openings.
Clarify whether each opening retains, connects or simply clears another part.
Why identify the function of each cylinder opening?
An opening may guide, retain, connect or clear another component.
These roles determine which size and position relationships matter.
Defining the role makes it possible to apply controls to the working interface rather than to all openings indiscriminately.
Turning versus MIM for cylindrical lock bases
Compare turning for the cylindrical base with MIM or secondary machining for integrated detail.
Final bore or outside-fit requirements should be reviewed after finishing.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Cylindrical lock body material, treated-surface and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
The component specification does not establish a security rating for the complete lock.
Review material-selection information →Locating fit, opening position and end-engagement checks
Inspect locating fit, opening positions and end engagement.
Check the intended lock action with the mating body and actuator.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →What drives cost on a cylindrical lock body
A cylinder is formed close to size and then turned. Turning is quick per part but it is still a per-part operation, and the locating diameter that the lock depends on is usually the reason it exists.
| Cost element | Why a small order costs more per piece | Why a large order stops getting cheaper |
|---|---|---|
| The forming tool and its wear parts | Cylindrical parts need a tool with a well-controlled bore and a clean ejection path. Ejector and core wear show up as a change in roundness before anything measures out of tolerance. | Tooling is amortised early. Wear parts are a running cost that volume makes more frequent, not less. |
| Turning of the locating diameter and ends | The diameter that locates the cylinder in the lock is turned, and so are the ends. Each is a set-up plus a per-piece time. | Automatic turning makes the per-piece time small but not zero. The number of turned features is fixed by the drawing, so volume lowers the rate rather than the workload. |
| Furnace load and section size | A solid cylinder occupies furnace space in proportion to its size and gives no benefit from stacking. | The chamber sets the limit. Beyond a full load, more volume means more cycles. |
| Plating and handling of cylindrical parts | A cylinder rolls, which is actually helpful: barrel or rotating plating loads densely and coats evenly. | This is the one line where a cylindrical part scales well. Once the barrel is full, cost per part is close to constant and already low. |
| Diameter and end-feature inspection | Gauging a diameter is fast. Checking an opening position relative to the axis needs a fixture or a CMM, and the fixture is a one-off cost that a small order still has to carry. | The per-part check stays quick. What does not repeat is the fixture, which is why a repeat order on the same drawing is proportionally cheaper than the first. |
Note. The split below describes cost structure, not prices. What a specific part costs depends on its geometry, material, finish and the quantity you can commit; this page explains which of those you can move and which you cannot.
The cylinder is a case where plating is already efficient and turning is already fast. What a small order actually pays for is the inspection fixture and the tooling, both one-off. If the first quotation looks high, the useful question is which one-off items it contains and whether they can be reused on the next order.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Can all openings use one general position tolerance?
Their controls should follow their functions and datums; retention or drive openings may need different requirements from clearance holes.
Why identify the function of each cylinder opening?
An opening may guide, retain, connect or clear another component. These roles determine which size and position relationships matter. Defining the role makes it possible to apply controls to the working interface rather than to all openings indiscriminately.
How should the completed mechanism be checked?
Inspect locating fit, opening positions and end engagement. Check the intended lock action with the mating body and actuator.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →