
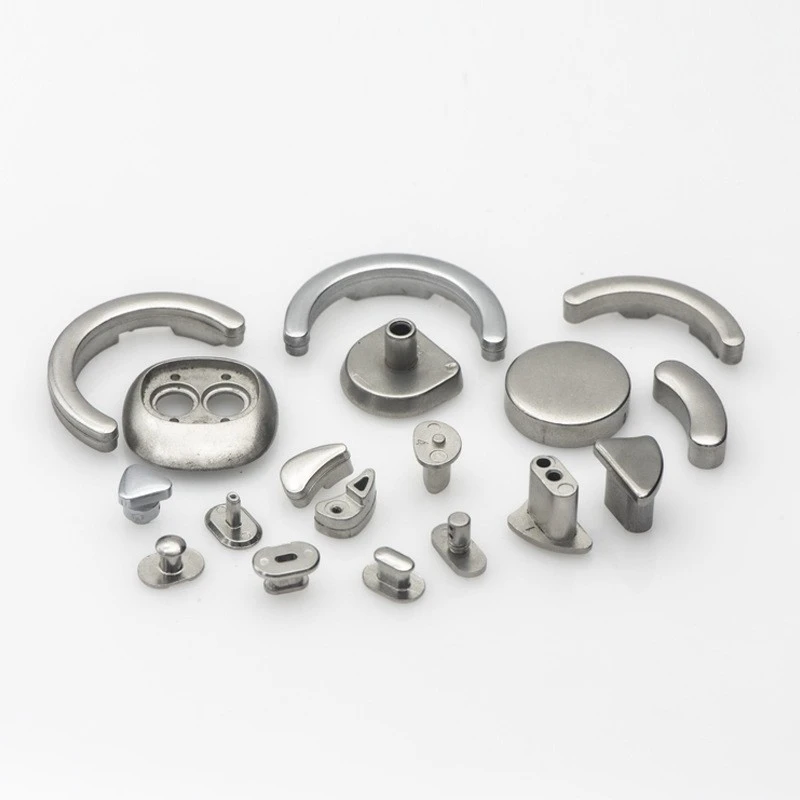
What covers, rings and hardware do around RF assemblies
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
The reference group shows mechanical forms; RF performance requirements must be supplied separately.
Mechanical-role versus electrical-function interfaces
Identify whether the part has only a mechanical role or also carries a specified electrical function.
Define enclosure interfaces, fastening and relevant contact surfaces.
Why define contact surfaces in RF hardware?
Some interfaces only locate mechanical parts, while others may have a specified electrical role.
A finish selected for appearance does not automatically define the latter.
The system requirements must identify the contacts and the acceptance evidence expected for them.
Forming and machining for rings, covers and supports
Review forming and machining for the individual ring, cover or support.
Contact faces that affect assembly or electrical connection need explicit finish requirements.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →When RF hardware should leave the sintering route
RF parts are judged on contact condition and surface state more often than on dimensional tolerance. Both of those are set by finishing and by how the part is measured, not by how it is formed. Forming only decides whether the right face can be left for the operation that follows.
| Alternative process | When it wins on this part | What puts sintering back in front |
|---|---|---|
| CNC machining (three and four axis) | Wins on waveguide flanges, cavity blocks and lids where the count of distinct features is low, the tolerance band is tight, and flatness plus surface roughness carry the function. | A sintered face will not come off the furnace at sealing roughness, so stock has to be left and milled anyway. If the entire face is being milled, forming saved material and saved no time. |
| Sheet metal and forming | Wins on shield cans and flat covers. A bent shield is lighter, cheaper and does not add mass next to a tuned circuit. | Sintering cannot produce a thin deep drawn can, and should not try. Where the cover also has to carry a connector boss, a two-piece assembly usually beats asking one process to do both jobs. |
| Aluminium die casting | Wins on the larger cavity housing where mass matters and the wall can carry draft. Aluminium gives the stiffness at a fraction of the density. | Draft and ejector marks sit inside a cavity that may need to stay parallel. Where the inner faces are functional rather than clearance, the draft becomes a machining allowance on every face. |
| Screw machining | Wins on the inner conductor and on cylindrical pins, where the part is a solid of revolution and the controlling callout is coaxiality. | Cross-drilled holes, flats for a wrench, or a shoulder that is not round break the single-setup advantage. Those are exactly the features a pressed shape gets for free. |
| Powder metallurgy pressing | Wins on plain rings, washers and flanges whose outline is two-dimensional. A pressing tool costs less and quotes faster than a feedstock line. | The moment a radial hole or an angled port appears, pressing cannot fill it. That single feature is usually what moves a part from pressing to injection. |
Note. This table is a screening aid, not a recommendation against our own process. Where a row above describes your part better than the sintering route does, we will say so and quote against the route that actually fits; the quantities, alloy and tolerances on your drawing still decide the answer.
If the drawing separates mechanical fit from electrical function, this table can be read once. If the two are mixed into one tolerance, the route cannot be chosen honestly by anyone, and the argument later will be about which requirement was actually meant.
RF hardware material, contact and finish requirements
Define base material, final condition and cosmetic finish separately.
Identify visible faces, permitted edge rounding and the dimensions that must be met after finishing.
Any magnetic, electrical or acoustic requirement needs its own specification.
Review material-selection information →Mechanical fit and final-surface checks
Inspect mechanical fit and the agreed final surface.
Any shielding, grounding or frequency-related acceptance belongs to a defined customer test.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Can RF performance be judged from the component shape?
No. Electrical behavior depends on material, contacts and the full system; it needs a separate specification and validation.
Why define contact surfaces in RF hardware?
Some interfaces only locate mechanical parts, while others may have a specified electrical role. A finish selected for appearance does not automatically define the latter. The system requirements must identify the contacts and the acceptance evidence expected for them.
How are appearance and functional fit checked?
Inspect mechanical fit and the agreed final surface. Any shielding, grounding or frequency-related acceptance belongs to a defined customer test.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →