
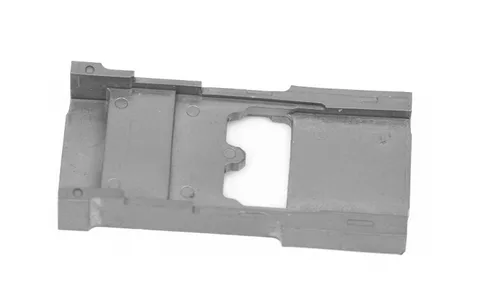
What frame inserts support inside a phone enclosure
Long edges and internal openings must align with the surrounding housing and installed components.
Attachment datums, opening positions and surrounding-space interfaces
Define the attachment datums, opening positions and available space around the insert.
Flatness and straightness may matter to assembly even if the part is not externally visible.
Why use assembly datums for an elongated insert?
The insert's working position is established by its attachment or locating features.
An unconstrained long edge can be a poor description of that position.
Assembly-based references clarify whether straightness, seating or opening alignment is the feature that actually controls fit.
Machining, stamping and near-net forming for thin sections
Compare machining, stamping or near-net forming for the section and quantity.
Thin elongated sections need a route that preserves their finished mounting relationship.
Compare manufacturing capabilities →Frame insert material and finish requirements
Define base material, final condition and cosmetic finish separately.
Identify visible faces, permitted edge rounding and the dimensions that must be met after finishing.
Any magnetic, electrical or acoustic requirement needs its own specification.
Review material-selection information →Seating, window position and assembly-interference checks
Inspect seating, hole or window position and any interference during enclosure assembly.
Specify visible edges and finish only where they are actually exposed.
Quality documentation →Where the cost sits on a thin frame insert
A frame insert is a flat part with openings, bought in phone quantities and judged on how flat it stays. Its cost profile is dominated by flatness and by the process chosen for a thin section.
| Cost element | Why a small order costs more per piece | Why a large order stops getting cheaper |
|---|---|---|
| The tool and its flatness control | A long thin part needs a tool that keeps the whole length supported. Tool cost is moderate, and flatness is designed into it rather than corrected afterwards. | Tooling is one-off. Tool maintenance returns with stroke count, so a long programme pays for re-polishing the face more than once. |
| Process choice for a thin section | Stamping or etching can be cheaper than forming for a uniform thin part, and both avoid the distortion that sintering introduces. Forming wins where there are bosses or local thickness changes. | If stamping is viable, its cost per part falls faster with volume than forming does. The process decision sets the slope of the whole cost curve. |
| Flattening or coining | Formed thin parts need flattening, which is per part. A stamped part often does not, which is one reason the two routes diverge. | Flattening can be automated but not eliminated without a design change. On a stamped blank the operation does not exist at all. |
| Finishing on a large flat area | Coating, anodising or brushing are priced on area, and a frame insert has a lot of it for very little mass. | Area does not scale down. This is a linear line at any quantity. |
| Flatness and window-position checks | Both need a fixture or a CMM programme, and both are per lot rather than per part. | The fixture is one-off, the checks are fast. This is the line that makes a second order cheaper than the first. |
For a price comparison, use the same material, finish, order quantity and inspection requirements.
The question worth asking on a frame insert is whether the wall is uniform. If it is, the honest comparison is against stamping or etching, and that comparison will often win. Forming earns the order when the insert carries local thickness changes that a stamped blank cannot produce.
What to include in your enquiry
- Drawing and mating dimensions.Define the attachment datums, opening positions and available space around the insert. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Inspect seating, hole or window position and any interference during enclosure assembly. Specify the mating part or inspection fixture.
Common questions
Should a frame insert be dimensioned from its outermost edge?
Use the assembly datums that locate it; a cosmetic or clearance edge may not be a suitable primary datum.
Why use assembly datums for an elongated insert?
The insert's working position is established by its attachment or locating features. An unconstrained long edge can be a poor description of that position. Assembly-based references clarify whether straightness, seating or opening alignment is the feature that actually controls fit.
How are appearance and functional fit checked?
Inspect seating, hole or window position and any interference during enclosure assembly. Specify visible edges and finish only where they are actually exposed.