
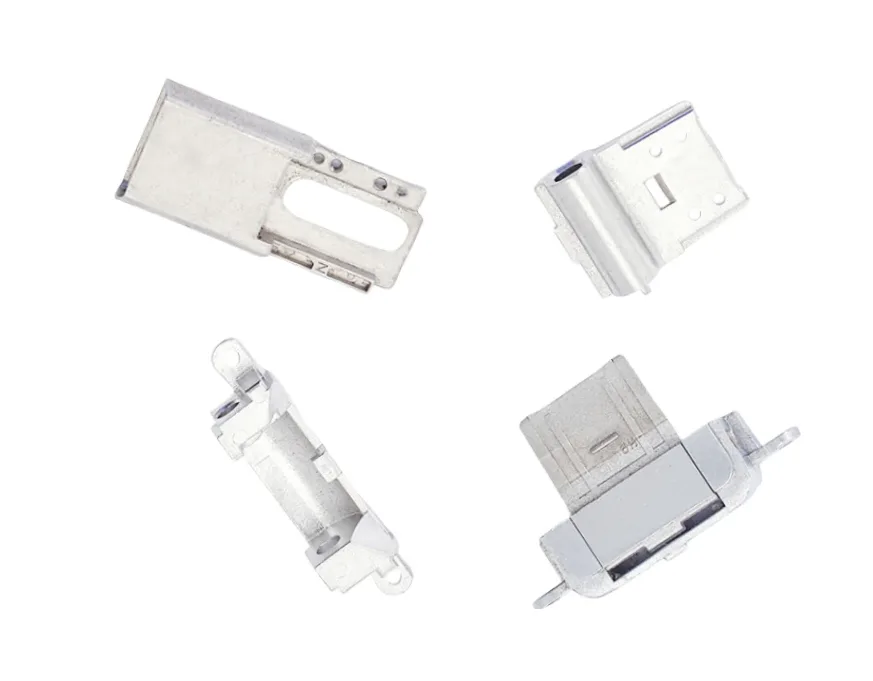
What phone camera housings position and enclose
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
The reference group illustrates small housing and support forms, not a complete camera module.
Module locating surfaces, opening positions and frame attachment
Define optical or module locating surfaces, opening positions and attachment to the phone frame.
Keep cosmetic surfaces separate from the alignment datums.
Why distinguish a cosmetic opening from a locating aperture?
An exterior opening may provide visibility or clearance, while another surface locates the module.
Their acceptable positions need not be the same.
The module drawing identifies the critical interface and avoids using appearance alone to judge the mounting geometry.
MIM versus machining for camera housing geometry
Compare MIM and machining for the enclosure geometry and small attachment features.
Openings that control alignment may need final machining and inspection access.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Camera housing base material and cosmetic-finish requirements
Define base material, final condition and cosmetic finish separately.
Identify visible faces, permitted edge rounding and the dimensions that must be met after finishing.
Any magnetic, electrical or acoustic requirement needs its own specification.
Review material-selection information →Aperture position, module clearance and mounting-fit checks
Check aperture position, module clearance and mounting fit.
The metal housing does not itself establish image quality or sealing performance.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →What shifts between lots on a camera housing
The housing does two jobs at once: it locates the module, and it is seen. The locating surfaces are small, the visible area is large, and the two are affected by different parts of the process.
| What drifts between lots | Where the drift comes from | What the release check catches |
|---|---|---|
| Module locating surface position and flatness | The locating surface is often machined after sintering to hold its position against the frame datum. Flatness depends on how the thin wall was supported during the cut, and thin walls move. | Check the locating surface against the frame datum on an assembled sample, and check flatness in the free state. A surface that is flat while clamped is not flat in the phone. |
| Aperture position relative to the module seat | The aperture is formed by a core, and where it is finished the finishing follows the sintered blank. Blank variation therefore moves the aperture relative to the seat rather than on its own. | Check the aperture from the module seat, not from the outer edge. Optical clearance is set by that relationship, and an outer-edge dimension mixes the two. |
| Wall thickness and its effect on coating | Thin walls take coating differently from thick ones, and a coated thin wall can close an aperture that was correct before coating. | Check the aperture after coating. Where the aperture controls light or clearance, state its size in the delivered condition. |
| Surface roughness on the visible area | A sintered surface starts rough, and how much of that roughness is removed depends on the finishing sequence rather than on the mould alone. | State roughness on the visible area by value and by sample, and check it on the surface that will be seen. Roughness measured on a protected face is not evidence for the visible one. |
| Distortion across the open side | An open frame is the least rigid shape in the family. It distorts in sintering and again during machining, and the distortion shows up as a gap at the frame joint rather than as a dimensional error. | Check the frame joint gap on an assembled sample, and keep free-state flatness as an in-process check. The gap is what the customer sees and what a seal depends on. |
Note. This describes how the process behaves across a production run, not the history of any particular lot. Acceptance values, sample sizes and inspection methods come from the project drawing and the agreed quality plan.
Three of these five are set by the relationship to the module or the frame, and only that relationship can be inspected meaningfully. The other two are process outputs that need a retained sample. A drawing that gives the outline and an appearance note but no module datum leaves the two most important items unmeasurable.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Can the housing be approved without the camera module drawing?
An initial geometry review is possible, but the module envelope and locating requirements are needed to verify fit.
Why distinguish a cosmetic opening from a locating aperture?
An exterior opening may provide visibility or clearance, while another surface locates the module. Their acceptable positions need not be the same. The module drawing identifies the critical interface and avoids using appearance alone to judge the mounting geometry.
How are appearance and functional fit checked?
Check aperture position, module clearance and mounting fit. The metal housing does not itself establish image quality or sealing performance.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →