
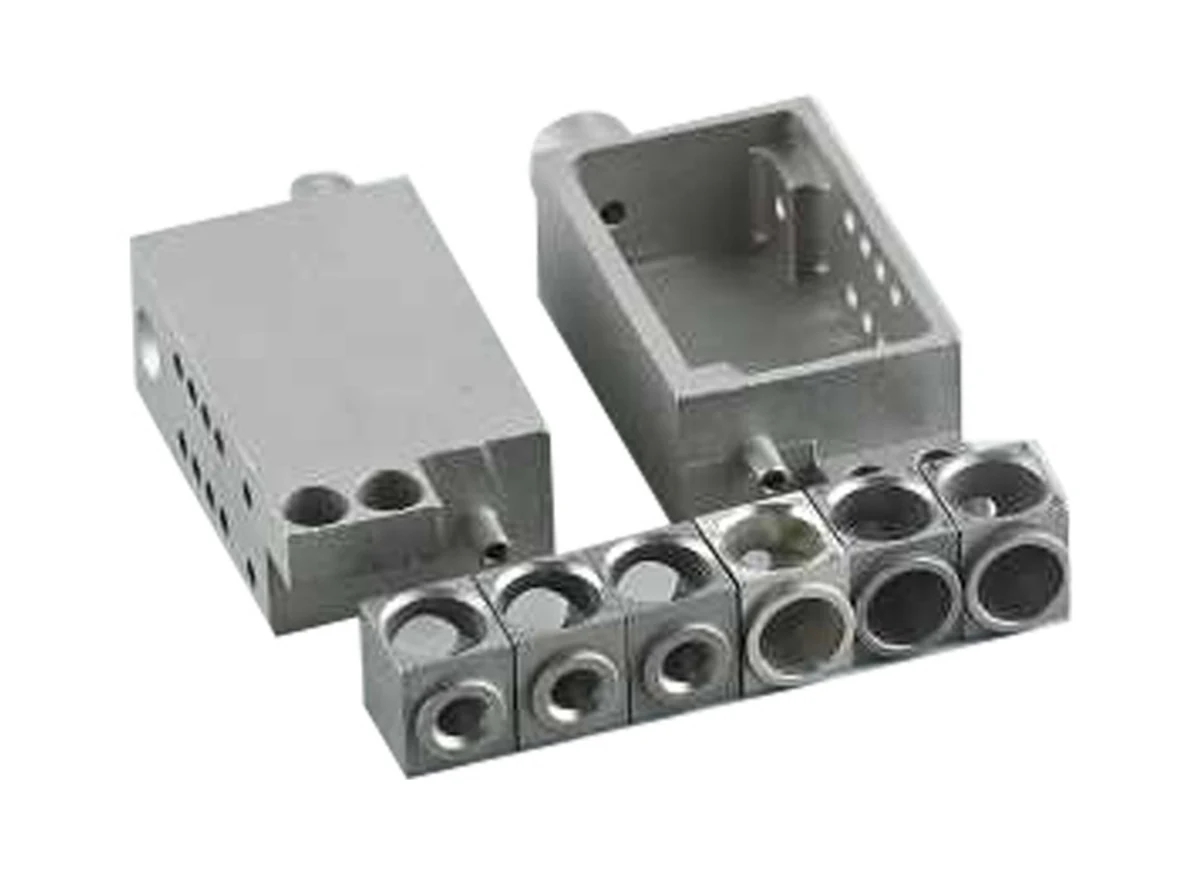
What optoelectronic housings locate and protect
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
The reference shows cavities and multiple openings that require clear alignment and component-scope definitions.
Component-carrying and clearance-only opening interfaces
Identify which openings carry or locate components and which simply provide clearance.
Establish a common datum for the cavity, mounting face and critical aperture positions.
Why relate apertures to the mounting datum?
An aperture's useful position is its relationship to the assembly, not merely its distance from a free outer wall.
Relating openings and mounting features to a common reference makes the intended alignment inspectable and clarifies which surfaces may need final machining.
MIM versus machining for housing detail and alignment access
Compare MIM for integrated housing detail with machining where access and alignment require it.
Internal faces and openings should be checked for finishing and inspection access.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Process fit for optoelectronic housings
A housing looks like a casting job until the aperture positions are examined. The deciding question is whether the openings locate components or merely clear them, because that sets how the position is held through whichever process is chosen.
| Alternative process | When it wins on this part | What puts sintering back in front |
|---|---|---|
| Zinc or aluminium die casting | Wins on the plain housing body. Tool life is long, trimming is fast, and at this size the per-piece cost is the lowest of the four. | Draft, ejector marks and subsurface porosity all sit in the wrong places for an optical cavity: the draft tilts the bore, and porosity only shows up after machining opens it. Sintering holds a bore without draft and forms it in one cycle. |
| CNC from solid | Wins from prototype to low volume, and wins outright on a lens barrel where bore-to-bore coaxiality dominates everything else. | Hollowing a block removes most of the material by volume. Where the cavity is not a solid of revolution, that removal is slow and the shape is what forming is for. |
| Investment casting | Wins on the mid-volume complex cavity that is too large for a pressing tool and too intricate for a two-part die. | Wax patterns scatter more than sintered parts do, and wall uniformity is harder to hold. When the aperture has to align with another component, that scatter is paid for in sorting, not in the casting price. |
| Plastic moulding with a metal insert | Wins wherever the housing only carries structure and neither conducts heat nor shields. | Any thermal path or shielding requirement removes plastic from the comparison at once. So does a screw thread that will be used more than a few times. |
| Powder metallurgy pressing | Wins on the flat base plate with regular hole positions, where the outline is a single pressing direction and the tool is simple. | Openings perpendicular to the pressing direction cannot be filled by a rigid die. One side port is enough to move the part to injection. |
Note. This table is a screening aid, not a recommendation against our own process. Where a row above describes your part better than the sintering route does, we will say so and quote against the route that actually fits; the quantities, alloy and tolerances on your drawing still decide the answer.
One property is usually left out of the comparison: a sintered housing is porous until it is sealed. Internal residue and outgassing have to be raised while the process is being chosen, because sealing is a separate step with its own cost and its own effect on the aperture.
Optoelectronic housing material and finish requirements
Define base material, final condition and cosmetic finish separately.
Identify visible faces, permitted edge rounding and the dimensions that must be met after finishing.
Any magnetic, electrical or acoustic requirement needs its own specification.
Review material-selection information →Aperture location, mounting relationship and internal-clearance checks
Inspect aperture location, mounting relationships and internal clearance.
Optical or electrical performance must be evaluated through the customer's complete assembly requirements.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Does the metal housing determine optical alignment by itself?
No. The mounting method and mating optical components also matter; provide the full locating arrangement.
Why relate apertures to the mounting datum?
An aperture's useful position is its relationship to the assembly, not merely its distance from a free outer wall. Relating openings and mounting features to a common reference makes the intended alignment inspectable and clarifies which surfaces may need final machining.
How are appearance and functional fit checked?
Inspect aperture location, mounting relationships and internal clearance. Optical or electrical performance must be evaluated through the customer's complete assembly requirements.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →