
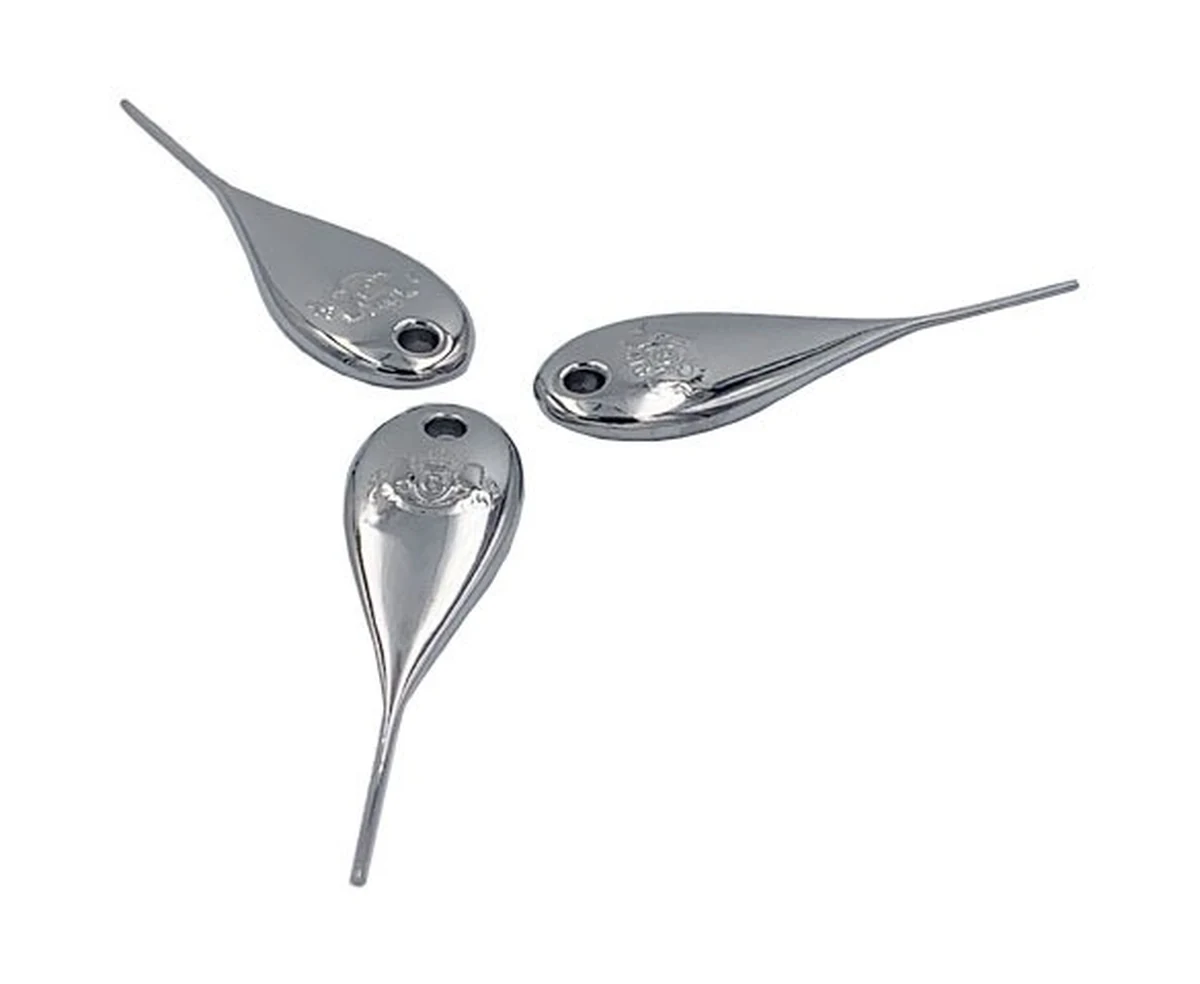
What a phone ejector tool does between grip and tray release
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
The grip and narrow working end need different geometry controls.
Working-end, tip shape and grip-transition interfaces
Define the working-end length and diameter, tip shape and the transition into the grip.
Confirm the tray mechanism and allowable insertion envelope.
Why define both the pin tip and the grip transition?
The working tip must enter the release opening, while the transition connects that slender feature to the user's grip.
Their roles differ, so an overall length check alone leaves important geometry unspecified.
The device interface establishes which tip and transition details matter.
Forming, stamping and machining for grip-to-pin construction
Compare forming, stamping and machining with any joining required between the grip and pin.
A long slender feature needs particular attention to support and straightness.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Ejector tool base material and finish requirements
Define base material, final condition and cosmetic finish separately.
Identify visible faces, permitted edge rounding and the dimensions that must be met after finishing.
Any magnetic, electrical or acoustic requirement needs its own specification.
Review material-selection information →Tip condition, straightness and release-clearance checks
Check tip condition, straightness and clearance to the intended release opening.
Verify operation in the approved device without assuming compatibility with other models.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Where phone ejector tools fail, and why the drawing decides most of it
An ejector tool looks like a pin with a handle, and that is exactly why it gets under-specified. It is used once or twice in the life of a phone by someone who does not know how hard to push, so the failure modes are dominated by bending, by insertion depth and by what the tip does to the frame.
| What goes wrong in service | What drives it | Where the drawing closes it out |
|---|---|---|
| The pin takes a permanent bend on first use | The section between the grip shoulder and the working end is the thinnest part of the tool and carries all the bending when the user levers sideways. If the material condition or the effective section is chosen for cost, the tool yields instead of springing back. | Pin diameter over the free length, material grade and condition, and a minimum bend load with the load applied at the tip rather than at the shoulder; verified on a bend fixture that mimics a thumb load off-axis. |
| The tip will not reach the tray catch | Insertion depth is often dimensioned from the grip face instead of from the shoulder that actually bottoms out on the phone. The tool stops short, the user pushes harder, and the tray never releases. | Overall length plus the effective tip projection measured from the stopping shoulder, with the datum named on the drawing; verified with a go/no-go depth gauge rather than with a caliper over the whole part. |
| A fine scratch appears on the frame around the tray hole | At this scale the tip edge is hard to deburr and a parting line can sit right on the entry chamfer. Both leave a hard edge that scrapes anodising as the tool goes in at a slight angle. | Tip radius and chamfer called out explicitly, plus a burr-free requirement on the insert end only, so the requirement is inspectable; verified at magnification on a sample lot taken after the finishing step rather than before it. |
| The grip separates from the pin | Two-piece tools normally rely on a press fit between pin and grip. If the interference is specified before coating and only the pin is coated, the retention margin quietly disappears on the plated build. | A stated retention force for the joint, conditioned on the post-coating state, and the joint design named as press fit or overmould rather than left to the supplier; verified by a pull test on plated parts from the production lot. |
| The tip jams halfway into the hole | A missing entry radius combined with a tip diameter sitting at the top of its band is enough. The tool enters, wedges, and the user reads the resistance as the tray being stuck. | A stated entry radius at the tip and a diameter band with the gauge size named, so the check does not depend on which end of the tolerance the lot landed; verified with a ring gauge on both ends of the band. |
Note. The table names service failure modes and the drawing features that address them; it sets no acceptance values. Dimensions, tolerances and test criteria come from the project drawing.
Almost everything on this list is decided on the drawing. Diameter over the free length, the datum the insertion depth is measured from, and the edge condition at the tip are all things a competent shop can hold once they are written down; none of them are rescued by tighter incoming inspection. The one item that belongs to process control is the joint retention between pin and grip, because it depends on coating thickness and on press setting rather than on geometry alone. That is also the only item worth sampling destructively.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Is one ejector tool suitable for every phone tray?
No. Working length, opening diameter and the release mechanism must be checked for the intended device.
Why define both the pin tip and the grip transition?
The working tip must enter the release opening, while the transition connects that slender feature to the user's grip. Their roles differ, so an overall length check alone leaves important geometry unspecified. The device interface establishes which tip and transition details matter.
How are appearance and functional fit checked?
Check tip condition, straightness and clearance to the intended release opening. Verify operation in the approved device without assuming compatibility with other models.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →