
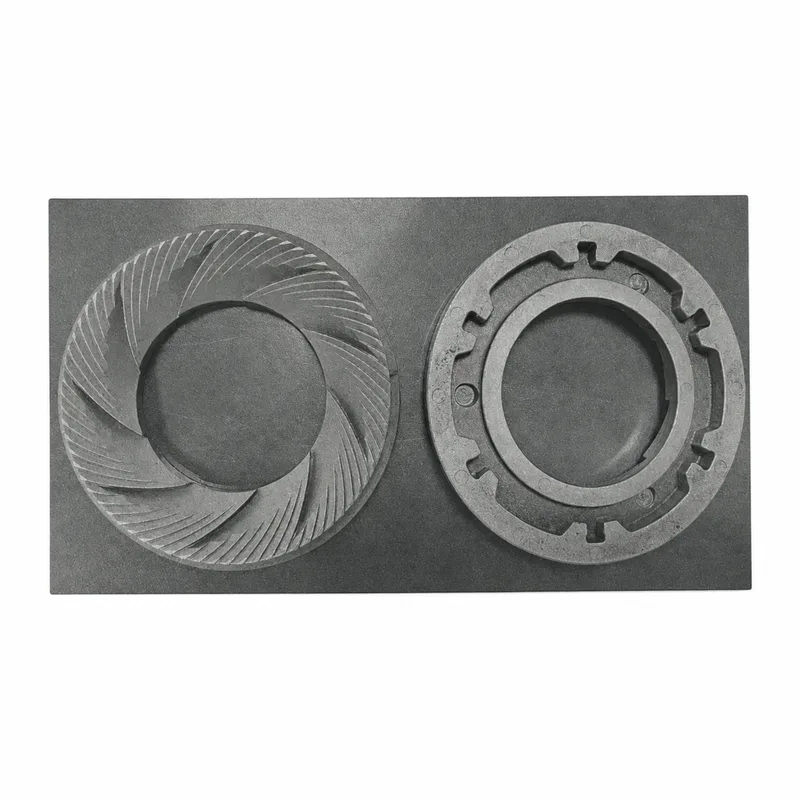
What head burr components combine on the grinding and reverse sides
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
Both sides affect installation and operation.
Grinding side, mounting side and rotation-direction interfaces
Mark the grinding side, mounting side and rotation direction on the drawing.
Reverse-side features must be related to the burr axis and the mating drive rather than treated as cosmetic details.
Why are the back features part of burr accuracy?
The reverse-side features establish how the burr is driven and seated.
They connect the finished grinding profile to the machine's mounting system.
Treating them as secondary cosmetic details can leave the actual operating position undefined even when the working face is well described.
Separating grinding-pattern and reverse-side production
Review the grinding pattern and reverse-side geometry as separate manufacturing features.
Forming may be considered for the body, with machining or grinding for defined functional surfaces.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Head burr grade, edge wear and food-contact requirements
Specify the required grade or performance criteria together with cleaning, wear and appearance requirements.
For any surface that contacts food or beverage, identify the applicable customer documentation and acceptance criteria.
A stainless label is not a complete contact specification.
Review material-selection information →Mounting relationship, tooth condition and drive-engagement checks
Inspect the mounting relationship, tooth condition and drive engagement.
Approve the component as part of the intended grinding head with its mating burr.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →What changes between lots on a grinding burr
A burr pair is judged by the grind it produces, and that depends on tooth form, edge condition, flatness and how the two discs sit together. Only one of those is a dimension in the ordinary sense.
| What drifts between lots | Where the drift comes from | What the release check catches |
|---|---|---|
| Tooth form and pitch | Teeth are formed by the mould and then finished on the working face. The finishing pass removes a fixed depth, so a blank that came in slightly different produces a slightly different tooth height. | Check tooth height and pitch on a finished part, and compare a ground sample with the reference grind. Tooth measurements taken on the blank do not describe the working face. |
| Edge sharpness of the cutting teeth | Sharpness is a result of the last finishing step and of the material hardness. Two lots can meet the same tooth dimensions and cut differently because the edge is rounded differently. | Agree a cutting test on a known load of beans and record the result per lot. Edge condition can also be checked at magnification against a boundary sample. |
| Flatness of the working face | A burr is a disc with a large diameter relative to its thickness, which is the shape that distorts most in sintering. Flatness also changes when the face is ground, depending on how the part was held. | Check flatness in the free state, and check the gap between the two discs when assembled. The gap is the functional requirement; flatness is how it is held. |
| Concentricity of the drive to the tooth circle | The drive is formed on the reverse side and the teeth on the working side, so the two are related only through the tool. Run-out between them appears as uneven loading around the burr. | Measure run-out between the drive and the tooth circle, not the drive on its own. An off-centre burr wears unevenly and the grind changes as it wears. |
| Cleanliness for food contact | Grinding produces fines and finishing media residue that lodge between teeth. Cleaning removes most of it, and the amount left depends on the cleaning process and on how fine the teeth are. | Agree a residue check and a cleaning record per lot, and state the food-contact requirement on the drawing. This is a documented requirement, not something that can be judged by looking. |
Note. This describes how the process behaves across a production run, not the history of any particular lot. Acceptance values, sample sizes and inspection methods come from the project drawing and the agreed quality plan.
Only the concentricity item is a conventional dimension. The rest are outcomes: a grind, an edge, a flatness in the free state, a residue level. Each needs a test or a retained sample to be meaningful, which is why a burr drawing with no agreed cutting test tends to be argued about after delivery rather than before.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Why is a reverse-side drawing needed for a burr?
The reverse side can determine centering, drive engagement and axial seating even when the grinding face appears correct.
Why are the back features part of burr accuracy?
The reverse-side features establish how the burr is driven and seated. They connect the finished grinding profile to the machine's mounting system. Treating them as secondary cosmetic details can leave the actual operating position undefined even when the working face is well described.
How should fit and operating behavior be approved?
Inspect the mounting relationship, tooth condition and drive engagement. Approve the component as part of the intended grinding head with its mating burr.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →