
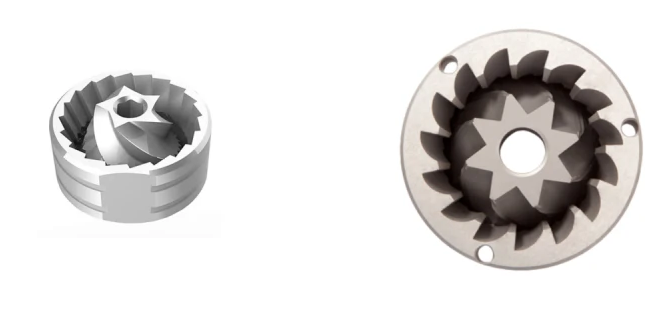
What a conical burr does in a paired grinding set
The reference shows complementary views of a compact toothed form.
Mating burr, axis and mounting-seat interfaces
Supply the mating burr, direction of rotation and installation section.
The rotating axis, mounting seat and grinding profile form one functional system, rather than independent outside dimensions.
Why should burr centering and seating be reviewed together?
The mounting interface establishes where the grinding profile sits relative to its partner.
A correctly produced tooth shape can still be positioned incorrectly if the locating and seating requirements are inconsistent.
The drawing therefore needs one coherent reference scheme for both functions.
Separating burr-body forming from tooth and edge production
Assess forming of the burr body separately from producing the final grinding teeth and edges.
The quotation should identify any machining or grinding, and how the functional profile will be inspected.
Compare manufacturing capabilities →Burr material, edge condition and food-contact requirements
Specify the burr material and final condition together with the required wear and cleaning criteria.
The mating burr and working edges must be included in that review.
A stainless description alone does not define edge behavior, hardness or food-contact documentation for the completed grinder.
Review material-selection information →Centering, mounting-face and tooth-condition checks
Check centering, mounting-face relationship, agreed runout and tooth condition.
Approve grinding behavior in the intended grinder using the customer's test method, not the photograph alone.
Quality documentation →Conical burr sets: taper, alignment and how the gap closes
On a conical set the grind adjustment works by moving one cone along the other. That means the taper angle, the concentricity of the flank to the shaft bore and the axial location all act together: a small alignment error shows up as a grind that changes across the adjustment range rather than as a dimension that fails inspection.
| Feature | What it governs | How it is specified and verified |
|---|---|---|
| Taper angle and flank concentricity | Whether the gap between inner and outer burr closes evenly along the full flank. | Taper angle and coaxiality of the flank to the shaft bore; CMM on a sectioned sample, since a single diameter cannot show it. |
| Tooth zone pattern and land width | Particle size distribution, and whether the burr cuts or crushes at a given setting. | Zone geometry by section on the 2D drawing; profile projector or optical comparator against the drawing. |
| Shaft bore, drive flat and end face | Axial float and the grind-size drift that appears after a few hundred shots. | Bore diameter, flat position and squareness of the end face to the bore; CMM. |
| Inner and outer pairing | Whether the two members were made as a matched set or simply share an outside diameter. | Pairing identification marked on both parts, with a matched grind check recorded before shipment. |
| Edge condition after hardening | Cutting consistency, and whether a rolled edge smears fines into the ground coffee. | Edge criteria at magnification, no rolled or chipped edges; checked on the finished, hardened part. |
Use the dimensions and acceptance criteria on the project drawing.
A conical burr is a poor moulding candidate when the flank pattern has to be generated on a relieving lathe after hardening, because the moulding step then only buys the blank. It is also the wrong route when the cone is large and the section thick: distortion on the taper is hard to hold, and a turned and ground blank is both more predictable and easier to inspect.
What to include in your enquiry
- Drawing and mating dimensions.Supply the mating burr, direction of rotation and installation section. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Check centering, mounting-face relationship, agreed runout and tooth condition. Specify the mating part or inspection fixture.
Common questions
Can one burr be quoted without the mating component?
An individual drawing can support an initial review, but the mating profile and installation are needed to resolve the grinding gap and assembly requirements.
Why should burr centering and seating be reviewed together?
The mounting interface establishes where the grinding profile sits relative to its partner. A correctly produced tooth shape can still be positioned incorrectly if the locating and seating requirements are inconsistent. The drawing therefore needs one coherent reference scheme for both functions.
How should fit and operating behavior be approved?
Check centering, mounting-face relationship, agreed runout and tooth condition. Approve grinding behavior in the intended grinder using the customer's test method, not the photograph alone.