
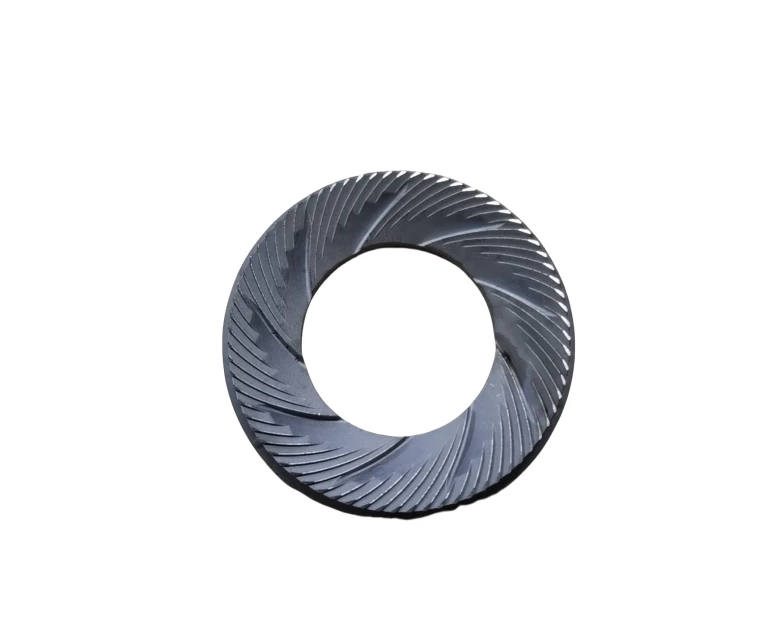
What flat burrs do in a paired grinding arrangement
Their mounting and centering features must preserve the intended relationship between the grinding faces.
Seating face, locating feature and fastener-pattern interfaces
Identify the seating face, central locating feature, fastener pattern and rotation direction.
Define whether a feature locates the burr or merely provides clearance for installation.
Why separate the locating feature from the fixing holes?
A fastener can clamp the burr without precisely locating its center.
If the assembly relies on another diameter or seat for location, the drawing should make that distinction clear.
This avoids assigning the same control to clearance holes and functional centering surfaces.
Near-net body production versus final tooth-pattern machining
Compare near-net body production and machining against the final tooth pattern.
Cutting edges, flatness and locating surfaces may require separate finishing and inspection operations.
Compare manufacturing capabilities →Material and coating requirements for both grinding members
Define the material and final condition of both grinding members.
State whether coatings or other surface treatments are required, and which seating and cutting surfaces must retain their dimensions afterward.
The required wear, cleaning and contact criteria must be agreed for the actual grinder application.
Review material-selection information →Mounting-face flatness, locating diameter and tooth-profile checks
Review mounting-face flatness, locating diameter, tooth profile and edge condition.
Include a matched grinding check under the intended assembly and cleaning conditions.
Quality documentation →Flat burr sets: face flatness, tooth zones and paired delivery
Two flat burrs face each other, and the gap between them is the grind setting. Everything that matters therefore lives on one annular surface: how flat it is, how the teeth are arranged across it, and how well its centre matches the other member of the pair.
| Feature | What it governs | How it is specified and verified |
|---|---|---|
| Annular face flatness | Whether the burr-to-burr gap stays consistent across the full face or opens on one side. | Flatness stated over the annular band rather than the whole blank; surface plate or CMM, after hardening. |
| Tooth zone progression | The pre-break, cut and finish behaviour that shapes the particle distribution. | Zone angles and land widths dimensioned zone by zone; profile projector check against the drawing. |
| Centering bore to the tooth circle | Concentric running, and whether wear stays even or concentrates on one side. | Coaxiality of the bore to the tooth annulus; CMM. A matching outside diameter alone proves nothing. |
| Fastener holes versus locating feature | Whether the screws clamp the burr or also try to locate it, which decides which feature carries the control. | Role of each hole stated on the drawing: clearance, clamp or locate. This is a drawing question before it is a manufacturing one. |
| Pairing and marking | Whether the delivered set is matched and can be identified after installation. | Pairing mark on both parts; matched grind check recorded and traceable to the delivery. |
Use the dimensions and acceptance criteria on the project drawing.
Where a burr is a plain disc with a simple radial tooth pattern and no locating feature, stamping or fine blanking plus a grind is usually cheaper. Moulding pays off when the tooth pattern is complex, the body needs a locating boss and the volumes justify tooling. A very large disc with a wide flat annulus is also difficult to hold flat through sintering, and a turned blank is easier to control.
What to include in your enquiry
- Drawing and mating dimensions.Identify the seating face, central locating feature, fastener pattern and rotation direction. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Review mounting-face flatness, locating diameter, tooth profile and edge condition. Specify the mating part or inspection fixture.
Common questions
Does a matching outside diameter make two flat burrs interchangeable?
No. The tooth pattern, rotation direction, centering and mounting arrangement also need to match the grinder design.
Why separate the locating feature from the fixing holes?
A fastener can clamp the burr without precisely locating its center. If the assembly relies on another diameter or seat for location, the drawing should make that distinction clear. This avoids assigning the same control to clearance holes and functional centering surfaces.
How should fit and operating behavior be approved?
Review mounting-face flatness, locating diameter, tooth profile and edge condition. Include a matched grinding check under the intended assembly and cleaning conditions.