
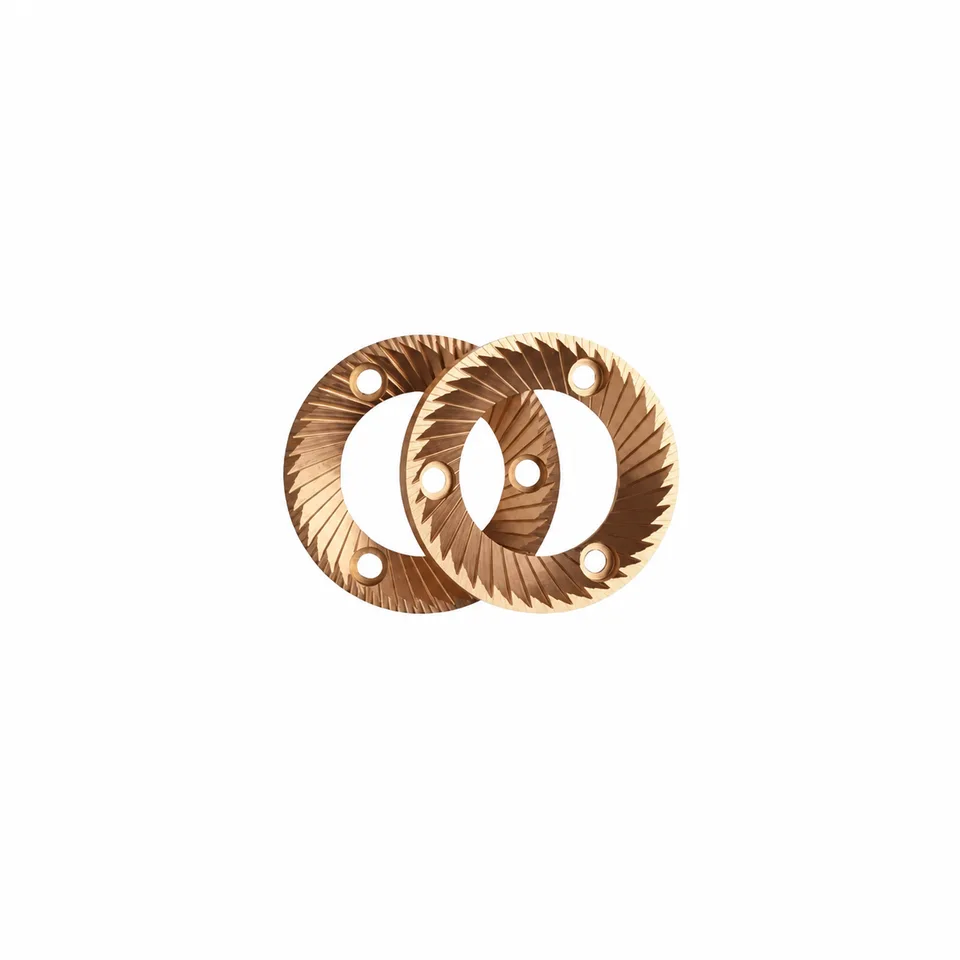
What cutting discs contribute to the assembled grinding relationship
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
Disc seating and the orientation of the working pattern both influence the assembled grinding relationship.
Working face, locating diameter and fastening interfaces
Define the working face, locating diameter and fastening arrangement.
Include the mating disc and distinguish fixing holes from any features used for centering.
Why identify the working face and rotational orientation?
An annular disc may look similar from either side while its seating and working pattern are directional.
Marking the working face and installation orientation connects the manufactured geometry to its intended function and reduces ambiguity when comparing samples or mating parts.
Separating disc-body manufacture from cutting-face production
Compare body manufacture and final cutting-face production separately.
The final profile may require machining or grinding independent of how the blank is formed.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Cutting-disc grade, wear and food-contact requirements
Specify the required grade or performance criteria together with cleaning, wear and appearance requirements.
For any surface that contacts food or beverage, identify the applicable customer documentation and acceptance criteria.
A stainless label is not a complete contact specification.
Review material-selection information →Working pattern, mounting face and fastener-alignment checks
Inspect the working pattern, mounting face and fastener alignment.
Agree how edge condition and installed operation will be evaluated.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Where grinder cutting discs fail, and what the edge does to the cup
A cutting disc is judged by the grind it produces, not by its dimensions, and that makes its failures unusual: a disc can measure perfectly and still produce an inconsistent grind, because the variable that matters is the edge and how the disc sits when it spins.
| What goes wrong in service | What drives it | Where the drawing closes it out |
|---|---|---|
| Fines and inconsistent particle size | A burr on the cutting edge, or an edge radius that varies around the pattern, changes how each passage shears. The result is a bimodal grind: some particles shatter, some are cut, and the cup tastes of the fines. | The working edge defined as a feature with an edge condition requirement, and the measurement method named; verified by a grind-particle check on an assembled grinder rather than by a dimensional report. |
| The machine vibrates and the grind setting drifts | Runout comes from three sources that all look alike: disc flatness after forming, the locating fit to the carrier, and mass distribution around the pattern. Fixing one without the other two does not remove the vibration. | Flatness, the locating diameter and its fit stated as separate requirements; verified by measuring runout on the carrier the disc is actually mounted to, since a flat disc on a bad carrier still vibrates. |
| The grind drifts over months of use | Every disc wears; the question is whether it wears evenly. An edge geometry that starts sharp but has little support behind it rounds quickly at the tips, and the grind coarsens before the disc looks worn. | Edge geometry shown on the drawing with the wear-relevant dimension identified, plus material hardness; verified by a life test that measures grind at intervals rather than only at the start. |
| Staining on the food-contact face | Coffee oils and moisture sit in surface porosity and in scratches, and a stainless that has not been properly passivated stains around them. | Grade, passivation and a surface finish on the food-contact face stated, with the finish requirement applying to the face that meets the grounds; verified after a staining test that leaves residue on the part for a defined period. |
| The fastening loosens | The screw seats on a countersink, and a countersink that does not match the screw head angle contacts on a line rather than a cone. Under vibration the joint relaxes. | Countersink angle and diameter toleranced against the specified fastener, with the seat face identified; verified with the production screw and a torque-retention check after vibration. |
Note. The table names service failure modes and the drawing features that address them; it sets no acceptance values. Dimensions, tolerances and test criteria come from the project drawing.
Two of these are edge questions and two are fit questions, and they fail in different ways. Edge problems show up as taste and consistency, which means they are caught by the customer rather than by inspection, so the requirement has to be written into the drawing and checked on an assembled grinder. Fit problems show up as noise and vibration, and a shop can hold them if the drawing separates flatness from locating fit instead of bundling both into a runout callout. The fastening item is the one that is purely a paired specification: the countersink is only right relative to a named screw.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Can a cutting disc be flipped to reverse its working direction?
Do not assume so. The tooth pattern, seating and rotation direction must be specified for the intended installation.
Why identify the working face and rotational orientation?
An annular disc may look similar from either side while its seating and working pattern are directional. Marking the working face and installation orientation connects the manufactured geometry to its intended function and reduces ambiguity when comparing samples or mating parts.
How should fit and operating behavior be approved?
Inspect the working pattern, mounting face and fastener alignment. Agree how edge condition and installed operation will be evaluated.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →