
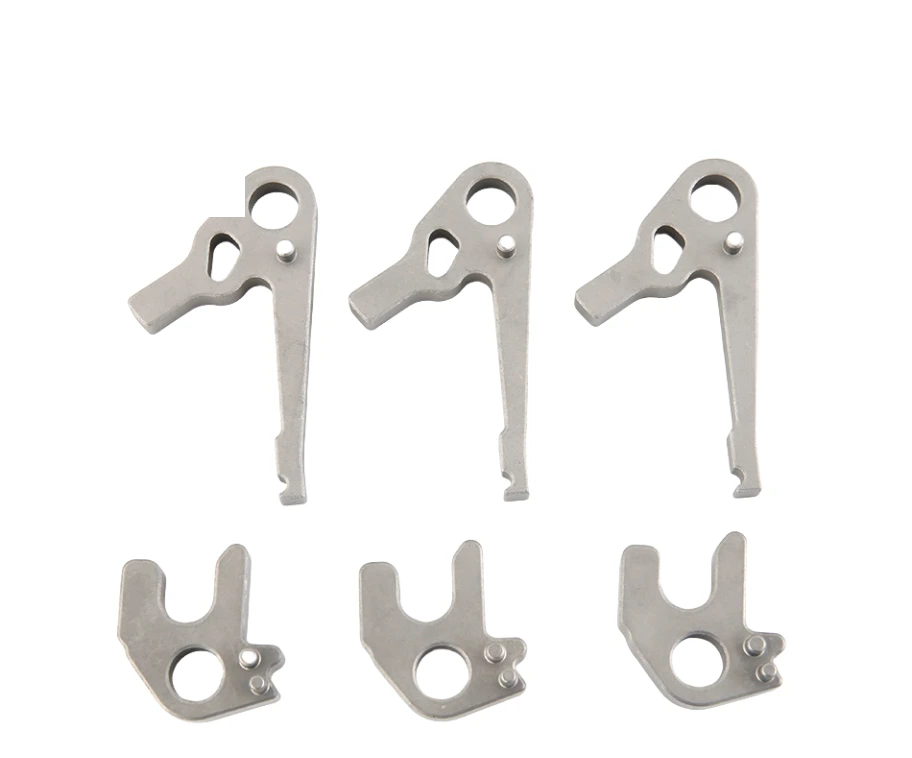
What actuator levers connect between driven and locking elements
Forked or open-ended forms may locate a pin, follow a profile or transfer force.
Pivot, working end and actuator interfaces
Specify the pivot, working end and relationship to the actuator.
Identify the load direction and motion range of each lever.
Why identify which end of the lever drives the mechanism?
Different ends can locate, follow or transfer motion, and their requirements follow those roles.
An assembly reference identifies the force and movement relationship.
This helps distinguish a working contact from a simple retaining or clearance feature.
MIM, stamping and machining by section and geometry
Compare MIM, stamping and machining according to section and integrated geometry.
Finishing of holes and contacts should follow the required fit.
Compare manufacturing capabilities →Actuator lever material, treated-surface and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
Specify any testing required on the assembled lock separately.
Review material-selection information →Hole position, end contact and operating-sequence checks
Check hole positions, end contact and clearance through the operating sequence.
Approve the final part with its actual driven mechanism.
Quality documentation →What changes lot to lot on a MIM actuator lever
A lever is long and thin, which is the shape a sintered part is least uniform at. Shrinkage is not the same along the length as across it, and the two features that matter, the pivot and the working end, sit at opposite ends of that difference.
| What drifts between lots | Where the drift comes from | What the release check catches |
|---|---|---|
| Pivot bore position along the length | Shrinkage in a long thin section depends on how the feed fills the cavity. The end farthest from the gate sinters from a slightly lower green density, so the distance between pivot and working end moves more than either feature moves on its own. | Dimension the working end from the pivot bore, and check that distance on a CMM across the run rather than only at the start. Where both features are dimensioned from a common outside edge, the two errors add instead of being controlled. |
| Squareness of the pivot bore to the lever face | The core pin forming the bore can shift slightly as the feed cools, and any tilt is exaggerated over the lever length even though the bore itself measures correctly. | Check squareness, or the end-to-end offset it produces, not only the bore diameter. A bore that passes a plug gauge can still put the working end out of plane. |
| Working-end profile against its mating part | The profile is formed by the mould, but its final position relative to the pivot depends on how far the part is sized. Sizing corrects the bore and can move the profile with it. | Compare the profile to the mating part or to a stated profile tolerance, using the pivot as the datum. Where the end follows a cam, ask for the cam drawing rather than a general tolerance on the outline. |
| Flatness in the free state | Long thin parts distort in sintering and again in heat treatment. How they sit in the furnace and how they are stacked for tempering change the result more than the drawing tolerance suggests. | Measure flatness with the part unrestrained, and say so on the drawing. A flatness callout checked while the part is clamped to a plate will pass levers that spring when the fixture is released. |
| Plating thickness inside the pivot bore | Electroplating throws more metal on edges and less inside a bore, and the throw varies with bath condition. Two lots can both meet a thickness callout outside and differ inside. | Gauge the bore after plating. Where the lever pivots on a pin, set the bore and the pin as a pair in the delivered condition. |
Agree on the sample size and inspection method before production.
This is a part where the datum choice does most of the work. Dimensioned from the pivot, four of these five items can be checked and argued about with numbers. Dimensioned from an outside edge, the same parts produce readings that cannot be compared between lots.
What to include in your enquiry
- Drawing and mating dimensions.Specify the pivot, working end and relationship to the actuator. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Check hole positions, end contact and clearance through the operating sequence. Specify the mating part or inspection fixture.
Common questions
Is an actuator lever the same as a lock retaining plate?
No. Identify the function on the assembly drawing so its movement and contact requirements are not confused with static retention.
Why identify which end of the lever drives the mechanism?
Different ends can locate, follow or transfer motion, and their requirements follow those roles. An assembly reference identifies the force and movement relationship. This helps distinguish a working contact from a simple retaining or clearance feature.
How should the completed mechanism be checked?
Check hole positions, end contact and clearance through the operating sequence. Approve the final part with its actual driven mechanism.