
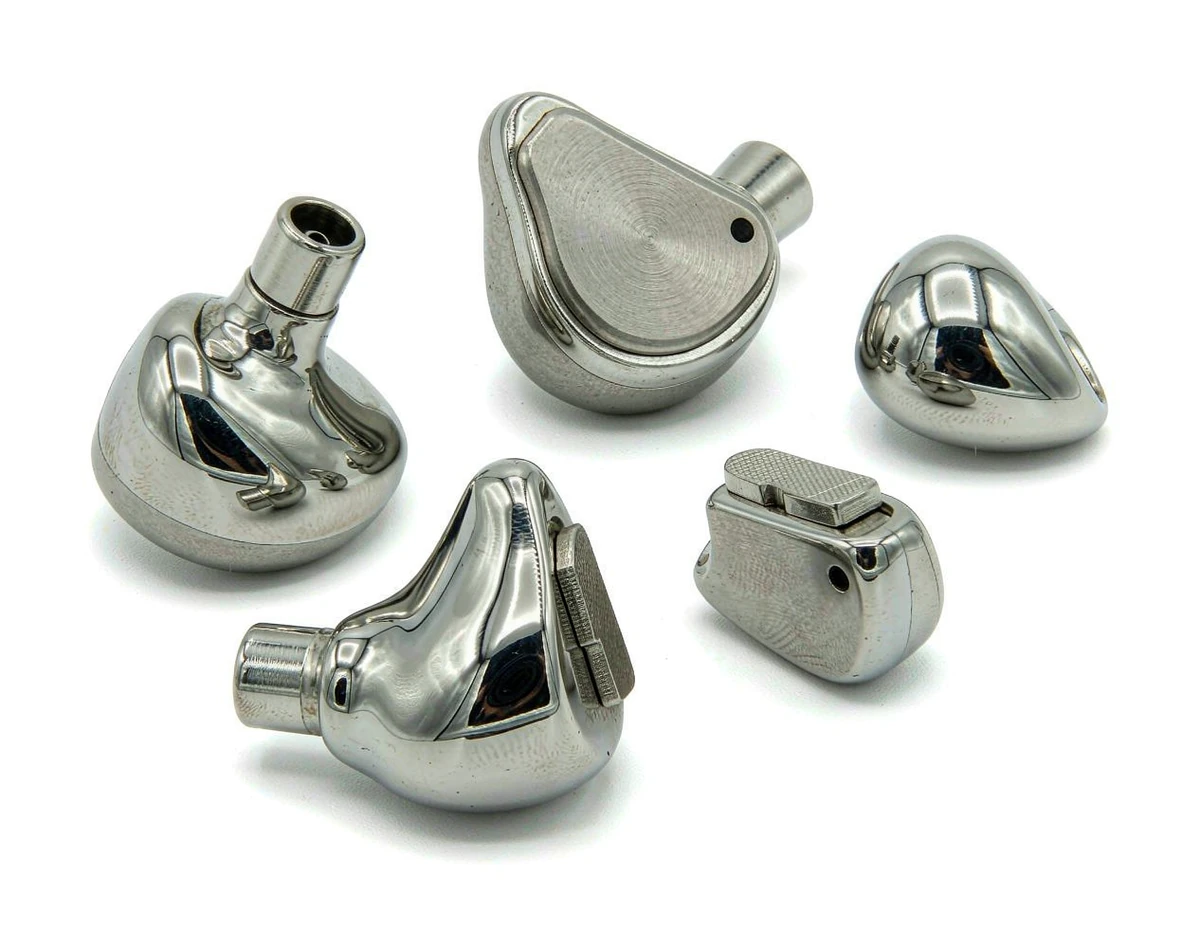
What an in-ear housing encloses and interfaces with
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
Related housing geometry is illustrative; the acoustic layout remains customer-defined.
Internal clearance, joint surfaces and acoustic-opening interfaces
Specify internal component clearance, joint surfaces, acoustic openings and external contact regions.
Keep sealing, locating and cosmetic requirements distinct.
Why separate housing manufacture from acoustic evaluation?
The metal housing can be inspected for its envelope, openings and joints.
Acoustic evaluation concerns how those features work with the other components in the completed design.
The two sets of requirements should be connected through the drawing, not assumed to be equivalent.
MIM versus machining for in-ear housing enclosures
Compare MIM and machining for the enclosure and integrated features.
Small openings and joint faces need a clear finishing and inspection plan.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →In-ear housing material, joint and finish requirements
Define base material, final condition and cosmetic finish separately.
Identify visible faces, permitted edge rounding and the dimensions that must be met after finishing.
Any magnetic, electrical or acoustic requirement needs its own specification.
Review material-selection information →Internal envelope, opening location and closure-fit checks
Check internal envelope, opening location, closure fit and finish.
Acoustic behavior must be evaluated with the complete transducer and housing assembly.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Where an in-ear shell drawing meets the tool
A shell is a cosmetic part that also happens to be an acoustic chamber and a battery holder. Those three duties pull against each other, and the changes below are where the drawing usually has to pick which one wins.
| What we flag | Why it bites on this part | How the drawing usually changes |
|---|---|---|
| Wall thickness around the chamber | A wall that varies by more than about 0.2 mm changes the chamber volume after shrink, and the tuning that was done on a machined prototype no longer matches. | The wall is brought to one nominal thickness, and any local thickening for a screw boss is moved outside the chamber rather than inside it. |
| Gate position against the visible face | MIM leaves a gate mark where the feedstock entered. On a part that is handled and photographed, that mark has to be on a face nobody looks at. | The gate is drawn onto a hidden face or a face that is machined afterwards, and the drawing says which face is cosmetic so the tool is not cut blind. |
| The surface finish call | Stainless cannot be anodised, so the usual phone-industry finish is not available. PVD, electropolish and bead blast give three different looks and three different costs. | The finish is named as a process with a target Ra and a colour reference, not as "brushed" or "premium". |
| The interface to the driver and the battery | Two tight fits in the same shell stack their tolerances, and the shell is the part that gets blamed when the assembly rattles. | One interface locates and the other floats, with a compliant feature taking up the stack. |
| Snap features moulded in | Sintered stainless has low elongation, so a snap arm that works in moulded plastic will either not deflect or will crack on the first engagement. | The snap becomes a separate spring steel part or a stamped clip, or the closure becomes a screw or an adhesive bond. |
Note. These are the changes we most often ask for on this class of part, not a review of any particular drawing. They describe how the process behaves; dimensions, tolerances and acceptance values come from the project drawing.
The item we push back on hardest is a cosmetic spec written as a standard rather than a process. "No visible defects" on a sintered surface is not a requirement anyone can inspect against, and it usually means the first batch is rejected for something that was never defined.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Does the metal housing alone determine acoustic performance?
No. Transducer, vents, seals and the complete acoustic design must be specified and tested together.
Why separate housing manufacture from acoustic evaluation?
The metal housing can be inspected for its envelope, openings and joints. Acoustic evaluation concerns how those features work with the other components in the completed design. The two sets of requirements should be connected through the drawing, not assumed to be equivalent.
How are appearance and functional fit checked?
Check internal envelope, opening location, closure fit and finish. Acoustic behavior must be evaluated with the complete transducer and housing assembly.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →