
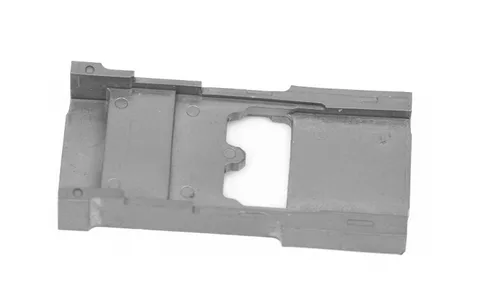
What frame inserts support inside a phone enclosure
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
Long edges and internal openings must align with the surrounding housing and installed components.
Attachment datums, opening positions and surrounding-space interfaces
Define the attachment datums, opening positions and available space around the insert.
Flatness and straightness may matter to assembly even if the part is not externally visible.
Why use assembly datums for an elongated insert?
The insert's working position is established by its attachment or locating features.
An unconstrained long edge can be a poor description of that position.
Assembly-based references clarify whether straightness, seating or opening alignment is the feature that actually controls fit.
Machining, stamping and near-net forming for thin sections
Compare machining, stamping or near-net forming for the section and quantity.
Thin elongated sections need a route that preserves their finished mounting relationship.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Frame insert material and finish requirements
Define base material, final condition and cosmetic finish separately.
Identify visible faces, permitted edge rounding and the dimensions that must be met after finishing.
Any magnetic, electrical or acoustic requirement needs its own specification.
Review material-selection information →Seating, window position and assembly-interference checks
Inspect seating, hole or window position and any interference during enclosure assembly.
Specify visible edges and finish only where they are actually exposed.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Where the cost sits on a thin frame insert
A frame insert is a flat part with openings, bought in phone quantities and judged on how flat it stays. Its cost profile is dominated by flatness and by the process chosen for a thin section.
| Cost element | Why a small order costs more per piece | Why a large order stops getting cheaper |
|---|---|---|
| The tool and its flatness control | A long thin part needs a tool that keeps the whole length supported. Tool cost is moderate, and flatness is designed into it rather than corrected afterwards. | Tooling is one-off. Tool maintenance returns with stroke count, so a long programme pays for re-polishing the face more than once. |
| Process choice for a thin section | Stamping or etching can be cheaper than forming for a uniform thin part, and both avoid the distortion that sintering introduces. Forming wins where there are bosses or local thickness changes. | If stamping is viable, its cost per part falls faster with volume than forming does. The process decision sets the slope of the whole cost curve. |
| Flattening or coining | Formed thin parts need flattening, which is per part. A stamped part often does not, which is one reason the two routes diverge. | Flattening can be automated but not eliminated without a design change. On a stamped blank the operation does not exist at all. |
| Finishing on a large flat area | Coating, anodising or brushing are priced on area, and a frame insert has a lot of it for very little mass. | Area does not scale down. This is a linear line at any quantity. |
| Flatness and window-position checks | Both need a fixture or a CMM programme, and both are per lot rather than per part. | The fixture is one-off, the checks are fast. This is the line that makes a second order cheaper than the first. |
Note. The split below describes cost structure, not prices. What a specific part costs depends on its geometry, material, finish and the quantity you can commit; this page explains which of those you can move and which you cannot.
The question worth asking on a frame insert is whether the wall is uniform. If it is, the honest comparison is against stamping or etching, and that comparison will often win. Forming earns the order when the insert carries local thickness changes that a stamped blank cannot produce.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Should a frame insert be dimensioned from its outermost edge?
Use the assembly datums that locate it; a cosmetic or clearance edge may not be a suitable primary datum.
Why use assembly datums for an elongated insert?
The insert's working position is established by its attachment or locating features. An unconstrained long edge can be a poor description of that position. Assembly-based references clarify whether straightness, seating or opening alignment is the feature that actually controls fit.
How are appearance and functional fit checked?
Inspect seating, hole or window position and any interference during enclosure assembly. Specify visible edges and finish only where they are actually exposed.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →