
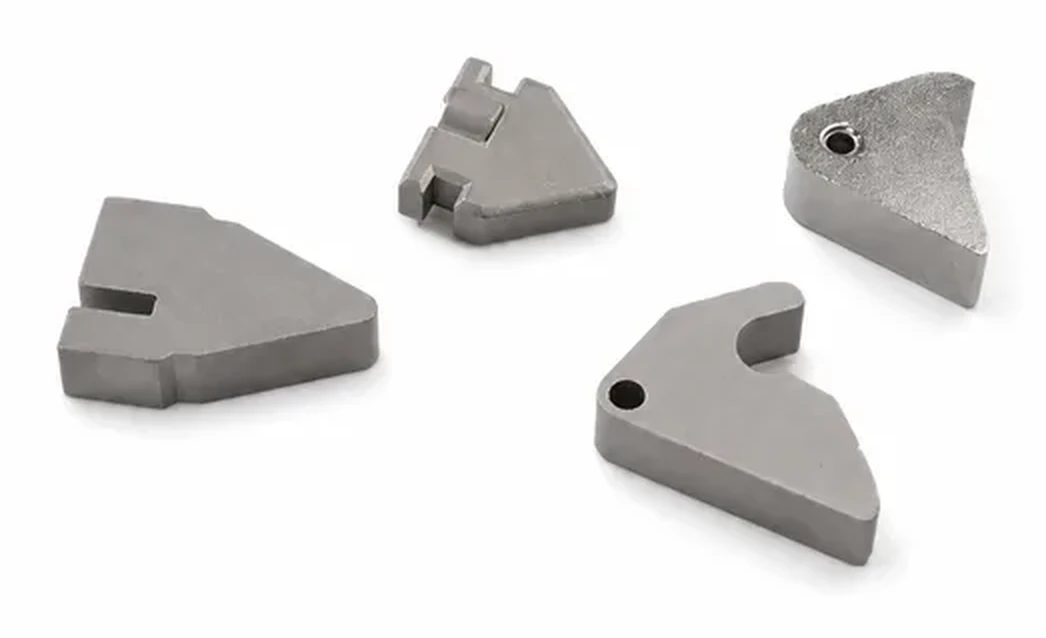
What a black-oxide latch request specifies beyond the part
The reference shows latch forms; appearance in a photograph does not verify their treatment or substrate.
Guiding, engaging and connecting-surface interfaces
Define the guiding, engaging and connecting surfaces.
State which features require dimensional control after the specified treatment and any supplementary protection.
Why specify substrate and treatment independently?
A finish description does not identify the underlying material or the full delivered condition.
Separate specifications allow the manufacturing sequence and inspection to address both.
The final component must still meet its functional fits after the agreed treatment.
Forming, then reviewing the substrate and treatment sequence
Compare forming and machining for the latch geometry, then review the material and finishing sequence.
Confirm that the requested treatment is appropriate for the specified base material.
Compare manufacturing capabilities →Black-oxide substrate, treatment and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
Specify any testing required on the assembled lock separately.
Review material-selection information →Final fit, engagement and surface-condition checks
Check final fit, engagement and agreed surface condition.
Any corrosion or wear target requires a separate specification and acceptance method.
Quality documentation →How black-oxide latch bolts fail, and what the finish can and cannot do
Black oxide is a surface conversion, not a barrier coating, and most bolt complaints come from expectations built on the second assumption. It holds oil, it gives a consistent dark appearance, and it does very little on its own against moisture in a cavity that never dries out.
| What goes wrong in service | What drives it | Where the drawing closes it out |
|---|---|---|
| Red rust appears at holes and cut edges after humidity cycling | The coating is thinnest exactly where the geometry is hardest to reach. Blind holes, thread roots and sheared edges get a fraction of the film that a flat face gets, so the first corrosion is always local and always at a feature rather than spread over the surface. | The substrate grade and its corrosion behaviour stated on the drawing, with black oxide named as an appearance and oil-retention treatment rather than as corrosion protection; verified by a humidity or salt-spray test on parts that include the holes and edges, not on polished coupons. |
| Bare grey metal shows on the sliding face | The film is thin and soft. Where the bolt runs against the guide, it wears through and exposes substrate, and the user sees a bright streak on a black bolt long before anything measures out of tolerance. | Wear surfaces identified by zone, with a requirement that the coating condition be judged on the functioning part after a stroke test; verified by running an assembled sample and inspecting the contact band rather than the delivered part. |
| Colour varies from lot to lot | Final colour depends on the substrate alloy and on how the surface was prepared. A polished part and a blasted part take the same treatment and come out visibly different, and both can be inside a loose appearance note. | Surface preparation stated per face, plus a colour reference the inspector can hold against the part; verified against the reference under the lighting the product is assembled under, on a sample from each lot. |
| A hardened lot cracks after treatment | Acid pickling before black oxide introduces hydrogen, and a hard substrate keeps it. The crack appears after assembly, which makes it look like an application problem rather than a process one. | Substrate hardness stated on the drawing, with a baking requirement triggered by that hardness; verified by a bend or sustained-load test on treated parts from a hardened lot, not on soft samples. |
| The bolt feels tacky and collects dust | Post-treatment oil is what carries most of the corrosion resistance, so more oil looks like more protection. In a dusty cavity it does the opposite and turns into a collecting surface. | The after-treatment named, with the oil or wax carrier identified and an upper limit on film; verified by a touch and residue check on packed parts, since the condition changes in the bag. |
Use the project drawing for tolerances and acceptance limits.
This is the one finish in the group where the drawing usually carries the wrong expectation. A black-oxide note is often written as if it were plating, and no process control can make a conversion coating behave like a barrier. What the process can control is film uniformity, colour consistency and the absence of hydrogen damage, and all three are worth writing down. What it cannot control is whether the substrate is corrosion-resistant enough for the cavity the bolt lives in. That question belongs to the grade choice, and it is better answered there than in a salt-spray argument after the first field returns.
What to include in your enquiry
- Drawing and mating dimensions.Define the guiding, engaging and connecting surfaces. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Check final fit, engagement and agreed surface condition. Specify the mating part or inspection fixture.
Common questions
Does a dark surface alone prove a black-oxide treatment?
No. Confirm the treatment specification, base material and required inspection documents independently of the image.
Why specify substrate and treatment independently?
A finish description does not identify the underlying material or the full delivered condition. Separate specifications allow the manufacturing sequence and inspection to address both. The final component must still meet its functional fits after the agreed treatment.
How should the completed mechanism be checked?
Check final fit, engagement and agreed surface condition. Any corrosion or wear target requires a separate specification and acceptance method.