
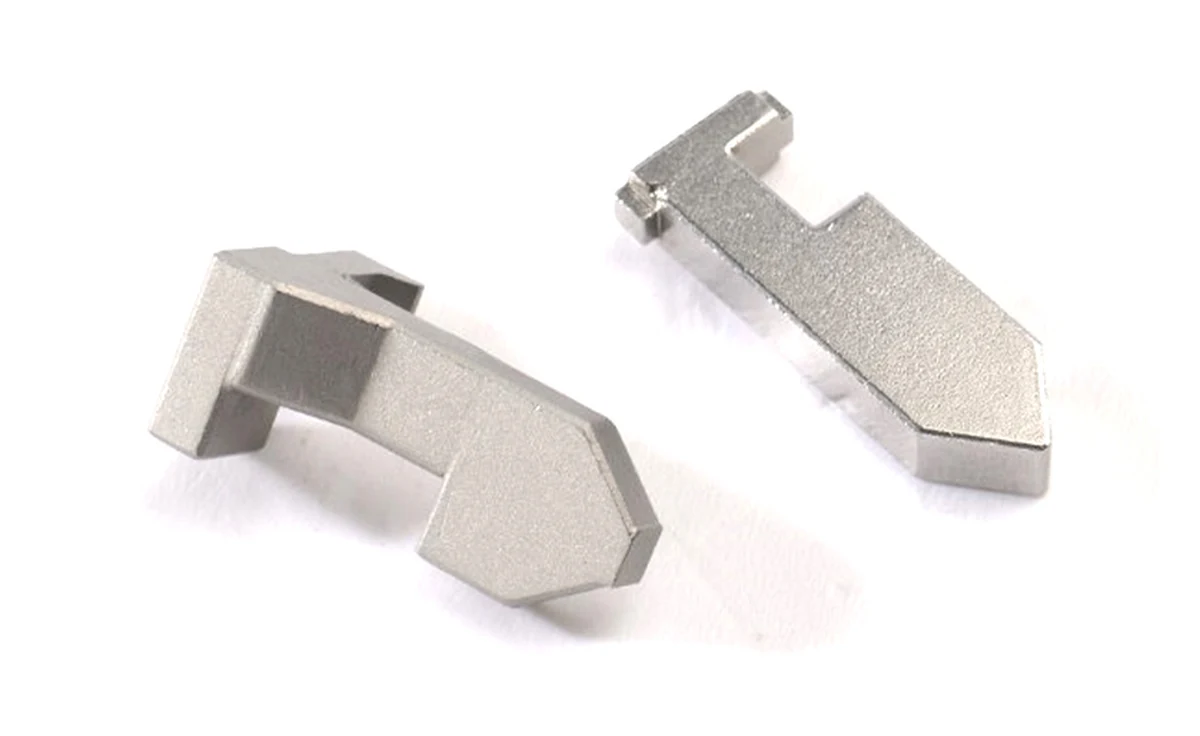
What a latch profile does on engagement and release
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
The reference shows shaped contact faces and connecting geometry for a drawing-based review.
Engagement depth, working direction and guide interfaces
Define engagement depth, working direction, guides and connection to the operating mechanism.
Separate contact faces from surfaces that merely provide clearance.
Why check release as well as engagement?
A latch must move between working states within the surrounding mechanism.
A part that engages in a static inspection does not automatically demonstrate correct release.
The acceptance plan should describe the intended action and the mating parts used to evaluate it.
Near-net forming versus machining for latch profiles
Compare near-net forming with machining for the profile and section.
Critical contact and connecting surfaces may require finishing after the body is formed.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Latch profiles: which route survives the release test
A latch is usually inspected on engagement depth, and usually fails on release. Release depends on the return path having no interference anywhere along its travel, which is a property of the profile as a whole rather than of any single dimension on the drawing.
| Alternative process | When it wins on this part | What puts sintering back in front |
|---|---|---|
| Fine blanking | Wins on the flat latch where the sheared face is the working face. The edge quality is available immediately, with no secondary sizing. | A latch with a locking ramp and a guide step is no longer flat. Adding those as separate parts puts the ramp angle tolerance into an assembly, where it drifts with every fastener. |
| Stamping plus grinding | Wins where the ramp is needed but the thickness is uniform, since the angle can be ground after blanking without a die change. | Grinding is a per-piece operation with a per-piece setup, and it has to be repeated for every angle revision. A formed ramp carries the angle in the tool and reproduces it without labour. |
| CNC machining | Wins on the prototype and on the irregular latch, where the ramp and the pin hole have to be referenced from one another in a single setup. | Cycle time stays high regardless of quantity, so the route never becomes the volume answer. It stays the right way to prove the design and the wrong way to supply it. |
| Investment casting | Wins on the larger latch where the section is too heavy for sintering and the surface can be machined afterwards. | The working face is a sliding contact. Cast surface plus machining on that face means the ramp angle depends on how the part was set up, which is a source of variation the drawing cannot see. |
| Sintering | Wins where the ramp, the guide step and the spring seat exist on one small body, and the hardening follows in the same production cycle so the whole body has one strength. | It loses where the latch is a plain flat plate. There, fine blanking is cheaper and gives a better working edge on the same outline. |
Note. This table is a screening aid, not a recommendation against our own process. Where a row above describes your part better than the sintering route does, we will say so and quote against the route that actually fits; the quantities, alloy and tolerances on your drawing still decide the answer.
Whatever the route, release cannot be inspected on the part alone. State the working direction and the return path on the drawing, and agree how release is demonstrated in the sample report. Without that, a part can pass every dimensional check and still jam in the field.
Latch material, treated-surface and corrosion requirements
Specify the base material, final condition and corrosion or appearance requirements.
Mark drive, guiding and contact surfaces that must meet their dimensions after treatment.
The component specification does not establish a security rating for the complete lock.
Review material-selection information →Engagement, release and guiding-clearance checks
Check engagement, release and guiding clearance in the finished assembly.
Include the agreed material and environmental requirements.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Why should the mating strike or engaging member be included?
It defines the actual contact and clearance, which cannot be established from the latch outline alone.
Why check release as well as engagement?
A latch must move between working states within the surrounding mechanism. A part that engages in a static inspection does not automatically demonstrate correct release. The acceptance plan should describe the intended action and the mating parts used to evaluate it.
How should the completed mechanism be checked?
Check engagement, release and guiding clearance in the finished assembly. Include the agreed material and environmental requirements.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →