
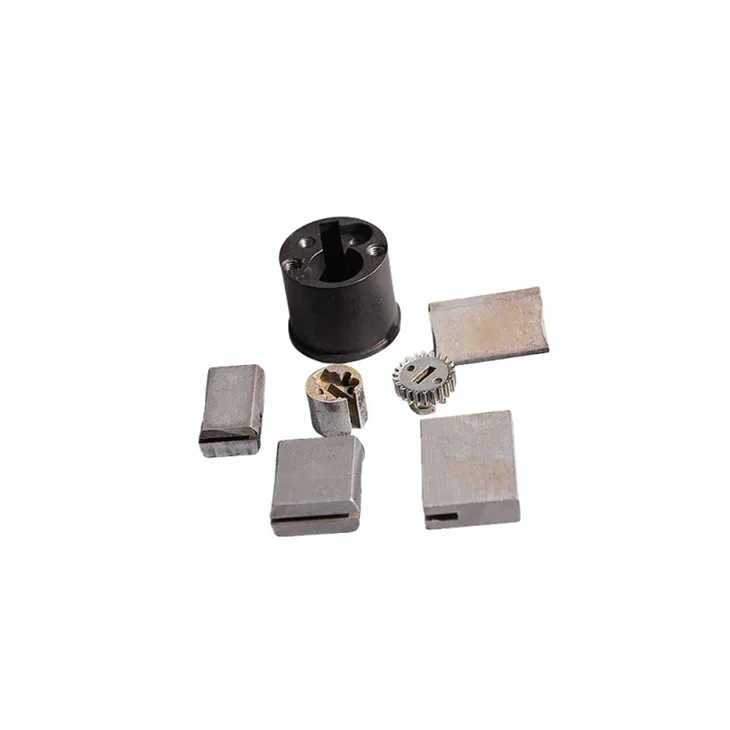
What sintered blocks provide within an assembly
Different steps, holes and wall sections affect how the part can be formed and located.
Load-bearing faces, side holes and section-change interfaces
Identify the load-bearing and locating faces, side holes and section changes.
State whether a hole is formed in the main pressing direction or needs later machining.
Why separate formed features from secondary holes?
A feature's position and direction can affect how it is produced.
Distinguishing the basic formed shape from later holes or threads clarifies tooling assumptions and the datums for subsequent machining.
It also makes the final inspection sequence easier to define.
Conventional PM versus machining against pressing direction
Compare conventional PM and machining with attention to pressing direction and tooling access.
Transverse holes, threads or close mating surfaces may need secondary operations.
Compare manufacturing capabilities →Sintered block material, density and treatment requirements
Material and final condition must be reviewed against the defined load, wear, lubrication and environment.
Where powder processing is proposed, agree any relevant density and treatment requirements.
A material family or hardness value alone does not specify the gear or bearing duty.
Review material-selection information →Sintered blocks: the chain runs along the pressing direction
In a pressed block the chain has a direction. Features formed in the pressing direction are held by the tool; features that cross it are not, and that single distinction divides every link below.
| Link in the assembly chain | What it adds to the stack | Where to take it out of the chain |
|---|---|---|
| Load-bearing and locating faces | These faces carry the chain. They are formed in the pressing direction, so the tool holds their position, but flatness is lost somewhat in sintering and comes back only if the part is sized. | Decide whether sizing is part of the route before quoting. Sizing closes the flatness link and it costs a tool; leaving it out closes nothing and the assembly absorbs the difference. |
| Side holes | A hole that crosses the pressing direction cannot be formed by a rigid die. It becomes a second operation, and a second operation re-establishes its own datum. | Say explicitly which holes are formed and which are drilled. Mixing them under one positional tolerance gives a band that neither feature can meet, and the drilled ones will be blamed. |
| Section changes and steps | A step is a position along the pressing direction. Multi-level pressing holds it well; a single-level tool cannot, and the step then depends on the fill. | State the step height as a functional dimension with its own tolerance rather than inheriting a general band. Steps are where density variation shows up first as a dimension. |
| Wall thickness around the block | Thin walls at the periphery fill less than the core, so density is not uniform across the block. That non-uniformity becomes dimensional scatter after sintering. | Keep wall sections as even as the function allows, and state the minimum wall as a requirement. It is the one geometry decision that changes the process rather than the tolerance. |
| Density and treatment | Density is not a dimension but it behaves like one: it moves size during sintering and it sets the strength the faces can carry. | Specify a density range rather than a single figure, and say which faces it applies to. A single density number on a block with varying wall is a number the process cannot deliver uniformly. |
The assembly designer sets the tolerance allocation. Mark the controlling dimensions on the component drawing.
The useful rule for pressed blocks: whatever is formed in the direction of pressing is a link you can hold, and whatever crosses it is a link you have to buy. Knowing which is which before quoting keeps the chain honest.
Seating, hole position and density checks
Inspect seating, hole position and any specified density or material requirement.
Approve the part under its defined support or mounting function.
Quality documentation →What to include in your enquiry
- Drawing and mating dimensions.Identify the load-bearing and locating faces, side holes and section changes. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Inspect seating, hole position and any specified density or material requirement. Specify the mating part or inspection fixture.
Common questions
Can a transverse hole always be formed during pressing?
Do not assume so. Its direction and tooling requirements need review, and secondary machining may be the appropriate route.
Why separate formed features from secondary holes?
A feature's position and direction can affect how it is produced. Distinguishing the basic formed shape from later holes or threads clarifies tooling assumptions and the datums for subsequent machining. It also makes the final inspection sequence easier to define.
Which checks should be included in gear or support approval?
Inspect seating, hole position and any specified density or material requirement. Approve the part under its defined support or mounting function.