
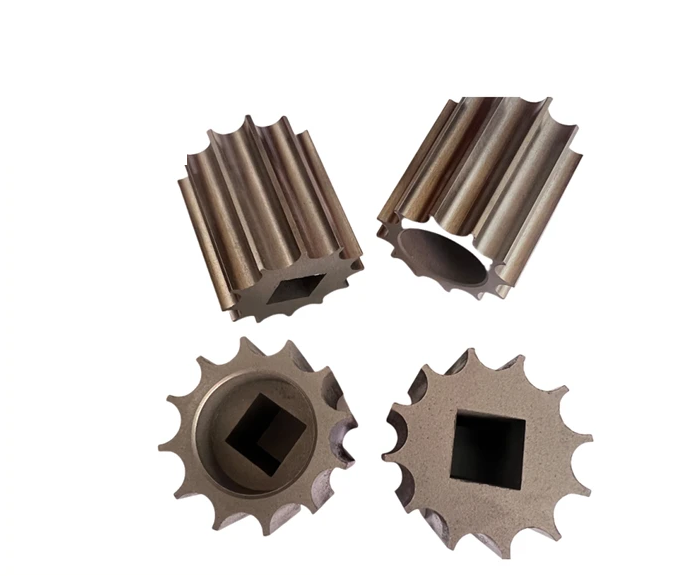
What splined drive parts transfer between profile and bore
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
The elongated reference forms differ from the compact agricultural gear examples.
Profile standard, engagement length and internal-drive interfaces
Specify the profile standard or full geometry, engagement length and internal drive.
Relate both profiles to the locating axis and end faces.
Why include spline engagement length?
The mating relationship extends along the profile rather than existing at a single cross-section.
Defining engagement length connects the profile to the installation and inspection requirements.
It also helps distinguish the functional region from assembly clearance or end relief.
Forming versus machining for profile length and section
Compare forming and machining against profile length and section thickness.
Any precision fit, lead or contact requirement must be separated from the basic blank specification.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Splined drive material, density and treatment requirements
Material and final condition must be reviewed against the defined load, wear, lubrication and environment.
Where powder processing is proposed, agree any relevant density and treatment requirements.
A material family or hardness value alone does not specify the gear or bearing duty.
Review material-selection information →Profile engagement, axis relationship and end-seating checks
Check profile engagement, axis relationships, end seating and the customer's operating requirements.
Use the mating connection to validate the required fit.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Where an agricultural part stops needing precision
Agricultural and outdoor power equipment is the one segment where a buyer regularly pays for precision the machine will never use. The changes below are mostly about giving tolerance back, and they usually cut cost more than any negotiation.
| What we flag | Why it bites on this part | How the drawing usually changes |
|---|---|---|
| Projected area against press capacity | A large flat part needs tonnage proportional to its projected area, and the tonnage decides which press runs it and therefore which price band it sits in. | A part that is close to a press boundary is sometimes cheaper in two pieces, or with a relief that reduces the projected area without weakening it. |
| Gear accuracy class | AGMA 8 on a gearbox that turns at 300 rpm is accuracy nobody can hear. The class is often copied from an automotive drawing. | The accuracy class is set from the actual speed and load, and the saving goes into tooth root strength where the failures actually happen. |
| Density against duty | Because density drives both strength and price, a part that only sees static load is being over-specified at 7.2 g/cm³. | The density is set from the load case, and the drawing states it rather than leaving the supplier to pick the cheaper end of a range. |
| Seasonality and stock | Agricultural demand is seasonal, and a tool sized for peak rate sits idle for half the year while its amortisation is carried on every part. | Annual volume and the shipment pattern are quoted separately, which often changes the cavity count rather than the design. |
| Corrosion protection | A machine that lives outdoors needs protection, but not the same protection as a marine part, and the two are priced very differently. | The exposure is described, and the finish is chosen from it rather than defaulting to the highest spec in the buyer s catalogue. |
Note. These are the changes we most often ask for on this class of part, not a review of any particular drawing. They describe how the process behaves; dimensions, tolerances and acceptance values come from the project drawing.
The useful conversation on these parts is almost always about giving tolerance away, not tightening it. We will tell a buyer which callouts cost money and which do not, and on this kind of part that list is usually long enough to move the price without touching the design intent.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Is a spline simply a gear with more face width?
No. Define the actual mating profile, engagement and fit; a visual resemblance does not establish a gear or spline specification.
Why include spline engagement length?
The mating relationship extends along the profile rather than existing at a single cross-section. Defining engagement length connects the profile to the installation and inspection requirements. It also helps distinguish the functional region from assembly clearance or end relief.
Which checks should be included in gear or support approval?
Check profile engagement, axis relationships, end seating and the customer's operating requirements. Use the mating connection to validate the required fit.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →