
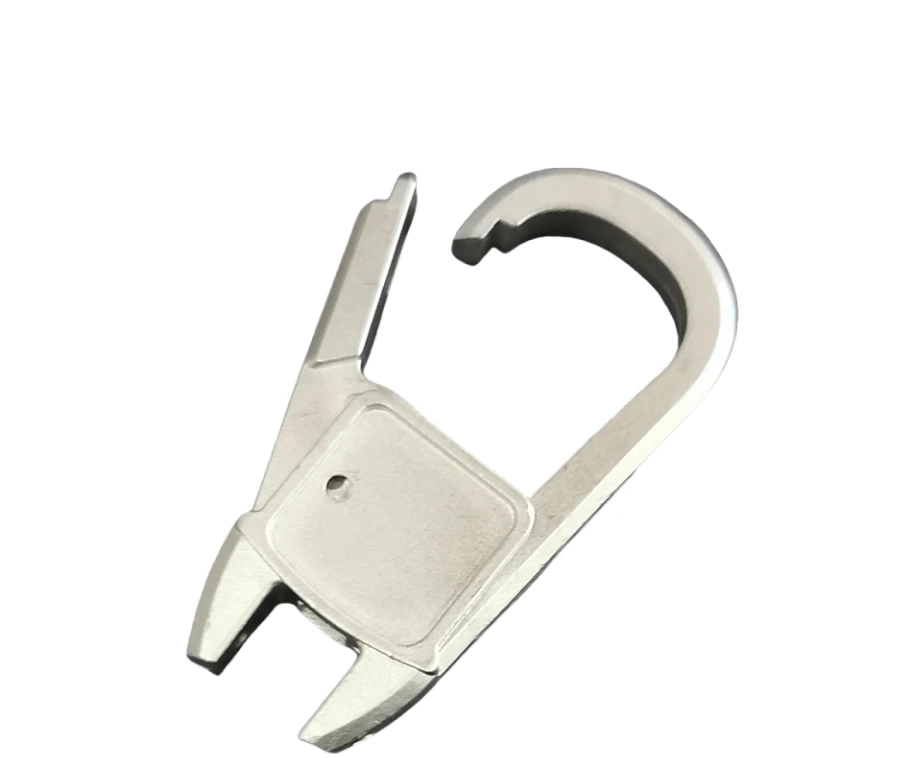
What decorative fastening hardware combines in one component
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
The reference illustrates a clasp-like form whose working surfaces must be separated from cosmetic areas.
Mating member, closure action and visible-face interfaces
Define the mating member, closure or retaining action and visible faces.
Finishing must not obscure engagement edges or alter a working clearance.
Why protect engagement edges during cosmetic finishing?
An edge that participates in closure or retention has a mechanical role even if it is visible.
A general polishing instruction can leave that role unclear.
Identifying protected working features allows appearance finishing and functional inspection to be planned together.
Integrated forming versus machining for clasp bodies
Compare integrated forming with machining for the clasp body and any moving member.
Joining, polishing and final assembly should be included in the quotation scope.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Decorative hardware: where a sintered part loses
On a visible part, the process that wins is usually the one that needs the least finishing, not the one with the lowest forming cost. The comparison below is therefore about what each route leaves behind on the surface, and what has to be removed afterwards.
| Alternative process | When it wins on this part | What puts sintering back in front |
|---|---|---|
| Stamping plus polishing | Wins on the flat clasp where thickness is uniform. Blank, form, tumble, polish: the total is well below any route that starts from powder. | A stamped clasp cannot carry an interlocking tooth form or a sprung arm in the same piece. Once the closure geometry has to work in three dimensions, the assembly that stamping needs costs more than the tool it avoided. |
| Zinc die casting plus plating | Wins on the larger decorative shell. Plating over zinc is the established route for this class of hardware and the tool amortises over a long life. | Plating adhesion at edges and the risk of blistering over porosity are the recurring complaints. Where the part is small and the edges are the working surfaces, a wrought or sintered substrate plates more predictably than a cast one. |
| CNC plus brushing | Wins on the low-volume flagship variant, where surface consistency matters more than piece price and the buyer will pay for a single-setup origin. | Cost per piece stays flat as volume rises, so it never becomes the volume answer. It stays the right answer for the first hundred and the wrong one for the hundred thousandth. |
| Investment casting | Wins on the sculpted, non-geometric body that no die would fill and no press would form. | As-cast surface needs extensive hand finishing, and hand finishing on a visible face is where consistency is lost. That labour is rarely in the initial comparison. |
| Sintering | Wins where an engagement tooth, a spring arm and a locating boss have to exist on one small body, and the saving shows up as fewer assembly steps rather than a lower piece price. | It does not win on a flat plate with a decorative outline. There, stamping is cheaper at every volume that matters. |
Note. This table is a screening aid, not a recommendation against our own process. Where a row above describes your part better than the sintering route does, we will say so and quote against the route that actually fits; the quantities, alloy and tolerances on your drawing still decide the answer.
The argument on a visible part is almost never about the process. It is about what counts as a scratch. That has to be written as a viewing distance, a light condition and an allowed count, and it decides who can supply the part far more than the route does.
Fastening hardware material, engagement-edge and finish requirements
Define base material, final condition and cosmetic finish separately.
Identify visible faces, permitted edge rounding and the dimensions that must be met after finishing.
Any magnetic, electrical or acoustic requirement needs its own specification.
Review material-selection information →Closure, retention and finish-consistency checks
Inspect closure, retention, accessible edges and finish consistency.
Agree an appearance sample separately from the functional test.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Can polishing change the fastening action?
It can affect edges or mating dimensions if uncontrolled; specify which functional surfaces must be preserved.
Why protect engagement edges during cosmetic finishing?
An edge that participates in closure or retention has a mechanical role even if it is visible. A general polishing instruction can leave that role unclear. Identifying protected working features allows appearance finishing and functional inspection to be planned together.
How are appearance and functional fit checked?
Inspect closure, retention, accessible edges and finish consistency. Agree an appearance sample separately from the functional test.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →