
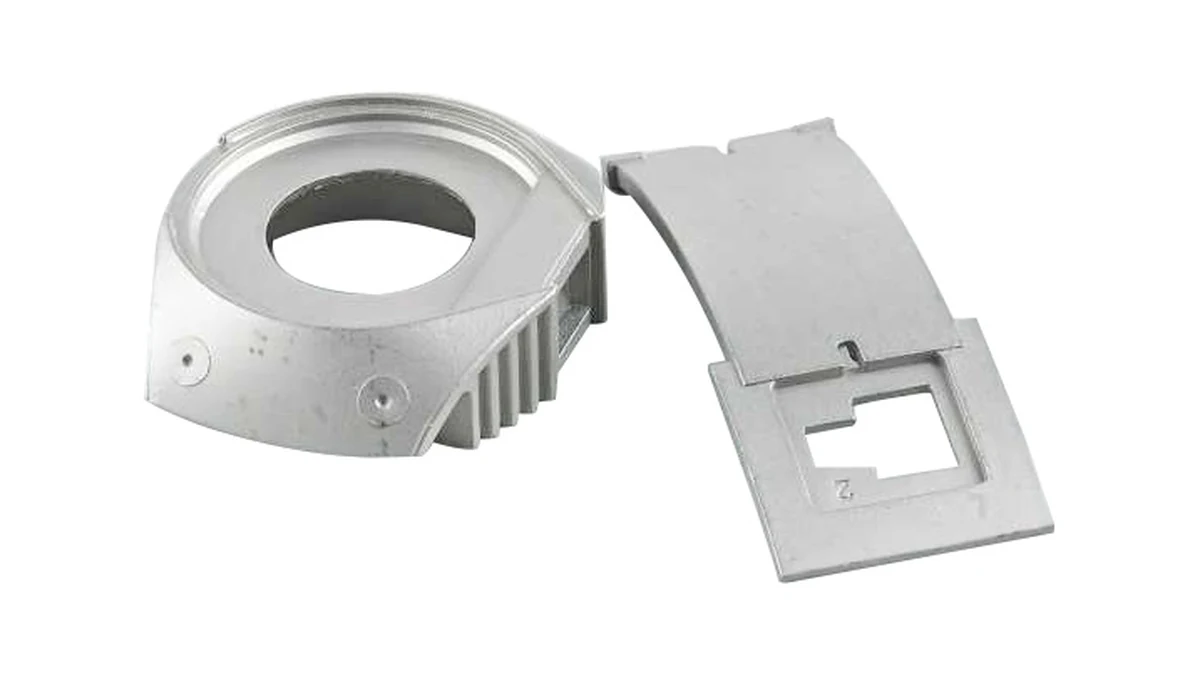
What watch cases and attachment hardware combine in an assembly
The reference includes case-like and rectangular forms, each needing a defined supply scope.
Case-back, movement, strap and assembly-datum interfaces
Mark interfaces to the case back, movement, strap or other mating components.
Visible surfaces, openings and assembly datums should be specified independently.
Why distinguish the exterior case from its closing interfaces?
The exterior establishes appearance, while seats, threads or other joints establish how the watch closes and retains its components.
These requirements should not be collapsed into one surface-finish description.
The mating parts define the functional meaning of each interface.
Forming versus machining for case profiles and attachments
Compare forming and machining for the case profile and integrated attachment features.
Threads, seating faces and openings may require finishing after the basic body is made.
Compare manufacturing capabilities →Watch case base material and cosmetic-finish requirements
Define base material, final condition and cosmetic finish separately.
Identify visible faces, permitted edge rounding and the dimensions that must be met after finishing.
Any magnetic, electrical or acoustic requirement needs its own specification.
Review material-selection information →Assembly fit, exterior finish and sealing-interface checks
Check assembly fit, exterior finish and any customer-defined sealing interface.
Water resistance cannot be inferred from a component photograph or material name.
Quality documentation →Which case features move between production lots
A watch case carries two unrelated requirements in the same part: a visible finish, and a closing joint that has to sit flush or seal. They drift for different reasons, and one cosmetic standard cannot cover both.
| What drifts between lots | Where the drift comes from | What the release check catches |
|---|---|---|
| Case-back joint, seating face and thread | The seat is machined after sintering, so its position depends on the sintered blank. A blank that comes in slightly oversize leaves less material for the finishing cut, and the seat moves with the blank. | Check seat depth and thread engagement on a finished part, and check blank size as a separate in-process item. A thread that gauges at the supplier can still fail after plating. |
| Lug hole position and spacing | Lug holes are usually drilled or reamed in a fixture located from the case centre. Fixture wear moves the pair together, which keeps the spacing correct while the position drifts. | Check the hole pair against the case centre and against the case-back seat. Spacing on its own will not show a shift of the whole pair. |
| Flatness of the case-back seating face | Thin case sections distort in sintering, and machining one face can relieve or add to that distortion. The result depends on how the part was supported during the cut. | Check flatness in the free state, and check sealing on an assembled sample. A flatness reading taken on a clamped part says nothing about whether the joint closes. |
| Visible surface, polish and brush direction | Polishing removes material, and the amount depends on the starting surface. Two lots that start from slightly different sintered surfaces need different polishing time to reach the same appearance. | Keep a retained boundary sample for each visible area, and re-qualify it when the sintered surface or the polishing process changes. Appearance is a process output, not a dimension. |
| Coating colour and thickness | PVD and electroplated finishes change colour with thickness and with surface preparation. Colour matching between lots is a process control question, not a drawing tolerance. | State colour by an agreed sample and thickness by range, and check both on the same part. Where colour is critical, ask for a coupon from the same load. |
Agree on the sample size and inspection method before production.
The closing joint is a drawing problem, because depth, position and flatness can all be stated against the case centre. The appearance is not: a polish specification only holds if a boundary sample is retained and refreshed. A drawing that treats both as one surface requirement leaves the visible side over-specified and the joint under-specified.
How the sintered blank and its finishing steps are sequenced →
What to include in your enquiry
- Drawing and mating dimensions.Mark interfaces to the case back, movement, strap or other mating components. Include the drawing revision.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
- First-sample inspection.Check assembly fit, exterior finish and any customer-defined sealing interface. Specify the mating part or inspection fixture.
Common questions
Does a metal watch case automatically provide water resistance?
No. Seals, closure, openings and assembly validation determine the finished watch requirement.
Why distinguish the exterior case from its closing interfaces?
The exterior establishes appearance, while seats, threads or other joints establish how the watch closes and retains its components. These requirements should not be collapsed into one surface-finish description. The mating parts define the functional meaning of each interface.
How are appearance and functional fit checked?
Check assembly fit, exterior finish and any customer-defined sealing interface. Water resistance cannot be inferred from a component photograph or material name.