
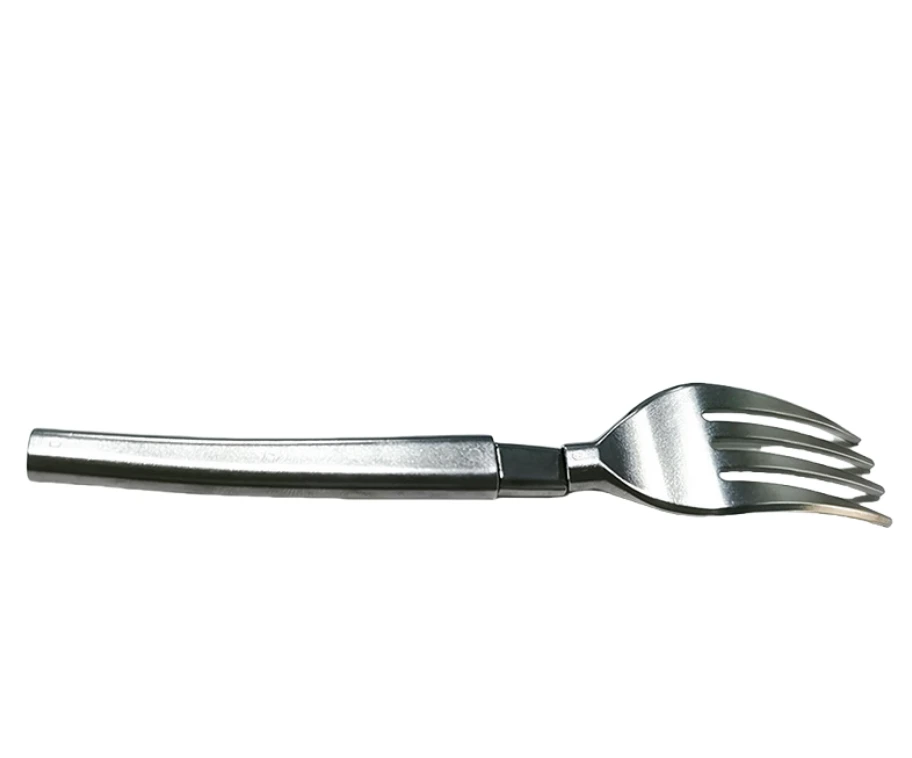
What kitchenware metal handles and fittings do in a utensil
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
The assembled reference helps locate the handle and the connection to the working end.
Handle body, utensil head and joining-feature interfaces
Distinguish the handle body from the utensil head and joining feature.
Grip edges, attachment geometry and accessible cleaning surfaces require separate acceptance criteria.
Why define the joint as well as the utensil outline?
A handle can have an acceptable grip contour yet connect incorrectly to its working end.
The joint carries the functional relationship between the pieces.
Reviewing the attachment and body separately makes it easier to specify the part boundary, finishing sequence and final assembly check.
Choosing MIM or machining for kitchenware fittings
Compare MIM for integrated small fittings with machining or other processes for simple or elongated shapes.
Joining and polishing need to be included in the component supply definition.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Grade, cleaning and food-contact requirements for kitchenware parts
Specify the required grade or performance criteria together with cleaning, wear and appearance requirements.
For any surface that contacts food or beverage, identify the applicable customer documentation and acceptance criteria.
A stainless label is not a complete contact specification.
Review material-selection information →Attachment fit, handling-surface and appearance checks
Check attachment fit, burr-free handling surfaces, appearance and any project-defined cleaning or contact requirements.
Do not infer a complete utensil qualification from a component material name.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →What food contact changes in a MIM kitchenware drawing
A kitchen part is a metal part with an extra set of requirements layered on top: what it releases, what it traps, and how it is cleaned. Those requirements do not appear on a mechanical drawing, and that is exactly why they cause trouble.
| What we flag | Why it bites on this part | How the drawing usually changes |
|---|---|---|
| Open porosity at the food surface | A sintered surface at 7.6 g/cm³ and above is nearly closed, but the surface still holds microscopic pits that trap food residue and are hard to clean. | Food-contact faces are either brought to a higher density, polished, or given a glass-bead finish that closes the surface rather than opening it. |
| The material declaration | Food contact is regulated by the alloy and by what it releases, not by whether it is stainless. Two grades that both pass a salt spray test can differ on release. | The grade is named with its standard and the food-contact compliance is quoted as a document in the RFQ, not assumed from the alloy name. |
| Cleaning agent resistance | Dishwasher detergents are alkaline and chlorinated, and both attack a passivated surface over repeated cycles. | The cleaning environment is written on the drawing, and the passivation class is chosen for it rather than for ambient humidity. |
| Radii instead of corners | Food-safe design is about cleanability, and an internal corner that cannot be reached with a cloth is a design defect regardless of the metal. | Internal radii are enlarged and sharp inside corners are removed, which also improves the fill in the tool. |
| Wall sections for heat | A handle or a bowl wall that is too thin transmits heat to the hand, and the thickness that fixes it is a design decision made before the tool. | Wall thickness is set from the thermal requirement and stated as a minimum, not left as a nominal that the tool can shave. |
Note. These are the changes we most often ask for on this class of part, not a review of any particular drawing. They describe how the process behaves; dimensions, tolerances and acceptance values come from the project drawing.
We do not certify food contact for a customer s market, and we say so early. What we do is supply the material certificates and the process records that let them certify it, and that is a different deliverable that should be quoted from the start.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Can the handle and working end be supplied as one part?
That depends on the drawing, overall geometry and joining requirements; mark the desired part boundaries before the process review.
Why define the joint as well as the utensil outline?
A handle can have an acceptable grip contour yet connect incorrectly to its working end. The joint carries the functional relationship between the pieces. Reviewing the attachment and body separately makes it easier to specify the part boundary, finishing sequence and final assembly check.
How should fit and operating behavior be approved?
Check attachment fit, burr-free handling surfaces, appearance and any project-defined cleaning or contact requirements. Do not infer a complete utensil qualification from a component material name.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →