High-speed gear stage
Small motor-end gears run faster and are sensitive to tooth accuracy, material consistency, noise and wear.
Cordless pruning shears package a motor, reduction system, blade-drive mechanism, battery and safety controls into a compact high-cycle tool. For SINTS, the strongest manufacturing questions are usually around gears, sector gears, links, bushings, pivots, locks and brackets — not the blade itself.
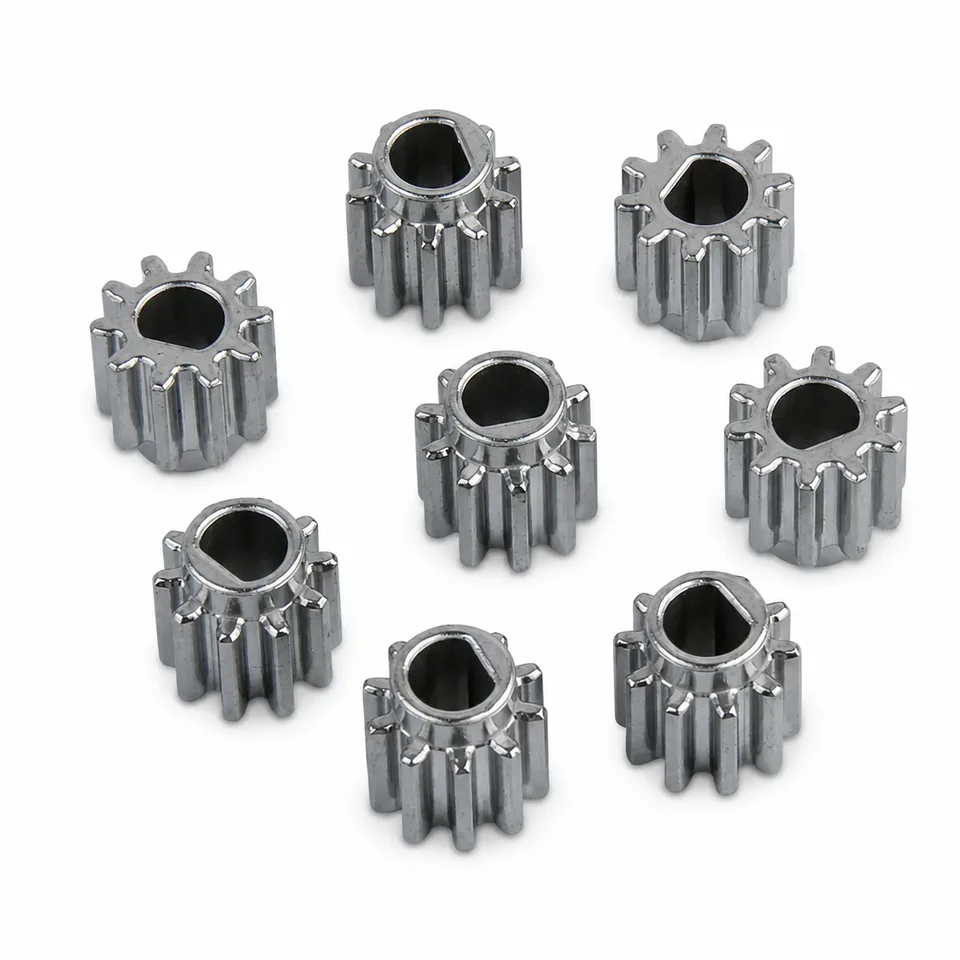
Manufacturing reference: Representative SINTS components are shown to illustrate gear, bushing and compact mechanism geometries relevant to electric pruning-shear engineering reviews. Final suitability depends on the actual drawing, load, wear, heat treatment and production requirements.
The SINTS technical handbook describes a typical chain as trigger and controller → motor → reduction gears → pinion, sector gear or linkage → moving blade around its pivot. The manufacturing route changes as speed falls and torque rises toward the cutting head.
Small motor-end gears run faster and are sensitive to tooth accuracy, material consistency, noise and wear.
Sector gears, rockers and links closer to the blade see higher torque, impact and fatigue demands; root strength and heat treatment become more important.
Pins, bushings and bearing surfaces control blade play and mechanism stiffness. Simple rotational geometry often still favors turning, grinding or PM bushings.
Feature-rich latches, stops, brackets and compact structural pieces may justify MIM when volume and geometry make multi-operation machining inefficient.
The first question is not “Can MIM make it?” but which route best matches load, geometry, tolerance, heat treatment and annual volume.
| Component | Function | First route to evaluate | Why / watchout |
|---|---|---|---|
| Spur / planetary gear | Motor-to-blade reduction | PM / gear process | Repeat-volume gears are strong PM candidates; tooth load, density, noise, accuracy and heat treatment define whether PM, MIM or another gear route wins. |
| Compound / feature-rich small gear | Compact multi-stage transmission | MIM / PM / gear process | Extra 3D features may improve the case for MIM, while press-friendly geometry may favor PM. Critical teeth or bores may still need finishing. |
| Sector gear / rocker | Converts gearbox rotation into blade motion | MIM / PM / CNC | Compact geometry can suit near-net-shape routes, but tooth-root impact, bearing surfaces and heat-treatment distortion must be reviewed. |
| Link / eccentric / lock part | Transfers motion or controls mechanism | MIM — worth evaluating | Small 3D parts with bosses, holes, pockets and multiple machining setups are common MIM candidates when volume is stable. |
| Pivot pin / shaft | Supports blade or transmission rotation | CNC / turning / grinding | Simple rotational geometry, runout, bearing fits and hardened surfaces often favor machining rather than MIM. |
| Bushing / sleeve | Supports pivot or gear rotation | PM — often strong | PM is a natural first route for many repeat-volume bushings; load, lubrication, density and wear determine the final specification. |
| Compact bracket / retainer | Locates mechanism or spring / sensor hardware | Stamping / MIM / CNC | Thin simple brackets favor stamping. MIM becomes more interesting when thickness, bosses, hooks or 3D features make stamping cumbersome. |
| Cutting blade | Shears branch material | Forging / stamping / machining + heat treatment | Usually not a MIM priority. |
SINTS component examples illustrate manufacturing geometry and process options. Final application suitability is assessed from your drawing and operating requirements.
Useful for discussing tooth form, bore features, heat treatment, density and repeat-volume transmission economics.
SINTS manufacturing reference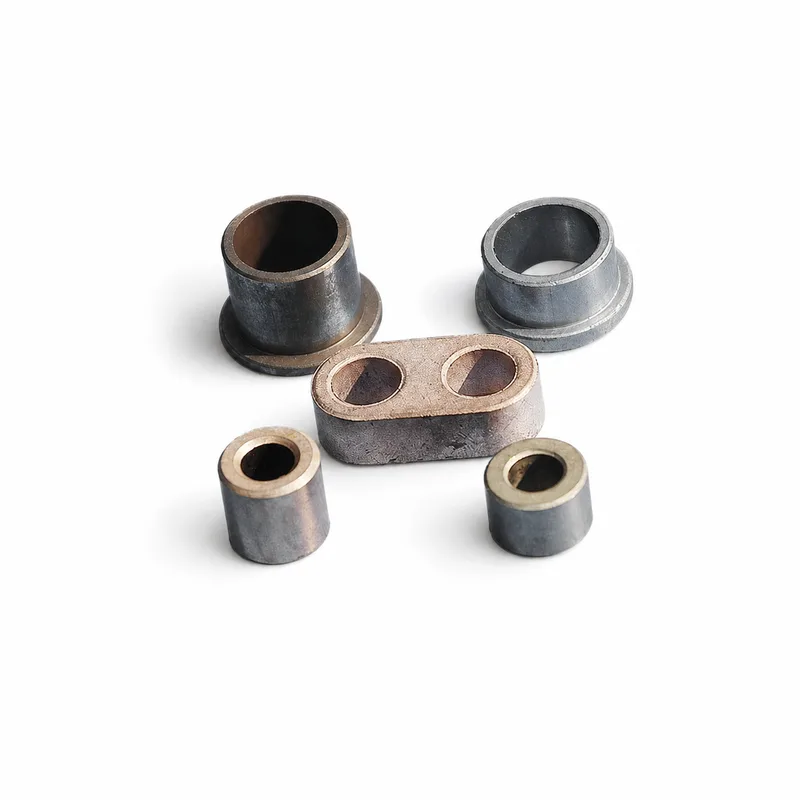
Relevant to pivot and support functions where load, lubrication, clearance, density and wear make PM worth evaluating.
SINTS manufacturing reference
Useful for discussing feature-rich near-net-shape geometry where teeth or drive features are integrated into a compact part.
SINTS manufacturing referenceUse this application guide for torque, wear, backlash, pivot and safety context. Use Product family pages for the component-level manufacturing decision.
Spur, compound, sector and other drive components where tooth load, wear, backlash and finishing decide the route.
Product family →Pivot and bearing interfaces where compaction direction, density, sizing, lubrication and wear matter.
Product family →Links, rockers, locks, carriers and feature-rich parts close to the blade-drive mechanism.
Product family →Pivot pins and rotating interfaces where turning, grinding and bearing-fit control may remain strongest.
Product family →Blade and wear-zone discussions where edge geometry, hardness, toughness and heat treatment dominate.
Product family →Repeat-volume gears, bushings and press-compatible transmission parts where material utilization and near-net-shape production matter.
Small complex links, lock parts, rockers, feature-rich gears or carriers with 3D geometry that would otherwise need several CNC setups.
Pins, shafts, prototypes, low-volume parts and components dominated by bearing fits, runout, flatness or hard precision datums.
Include gear data, datums, pivots, bearing fits and any surfaces already identified for machining.
State the current material, heat-treatment condition and wear or corrosion requirement.
Stable platform volume is what makes MIM or PM tooling economics meaningful.
Share nominal torque, peak or stall conditions, cutting diameter class and cycle-life target where available.
Identify gear backlash, pivot play, blade-side clearance and any dimensions tied directly to cut quality.
Cost, gear wear, noise, size, machining time, heat-treatment distortion or supply stability may lead to different process choices.
Electric pruning shears combine a geared transmission, a cutting blade and a trigger or sensor input in a handheld, battery-powered tool. These answers cover the gear, linkage and blade questions that decide process route and durability.
Repeat-volume gears, bushings and some press-compatible transmission parts are natural first candidates. Tooth load, density, noise, hardness and required accuracy still have to be reviewed.
MIM is most relevant to small feature-rich links, locks, rockers, carriers and complex compact mechanism parts. It is not automatically the right choice for simple shafts or blades.
Usually not the first target. Cutting blades depend heavily on blade-steel selection, edge geometry, heat treatment, toughness and sharpening, so conventional blade-manufacturing routes are normally evaluated first.
Share material, hardness, annual volume, gear data, normal and stall torque, cycle-life target, critical clearances, lubrication and any post-machining requirements.
It covers the metal parts between the trigger and the blade — the motor pinion, reduction gears, planetary carriers, cams, linkages, pivots, bushings and blade-retention hardware. Those parts transfer motor torque into a cutting stroke while surviving shock loads, dust, sap and repeated partial cycles, which is why gear and linkage components dominate the family rather than the blade itself.
Powder metallurgy is usually the first route to evaluate for repeat-volume spur, helical or planetary gears, because near-net shaping produces the tooth form in one operation and sinter-hardening or heat treatment can follow. MIM becomes more relevant when the gear carries integrated cams, hubs or non-rotational features that would otherwise need a second operation. Machining remains the reference for very low volume or where the tooth accuracy requirement exceeds what a sintered gear can hold.
They change the failure mode the review is about. A shear that stalls mid-cut or is forced through a branch puts a peak load through the gear train, the pivot and the linkage, and that peak — not the nominal cutting torque — usually decides dimensions, tooth root stress and heat treatment. Sharing stall conditions, jam behaviour and whether the tool reverses means the review covers impact and fatigue rather than average duty.
Send the drawing, the load case including stall and jam, the duty cycle and how many cycles the tool is expected to survive, the material or hardness of the mating blade, the outdoor and sap exposure, the noise and backlash targets and the annual volume. For a gear or linkage, tooth loading and functional backlash matter more at screening stage than a generic dimensional tolerance.
We can review gear/bushing suitability, MIM opportunities, machining-critical features, material and likely secondary operations — including cases where CNC or a conventional blade process remains the better route.