
Cost planning for a small metal part starts before the tool is designed. The drawing, annual quantity, material, critical features and inspection plan together determine whether MIM, powder metallurgy, CNC or a hybrid route will be economical and reliable over the life of the program.
This guide walks through the levers that actually move program cost — tooling amortization, geometry, volume, tolerances, secondary operations and RFQ quality — with the questions SINTS engineering asks when a customer wants a lower landed cost per part.
1. Separate tooling cost from unit cost
Tooling is an upfront investment; unit cost repeats with every part. Comparing a quoted piece price without the tooling and secondary-operation picture is how programs end up with a low part cost and a high total cost. The right comparison is total program cost over the expected production horizon:
A useful habit is to write the expected program quantity and its confidence level on the RFQ. A forecast that is materially higher or lower than actual demand can change the recommended route entirely, and the supplier cannot make that judgment call without a realistic range.
2. Simplify geometry without losing function
Geometry is where the biggest cost difference between a well-designed part and a difficult one is created. MIM and PM both form geometry in a cavity, so features that complicate the cavity, the ejection or the compaction repeat their cost in the tool and in every part.
The goal is not to weaken the part, but to remove complexity that does not earn its cost. The table below shows the features SINTS reviews first when a drawing is cost-sensitive:
The same discipline applies to cosmetic requirements. Separating faces that are critical-to-function from faces that are purely cosmetic lets the supplier run the cosmetic areas as-molded and concentrate machining where it matters, which keeps both tool and unit cost under control.
3. Let volume guide the process
Higher repeat volume generally makes tooling-based processes more attractive, but volume alone does not make a part suitable for MIM or PM. The route should fit both the quantity and the geometry:
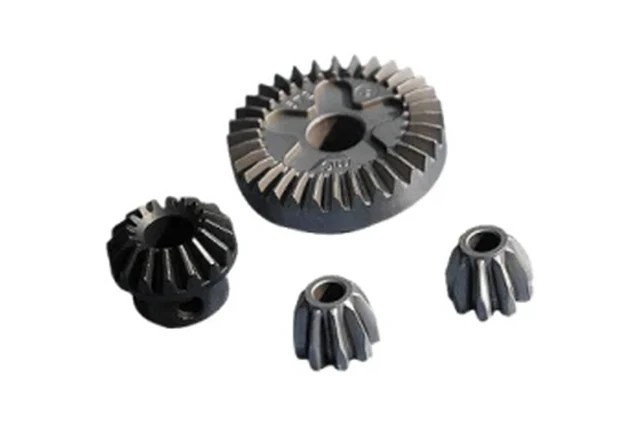
The key question is not “which process is cheapest?” but “which process holds this geometry at this volume with the required quality?” A part that is well suited to the process will always quote better than a part that is forced into one.
4. Control tolerance and inspection scope
Every unnecessary tight tolerance can add process, tooling or measurement cost. Use practical general tolerances and reserve tighter controls for features that truly govern fit, function, sealing, wear or assembly.
- Identify the dimensions that control fit and function: mating bores, press-fit diameters, gear teeth, sealing faces. These get the tight tolerance and the inspection attention.
- Use practical general tolerances elsewhere: cosmetic and non-mating dimensions should not inherit a tighter requirement than the assembly actually needs.
- State the measurement method and sample plan: CMM, gauge, first-article report, dimensional sampling frequency. The supplier can then price the real requirement instead of an avoidable worst case.
- Understand what the process holds: MIM and PM dimensional capability is well documented — a reference such as the MIM tolerances guide shows what is achievable as-molded versus what needs secondary machining.
Tolerance decisions interact with process selection. A feature that needs control beyond practical as-formed capability may require sizing, machining, grinding or another secondary step. Calling it out at RFQ stage lets the route comparison include that operation before sampling.
5. Choose the material for the property, then optimize it
Material cost is a large share of unit cost in MIM and PM, and it is driven by the grade rather than by the process. The cheapest way to reduce material cost is to select the grade that meets the requirement — no more, no less.
- Corrosion, media contact and food-contact requirements should be treated as separate material and compliance questions. Stainless grades may be evaluated, but exact grade, surface condition and regulatory requirements must be confirmed for the project.
- Hardness and wear can be met by a low-alloy grade with heat treatment, often at lower material cost than a stainless option.
- Magnetic properties are material-driven: soft-magnetic alloys or controlled stainless grades behave differently, and the grade must be selected for the requirement.
- Weight reduction through wall thinning only helps when the geometry can be lightened without losing strength — and it usually also shortens cycle time, which lowers unit cost twice.
The grade decision belongs on the drawing with the property target, so the supplier quotes the grade the application needs rather than a conservative default. When in doubt, a short functional note on the RFQ — “gear, wear application, no corrosion exposure” — lets engineering propose the most cost-effective grade for review.
6. Audit secondary operations
Secondary operations can become a major recurring cost in MIM/PM programs. A small number of tapped holes, sealing bores, ground faces or deburring steps can materially change unit cost when they were not planned into the process route.
The audit question for every feature is simple: does this feature have to exist, and does it have to be machined? Features that can be molded — threads with fine pitch limits, undercuts with draft, cosmetic faces without tight roughness — remove a per-part cost that repeats for the life of the program.
7. Design for tooling efficiency
Tooling cost tracks the number of actions, the steel complexity and the expected life — not the size of the part alone. A few design choices made early have an outsized effect on the tool quote:
- Minimize cavity actions: every slide, lifter or core pull adds moving steel and wear points. Ask whether the undercut can be redesigned, molded with a standard action, or left for a simple secondary operation.
- Plan the parting line: a flat parting line keeps the tool simple; a complex three-dimensional parting line increases build and maintenance cost. The parting line should fall where flash is acceptable and function is unaffected.
- Design for ejection: draft and surface finish on ejection surfaces reduce reject risk. A part that sticks in the cavity costs tooling time and rejects across the whole program.
- Match tool life to the program: tooling material, wear strategy and maintenance planning should follow expected volume, geometry, material and program life rather than one generic quantity threshold.
Tooling efficiency is a dialogue, not a one-way instruction. When SINTS reviews a drawing before quoting, the engineering feedback often includes a small geometry change that removes a tool action or a tolerance that removes an inspection step — changes that cost nothing on the drawing and save money in every part.
8. Prepare a cost-ready RFQ
A cost review is only as good as the information behind it. The checklist below is what SINTS engineering looks for when comparing MIM, PM, CNC and hybrid routes:
- Drawing or CAD file with material grade and condition.
- Annual volume and forecast horizon — the basis for tooling amortization and route selection.
- Critical dimensions identified, with the measurement method and sample plan.
- Finish, hardness and coating requirements on the faces that need them.
- Inspection documents required (FAI, dimensional report, material certificate).
- Target timing and packaging needs so the process and logistics plan can be priced.
With these details, SINTS can compare the routes, explain the main cost drivers and propose a tooling and process plan before any tooling investment is approved. The goal is a quotation that reflects the real requirement — not a worst-case risk allowance.
9. When SINTS helps you decide
The lowest-cost route for a small metal part is rarely obvious from the drawing alone. It depends on the interaction between geometry, volume, material, tolerances and secondary operations — which is exactly the review SINTS performs before quoting.
For OEM programs, the most efficient step is to send the drawing with a short note on annual volume and how the part is used. SINTS engineering reviews the part against MIM, PM, CNC and hybrid options, identifies the cost drivers, and proposes the most economical combination of process, grade and secondary operations before tooling is approved. Programs already locked to a process still benefit from the review: the focus shifts to geometry, tolerances and inspection scope, where most cost reduction is actually found.
Have a drawing and an annual volume?
Send both to our engineering team for a route and cost review. SINTS compares MIM, PM, CNC and hybrid options, explains the main cost drivers, and proposes the most economical plan before tooling approval.
Send Drawing for Review