Why a titanium request needs an alloy-specific review
Review this component together with its mating parts and delivered condition. The interfaces below define the drawing information needed to assess forming, finishing and inspection.
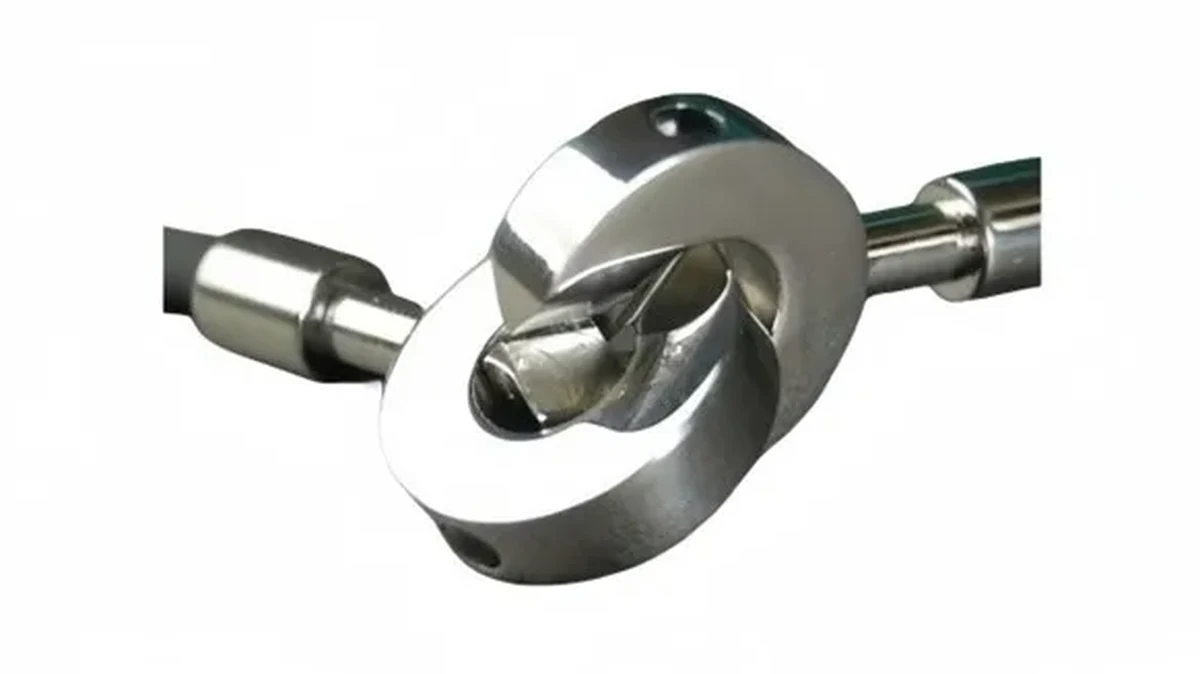
The catalog reference provides an example form; it is not proof of a particular alloy or an approved process for a new drawing.
Functional surfaces and titanium-specification interfaces
Define functional surfaces and the required titanium specification before comparing routes.
Identify any section transitions, holes or interfaces that control the part in service.
Why is a material-specific process review necessary?
The selected alloy and required condition determine what must be controlled and documented.
A familiar shape does not make a processing plan transferable from another metal.
The project needs an explicit relationship between material specification, manufacturing steps and acceptance evidence.
Comparing machining and powder routes after alloy review
Compare machining with powder-based routes only after reviewing alloy availability, process compatibility and validation needs.
Do not apply a steel MIM process assumption to titanium.
The proposed route is confirmed for your drawing, material and quantity. An image does not establish a fixed tolerance or a complete process specification.
Compare manufacturing capabilities →Titanium alloy, property and documentation requirements
Specify the titanium alloy or the required material properties and documentation.
Confirm how final chemistry, condition and critical surfaces will be established for the proposed route.
Material appearance and a legacy catalog label cannot verify either an alloy grade or suitability for a particular application.
Review material-selection information →Material records, final condition and critical-geometry checks
Specify material records, final condition, critical geometry and any application-specific verification.
The approval plan should identify the evidence required for the selected route.
Specify the drawing revision and the condition in which each dimension is inspected. Record the agreed dimensional and functional checks before sample approval.
Quality documentation →How titanium parts fail, and why the certificate does not settle it
Titanium is the one material in this group where the process atmosphere matters as much as the alloy. The failures below are not geometry problems and they are not visible on a dimensional report, which is why they tend to arrive as a surprise after a successful first article.
| What goes wrong in service | What drives it | Where the drawing closes it out |
|---|---|---|
| The part is brittle and cracks on the first serious load | Titanium picks up oxygen, nitrogen and carbon at elevated temperature, and the pickup happens during binder removal and sintering. A part can be the right alloy and still be interstitial-rich, and interstitials harden and embrittle it without changing the alloy name. | An interstitial specification alongside the alloy, with the analysis method named, and the maximum processing temperature band; verified by chemical analysis on the finished part rather than on the powder, plus a ductility check. |
| Fatigue life falls well short of the wrought reference | Residual porosity behaves as a crack starter, and in titanium the margin between "dense enough to machine" and "dense enough to cycle" is wider than in steel. | A density requirement tied to the actual load case, and whether hot isostatic pressing is part of the route; verified by a fatigue test on the intended section rather than by an archimedes density number alone. |
| Parts warp during sintering | Thin sections sinter at a different rate than thick ones, and the transformation behaviour of titanium gives little forgiveness. Support in the furnace and the geometry of the setter decide whether the part comes out flat. | Which surfaces must remain flat after sintering and what stock is available for correction; verified on parts from a full furnace load, since a single-part trial hides the thermal gradient. |
| Machining cost removes the benefit of the near-net shape | Titanium galls, work-hardens and conducts heat poorly, so every surface left for machining costs far more than the same surface in stainless. A design that leaves generous stock "for safety" is the most common way to lose the business case. | A statement of which surfaces are as-sintered and which are machined, with the stock allowance per surface; verified by a costing comparison at quotation, before the tool is cut. |
| The surface does not match the certified chemistry | A contaminated layer at the surface can differ from the bulk, so a certificate that describes the interior can be true and the surface still not be fit for a medical or implant-adjacent application. | Whether a surface removal step is required, and how much, plus the cleanliness condition; verified by surface analysis on a treated part rather than by a bulk certificate. |
Note. The table names service failure modes and the drawing features that address them; it sets no acceptance values. Dimensions, tolerances and test criteria come from the project drawing.
Nothing on this list is fixable by tight tolerances, and that is the point of separating it out. Interstitial control, density and surface contamination are furnace and atmosphere decisions; warpage is a fixturing decision; machining stock is a design decision. A titanium RFQ that only states the alloy and the dimensions leaves all five open, and each of them can fail independently while the dimensional report stays clean. If the application cannot tolerate the residual risk on density, the honest answer may be that this part belongs in a wrought route with machining, at a different cost.
Prepare a Product-Specific RFQ
- Component definition. Send the 2D drawing and 3D model, where available, with the drawing revision and the requested part or assembly scope.
- Mating information. Include the assembly references needed to define the interfaces discussed above.
- Delivered condition. State material, finishing and inspection requirements, identifying any items that need a manufacturing recommendation.
- Supply plan. Include sample needs, expected order and annual quantities, packaging requirements and target timing.
Product Questions
Can titanium use the same processing plan as stainless steel?
No. Material and processing compatibility must be assessed specifically for the selected titanium alloy and part.
Why is a material-specific process review necessary?
The selected alloy and required condition determine what must be controlled and documented. A familiar shape does not make a processing plan transferable from another metal. The project needs an explicit relationship between material specification, manufacturing steps and acceptance evidence.
What should the project acceptance plan include?
Specify material records, final condition, critical geometry and any application-specific verification. The approval plan should identify the evidence required for the selected route.
Technical Context
The product-specific notes above identify drawing-review questions. General process and material references are collected separately; they do not verify a material grade, production qualification or performance claim for the pictured part.
Manufacturing and material references →